Complete manufacturing
Cold swaging rifling mandrels are produced completely on one machine; cylindrical grinding and groove grinding are done on the same machine.
Since 198343 years serving Turkish industry
Rifling mandrel grinding
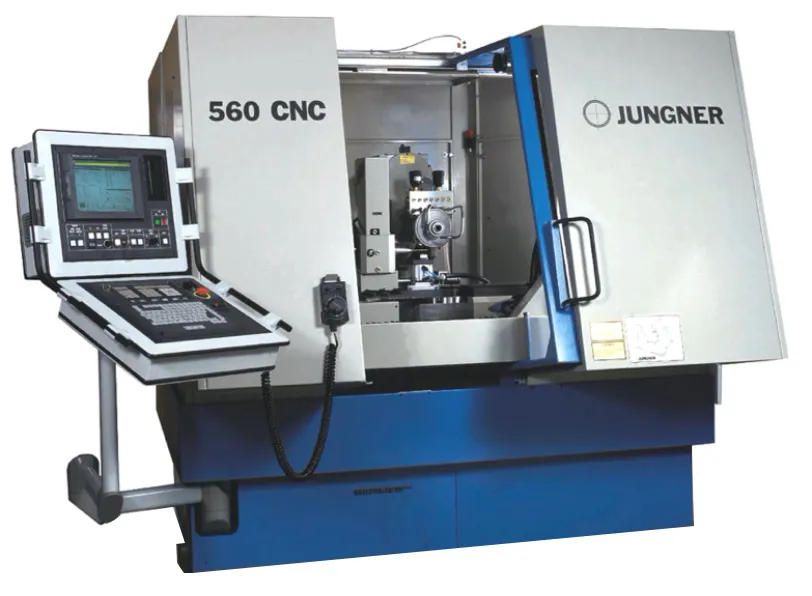
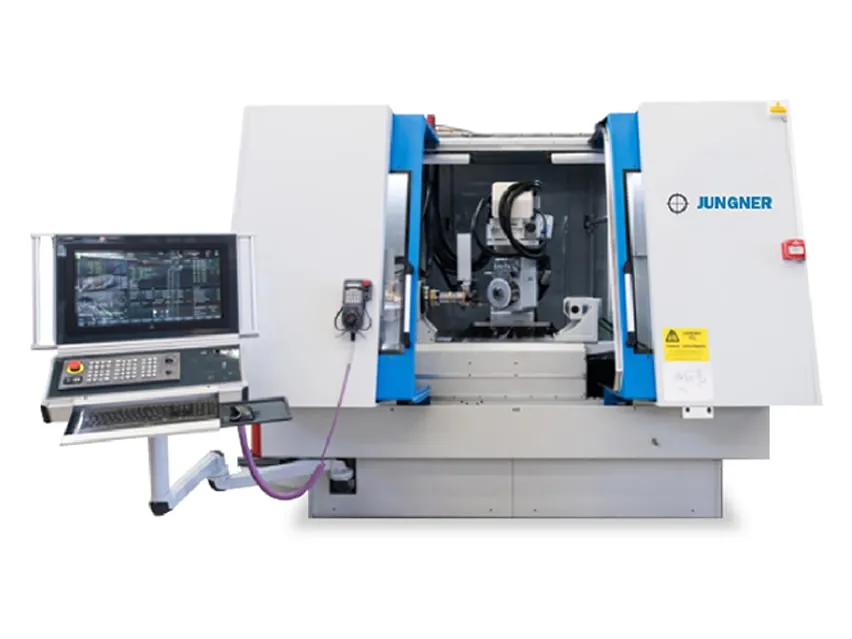
5-axis precision CNC grinding machine for the complete manufacturing of cold swaging rifling mandrels
ⓘ Manufacturer data (JUNGNER product page and technical specification). Values may change and vary; not binding on Boztaş.
Cold swaging rifling mandrels are produced completely on one machine; cylindrical grinding and groove grinding are done on the same machine.
The workhead, direct-driven by a torque motor, turns at up to 600 rpm; a rigid tailstock supports high-precision grinding.
5 axes with 5D interpolation and a 6th software axis; 0.0001 mm resolution, 1.2 µm positioning accuracy on X, Y and Z, Fanuc 0i MB or 30i MB control.
Direct-drive workhead 600 rpm, 85 Nm, ISO-50; tailstock; 11.5 kW spindle, Ø 200 mm wheel
Suited to: Complete manufacturing of cold swaging rifling mandrels
Workhead 166 rpm, 150 Nm; automatic loading and unloading with a Fanuc robot
Suited to: Resharpening and manufacturing of tools, cutters and broaches
| Feature | MG 560 CNC |
|---|---|
| Axes | |
| X axis: stroke / rapid traverse / positioning accuracy | 560 mm (product page: 600 mm) / 15 m/s / 1.2 µm |
| Y axis: stroke / rapid traverse / positioning accuracy | 300 mm / 15 m/s / 1.2 µm |
| Z axis: stroke / rapid traverse / positioning accuracy | 300 mm / 15 m/s / 1.2 µm |
| Linear-axis resolution | 0.0001 mm |
| B axis: stroke / speed / accuracy | Endless (∞) / 600 rpm / ±1.8″ |
| C axis: stroke / speed / accuracy | ±135° / 2,160 °/min / ±1.8″ |
| Rotary-axis resolution | 0.0001° |
| Interpolation | 5 axes with 5D interpolation + 6th software axis |
| Workhead (B axis) | |
| Drive | Torque motor, direct drive |
| Clamping interface | ISO-50 |
| Indexing accuracy | ±1.8″ (specification: ±36″) |
| Cylindrical grinding speed | 600 rpm |
| Max. torque | 85 Nm |
| Tailstock | Rigid tailstock; grinding between dead centres |
| Tool capacity | |
| Max. tool diameter | 300 mm |
| Grinding spindle and wheel | |
| Spindle speed | 0–12,000 rpm |
| Spindle power | up to 11.5 kW |
| Max. grinding wheel diameter | Ø 200 mm |
| Measuring | |
| Measuring probe | Renishaw LP2 / MP250, touch trigger, kinematic design, interference-resistant |
| Unidirectional repeatability | 1–2 µm |
| Control | |
| CNC control | Fanuc 0i MB or 30i MB |
Manufacturer data (JUNGNER product page and technical specification). The X stroke is 560 mm in the specification and 600 mm on the product page; workhead indexing accuracy is ±1.8″ on the product page and ±36″ in the specification. Rapid-traverse values are reproduced in the unit given in the specification (m/sec).
Technical data is taken from information published by the manufacturer. The manufacturer may change it without notice, and values may vary with the model and the machine configuration. The data is for information only and is not binding on Boztaş; binding values are stated only in a written quotation.
The manufacturer defines the MG 560 CNC for the complete manufacturing of cold swaging rifling mandrels; cylindrical and groove grinding are done on the same machine, between dead centres.
The workhead is direct-driven by a torque motor and turns at up to 600 rpm; torque is 85 Nm and the clamping interface ISO-50. A rigid tailstock is provided for high-precision grinding.
The grinding spindle runs at 0–12,000 rpm with up to 11.5 kW and a maximum wheel diameter of Ø 200 mm. The Renishaw LP2 / MP250 probe gives 1–2 µm unidirectional repeatability.
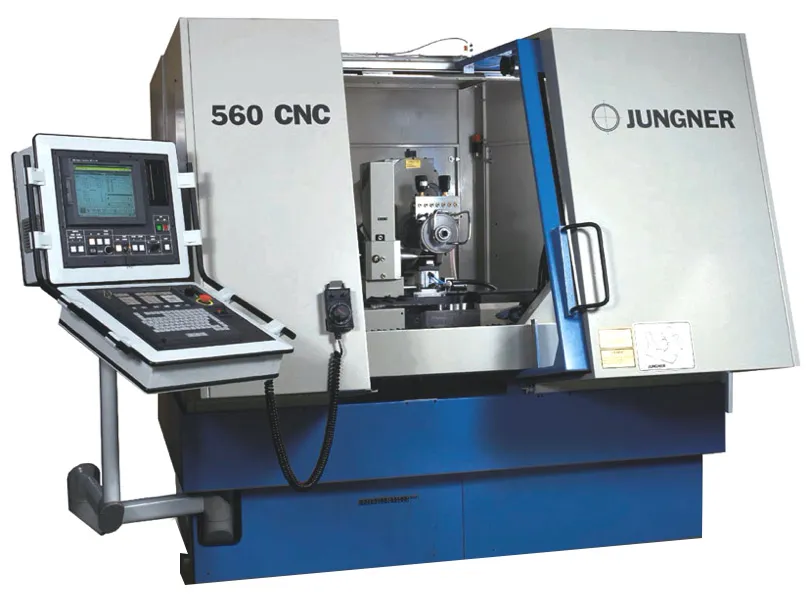 JUNGNER TG 560 CNC 5-axis precision CNC grinding machine for resharpening and manufacturing tools, cutters and broaches 5 + 1560 mm1.2 µm Technical data
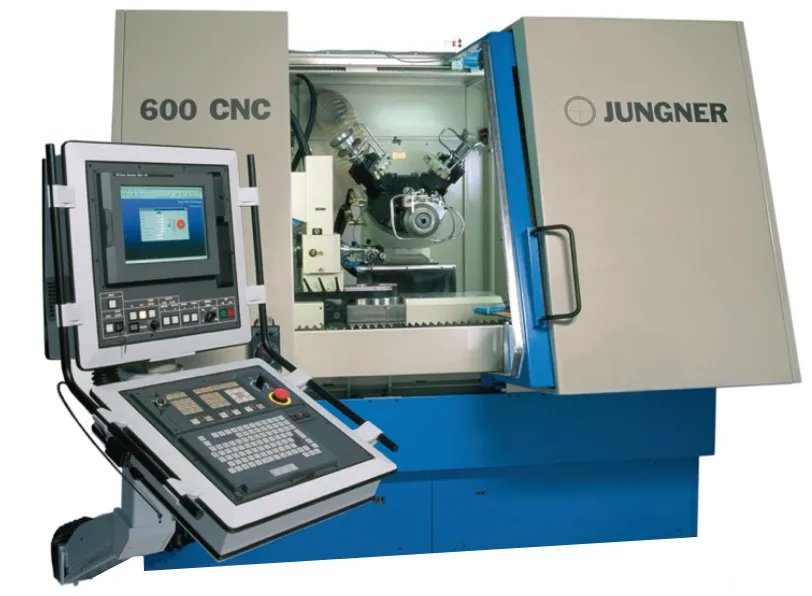 JUNGNER TG 600 CNC CNC tool and cutter grinder whose multi-spindle turret grinds complex tool geometries in one set-up 3–611–18.5 kWØ 300 mm Technical data
 JUNGNER PG 700 CNC High-precision profile cutter grinding machine for the cutters of screw pump and compressor rotors Ø 500 mm43 kW25,000 rpm Technical data