Since 198343 years serving Turkish industry

Bihler

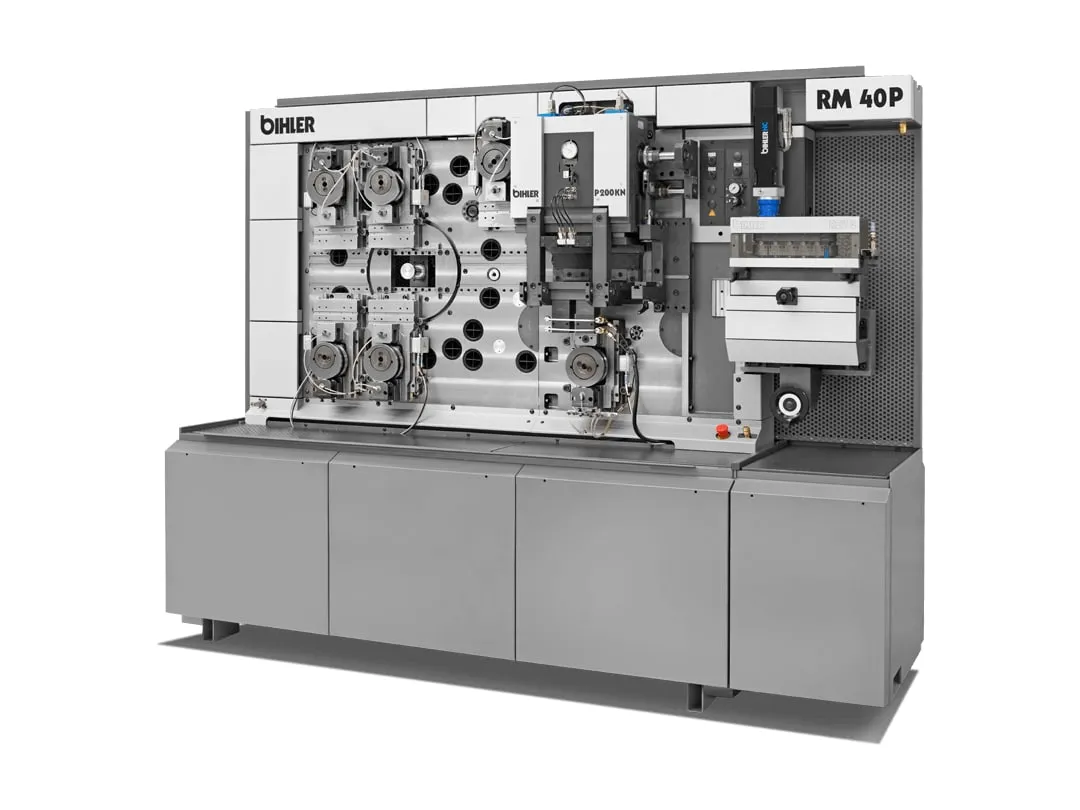
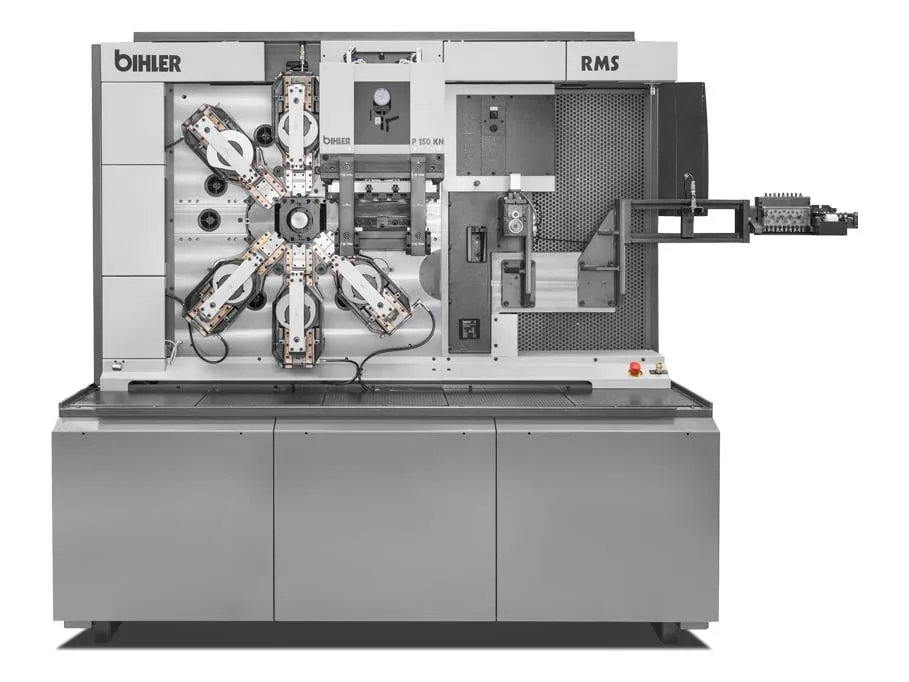
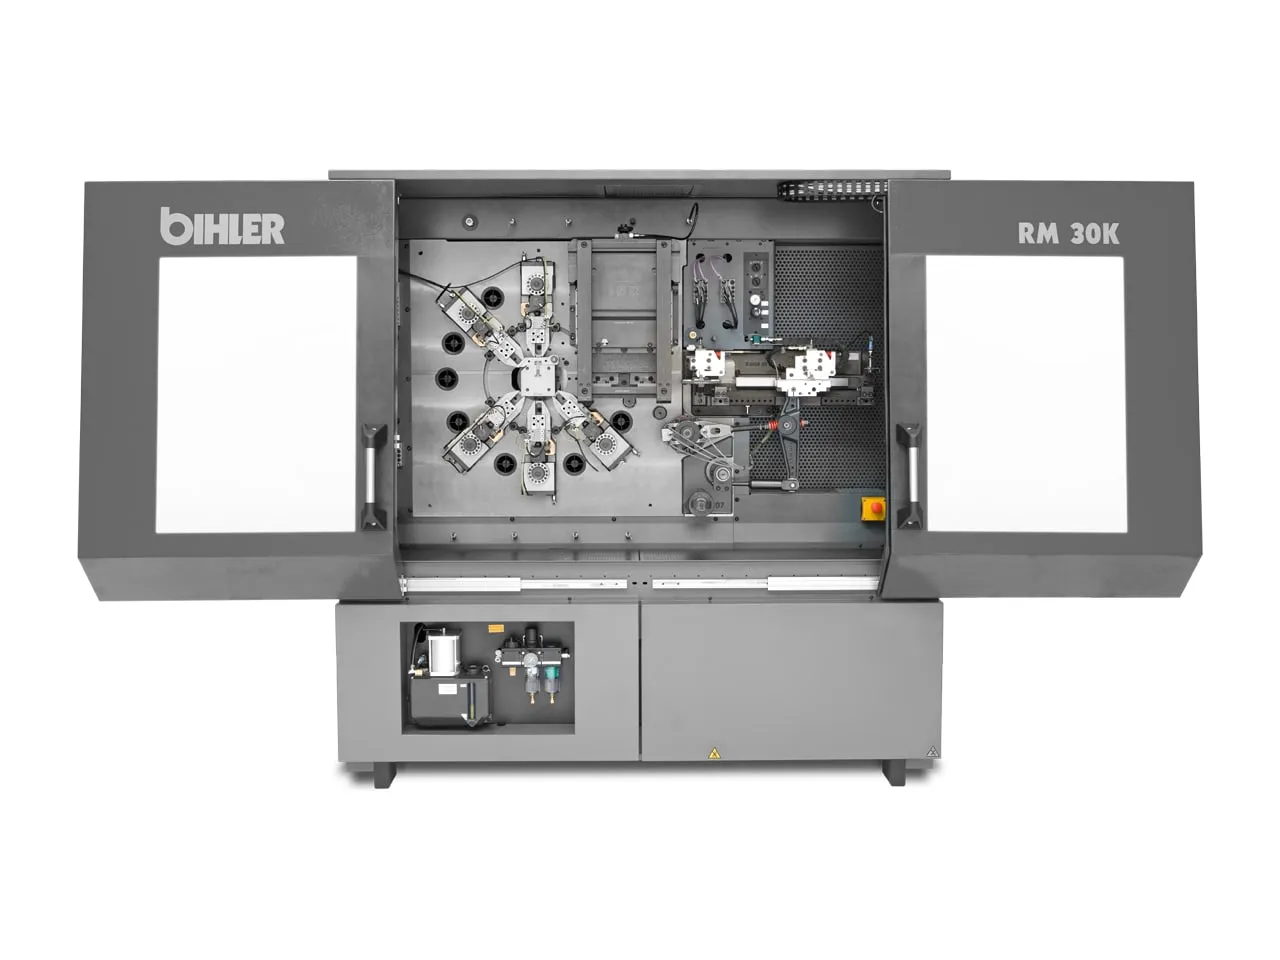
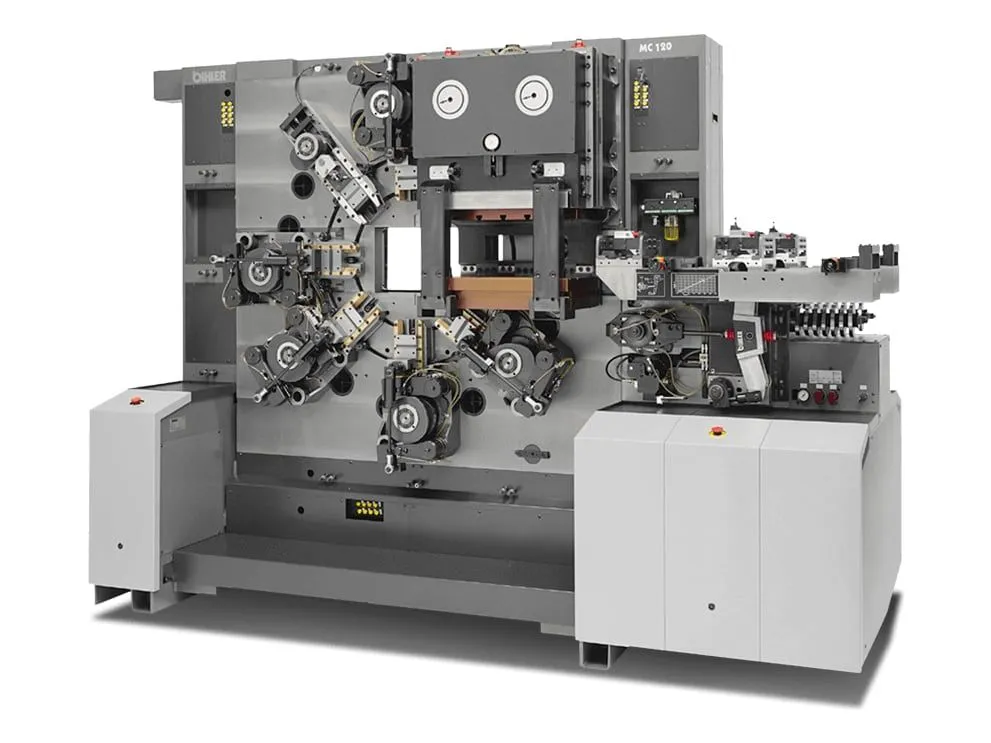
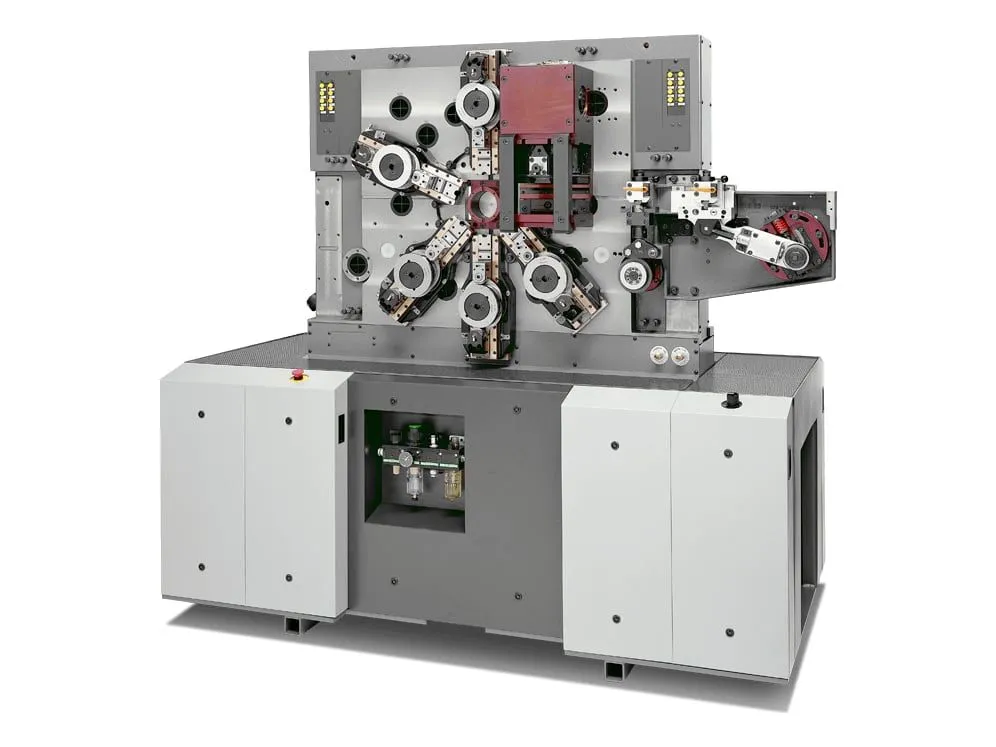
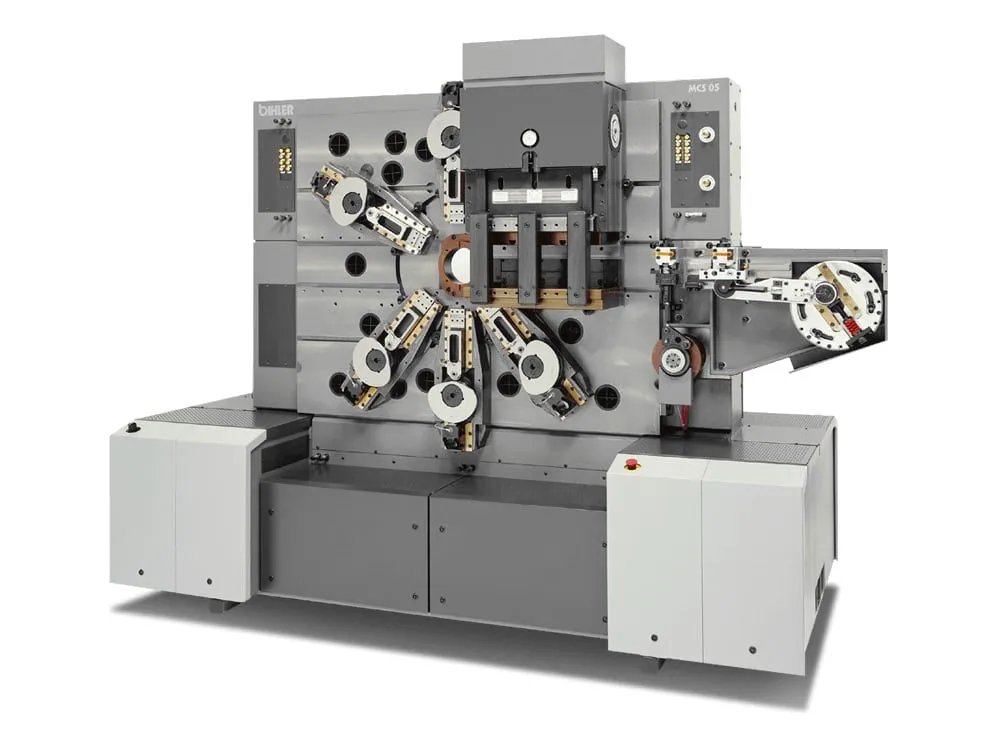
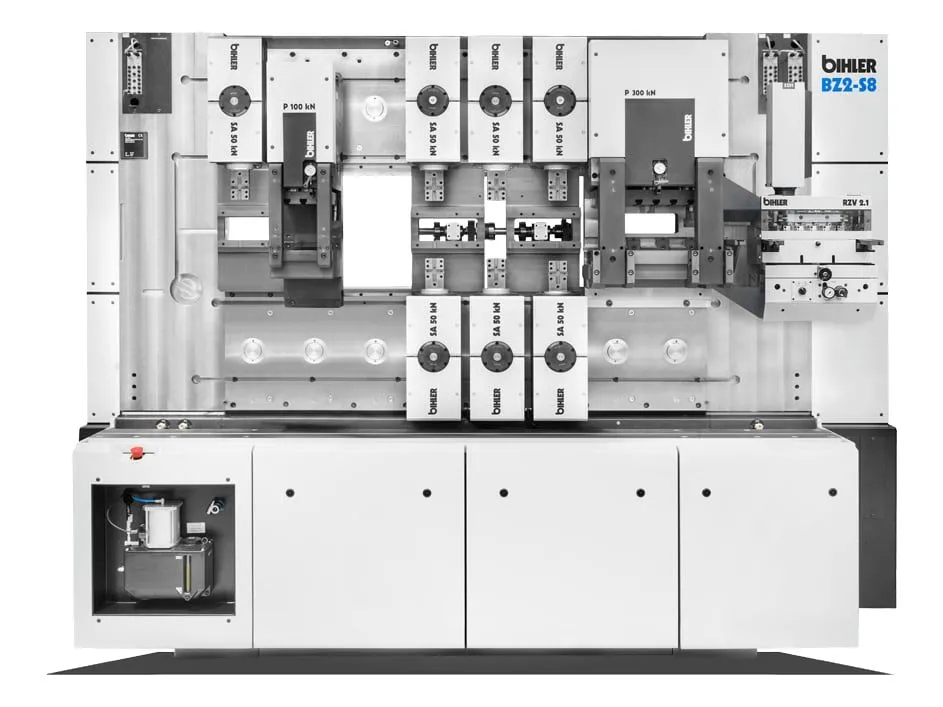
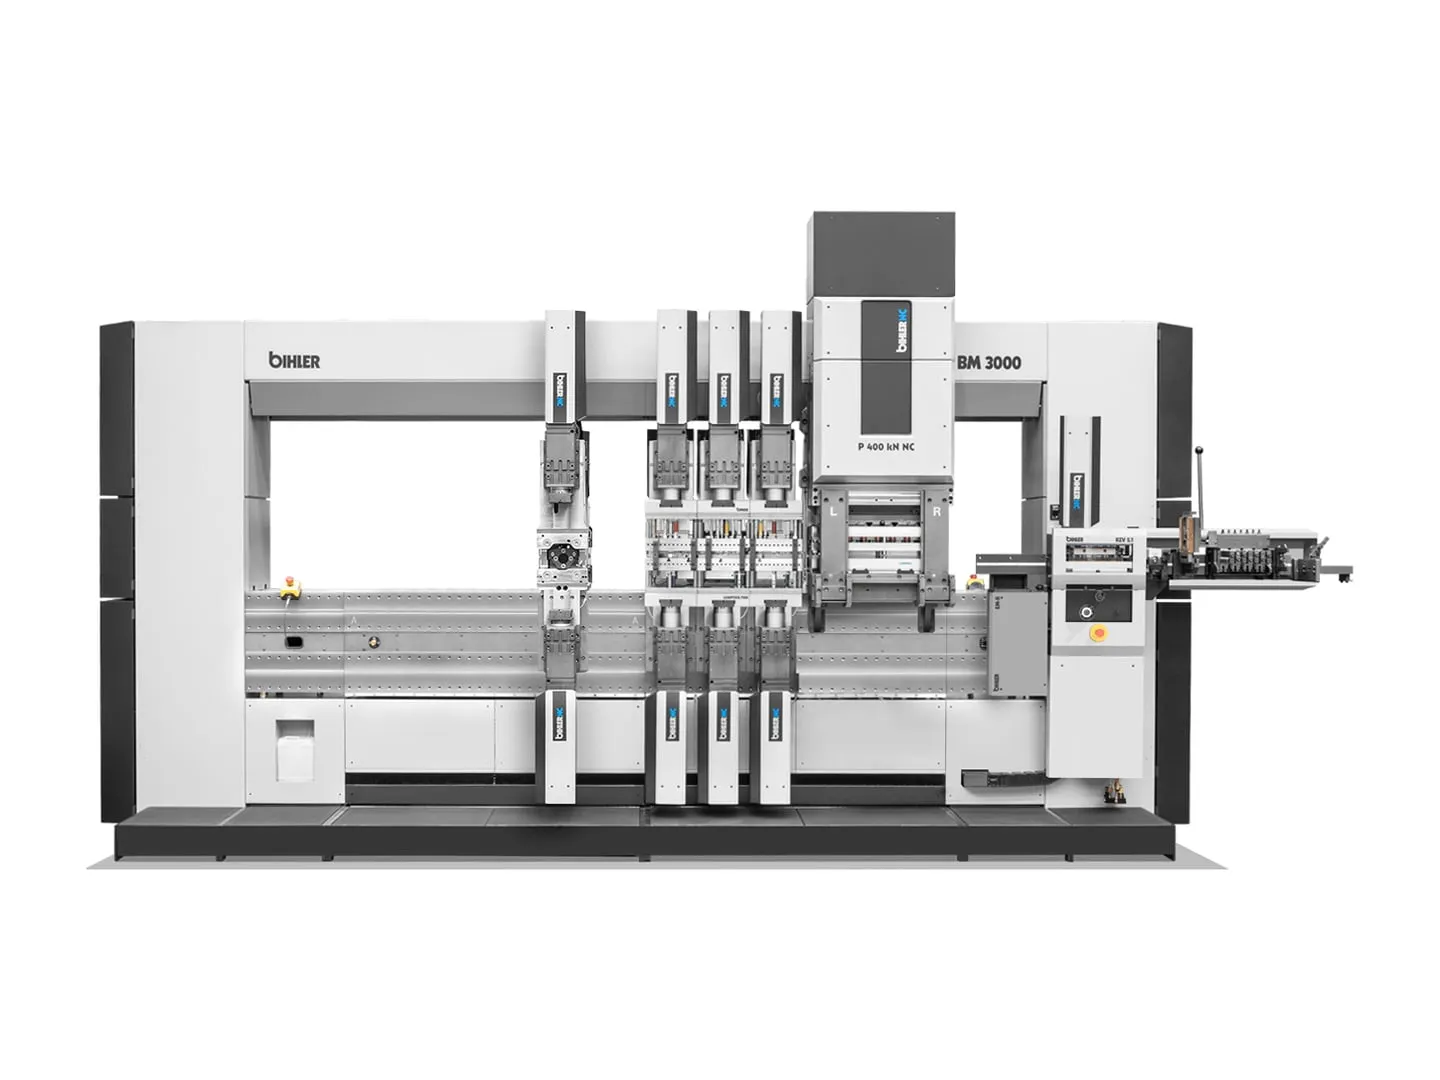
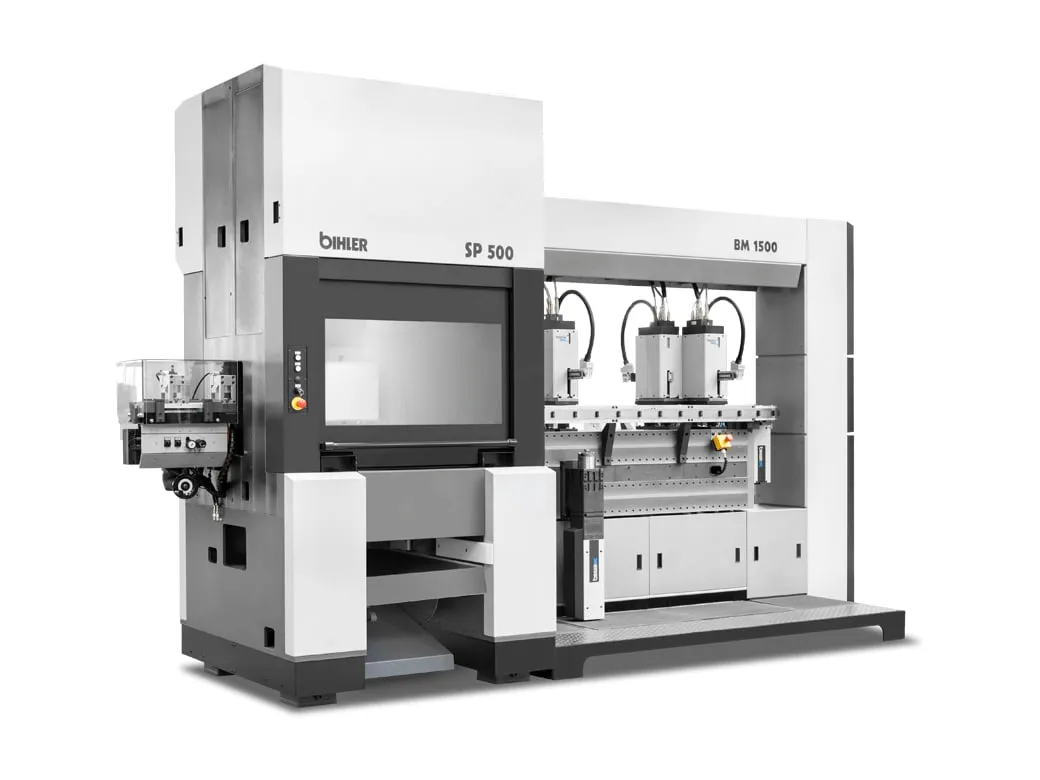
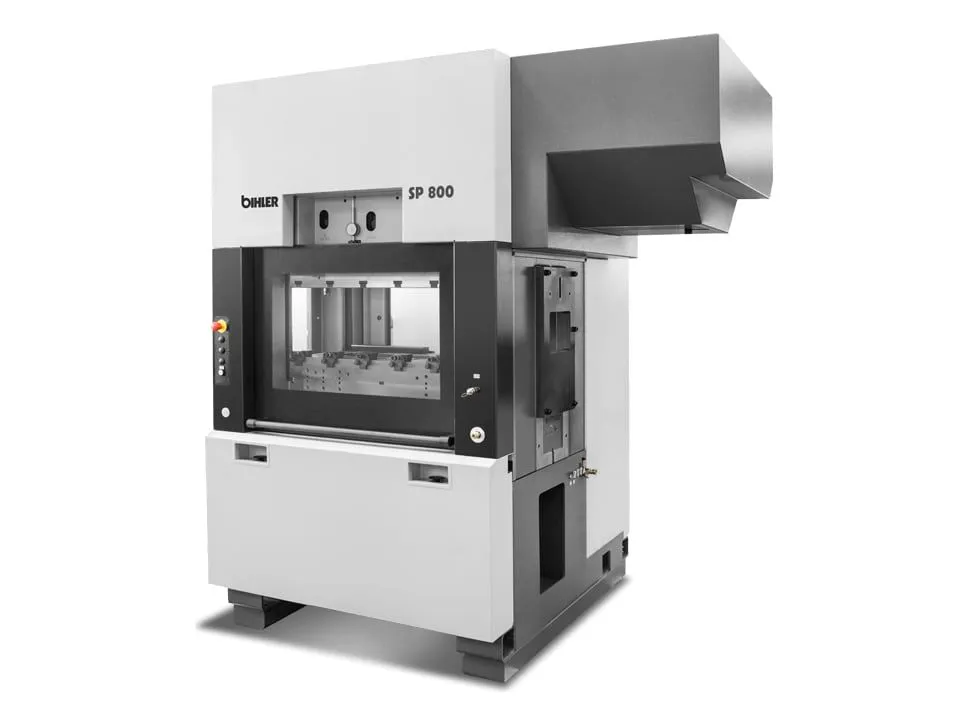
Bihler multi-slide machines and production systems

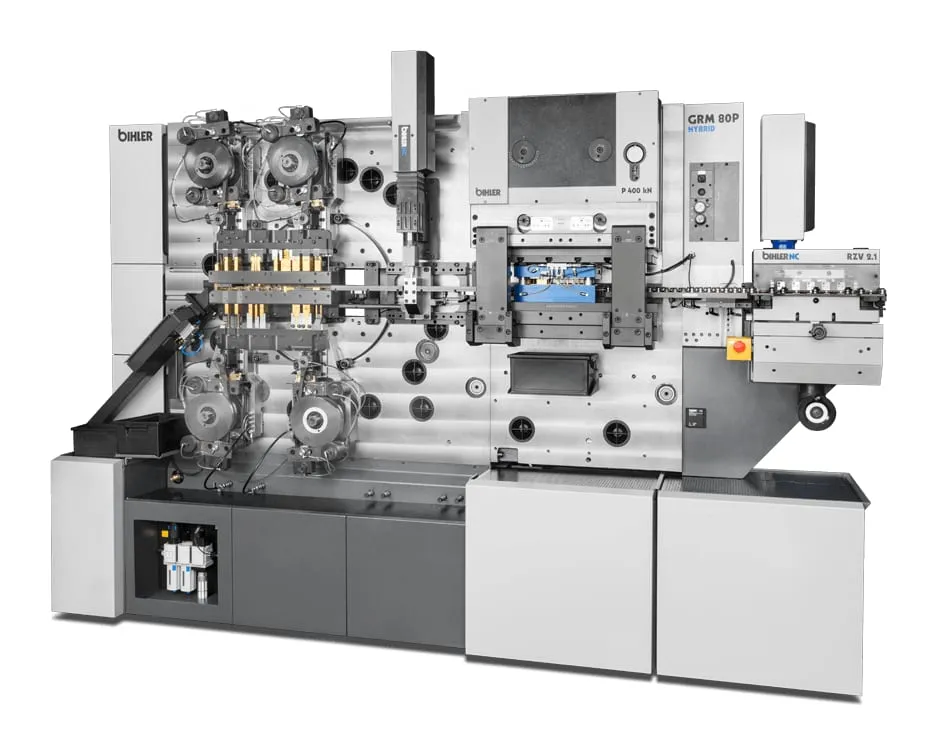
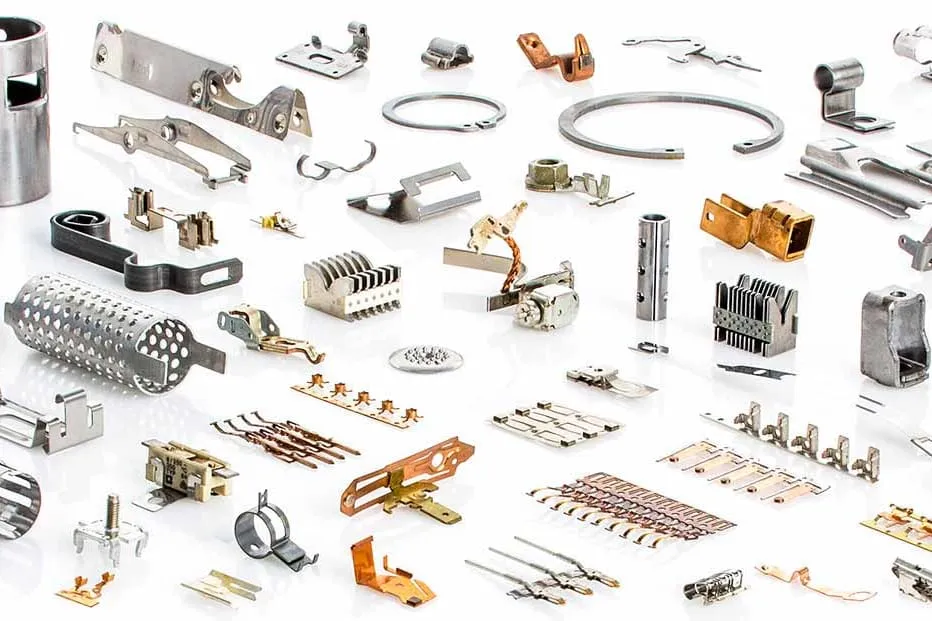
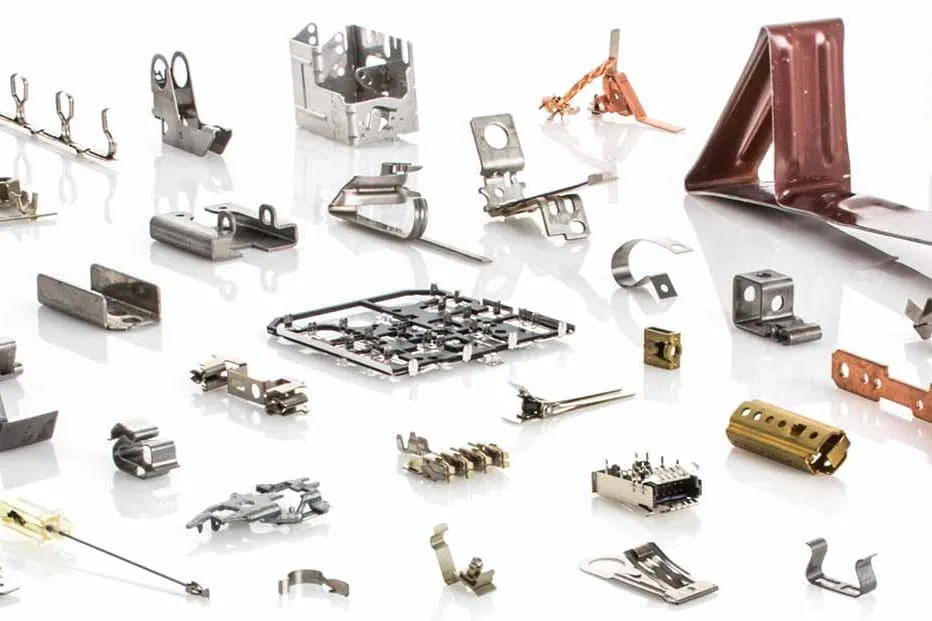
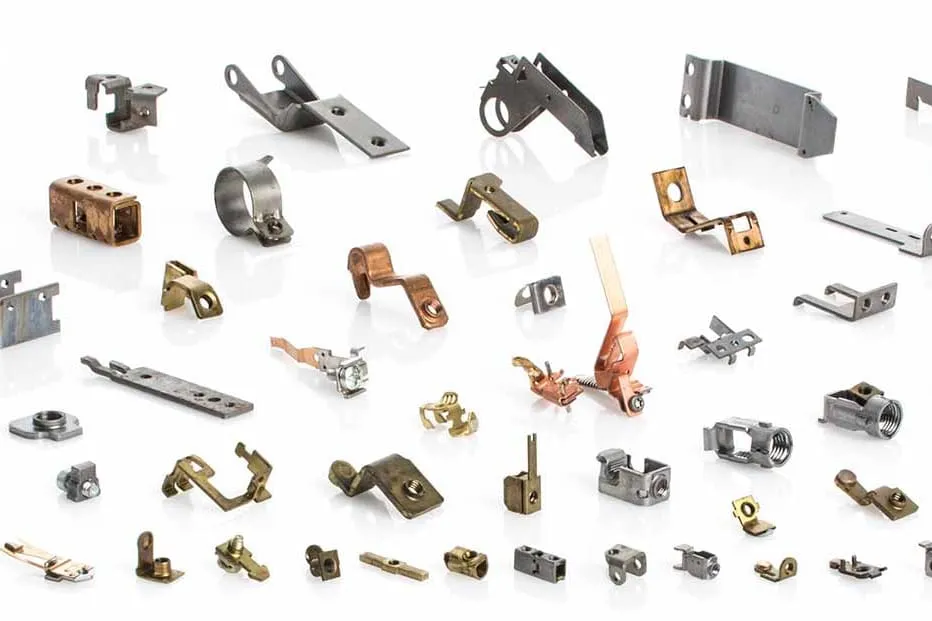
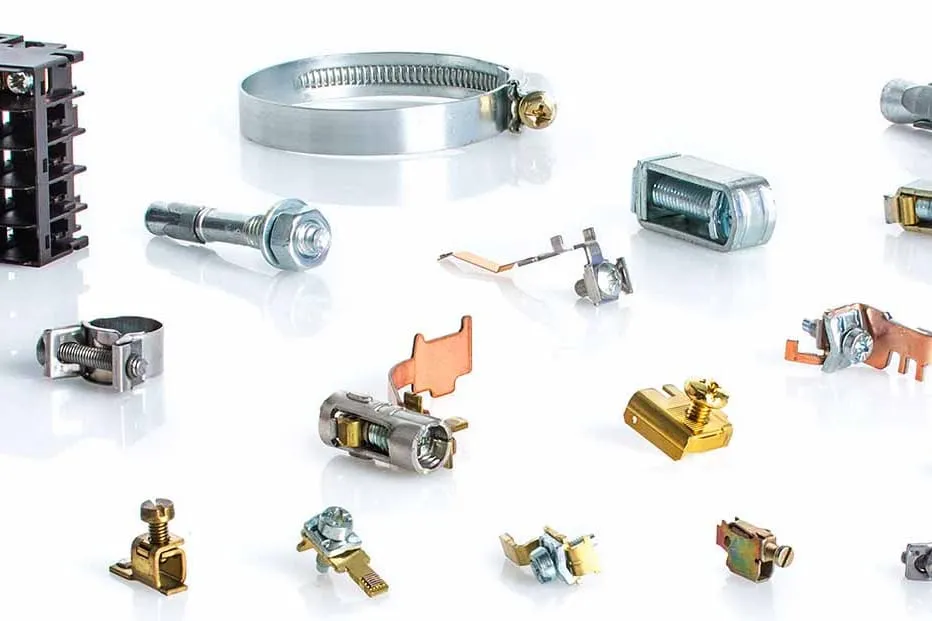
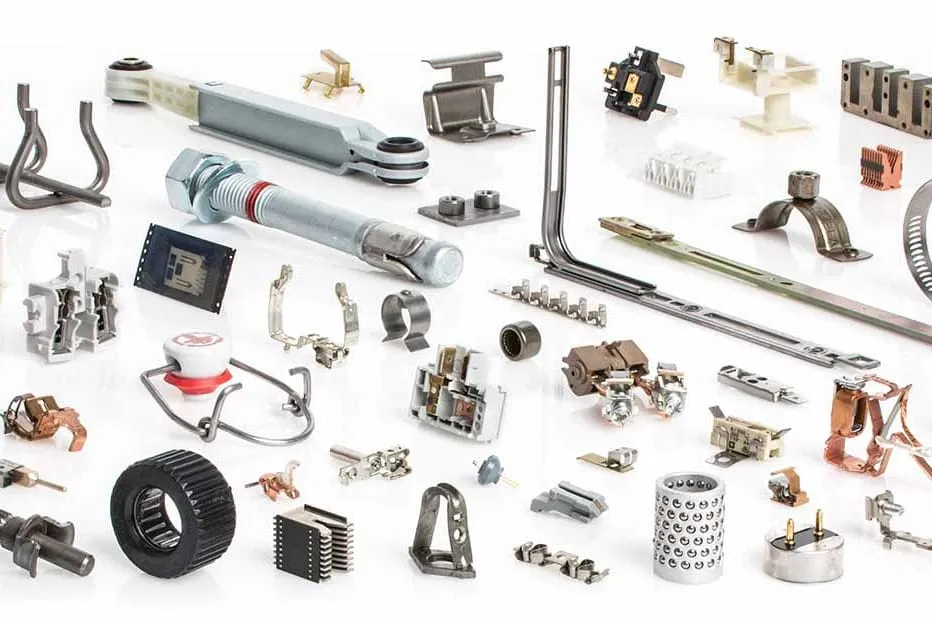
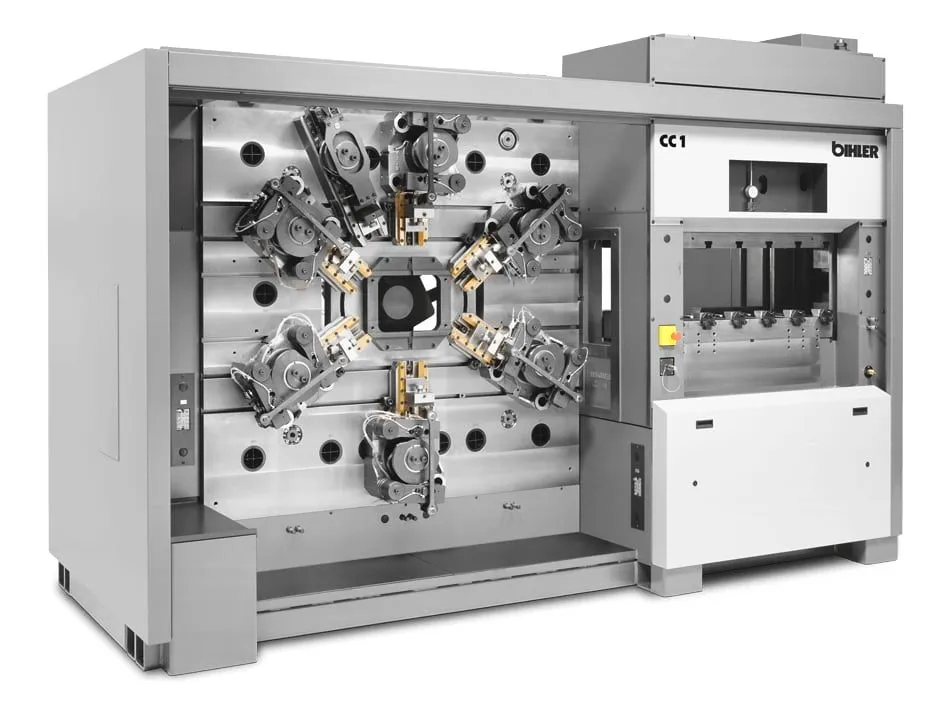
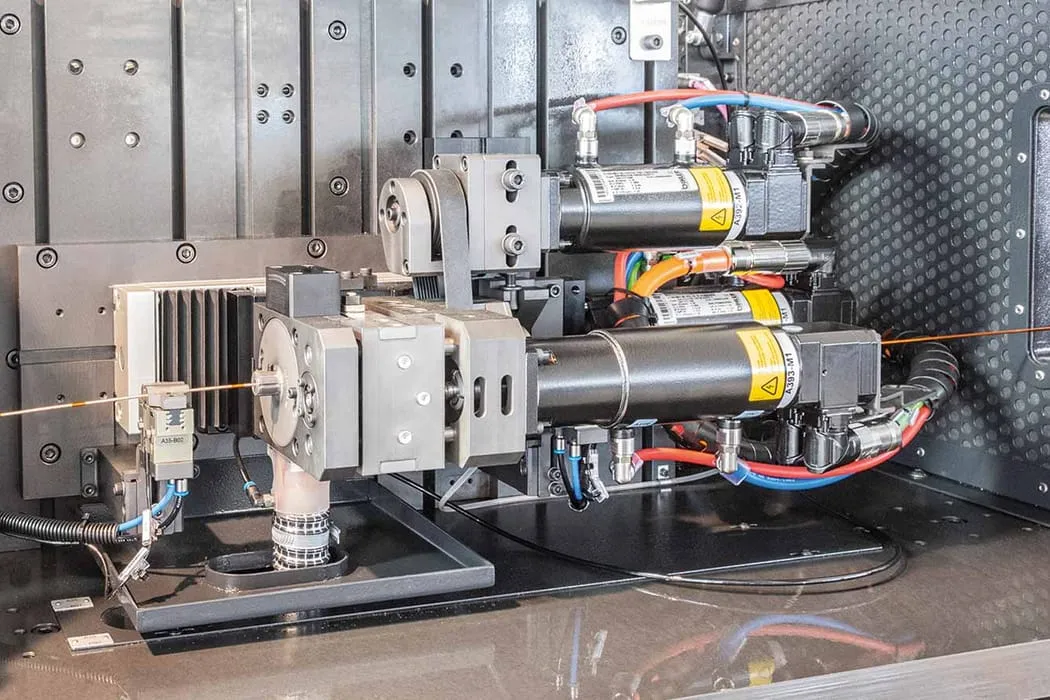
Otto Bihler Maschinenfabrik has built multi-slide machines, servo production and assembly systems and tooling technology in Halblech/Füssen (Germany) since 1953. On a Bihler machine wire or strip is fed from the coil; slides stamp, bend, weld and assemble in sequence. Complex bent parts that a press cannot make with a single die are produced in one operation, hundreds per minute.

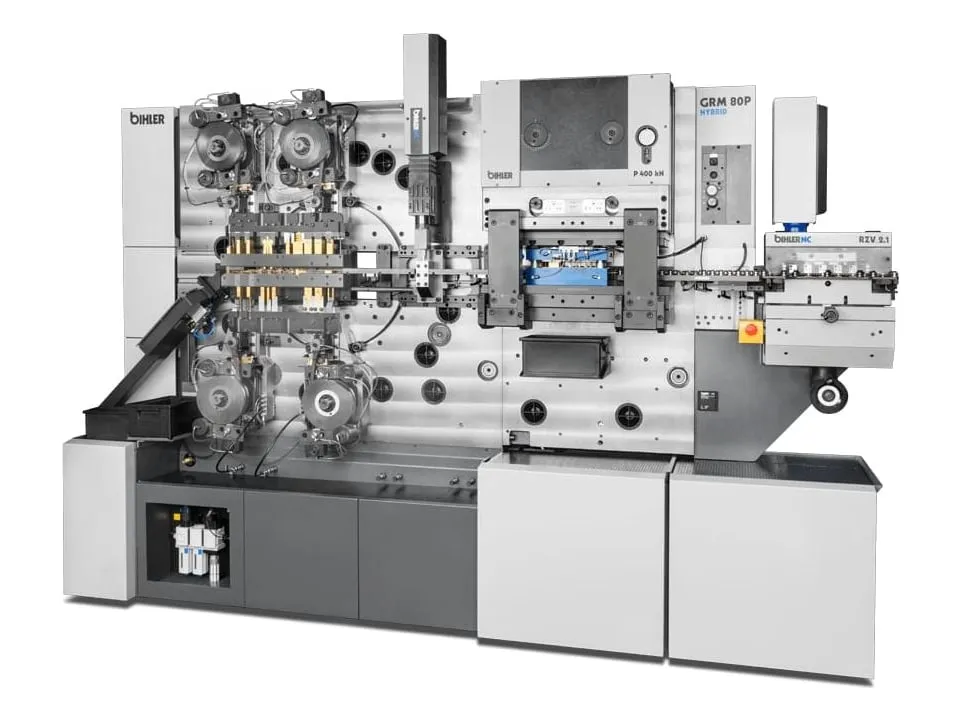
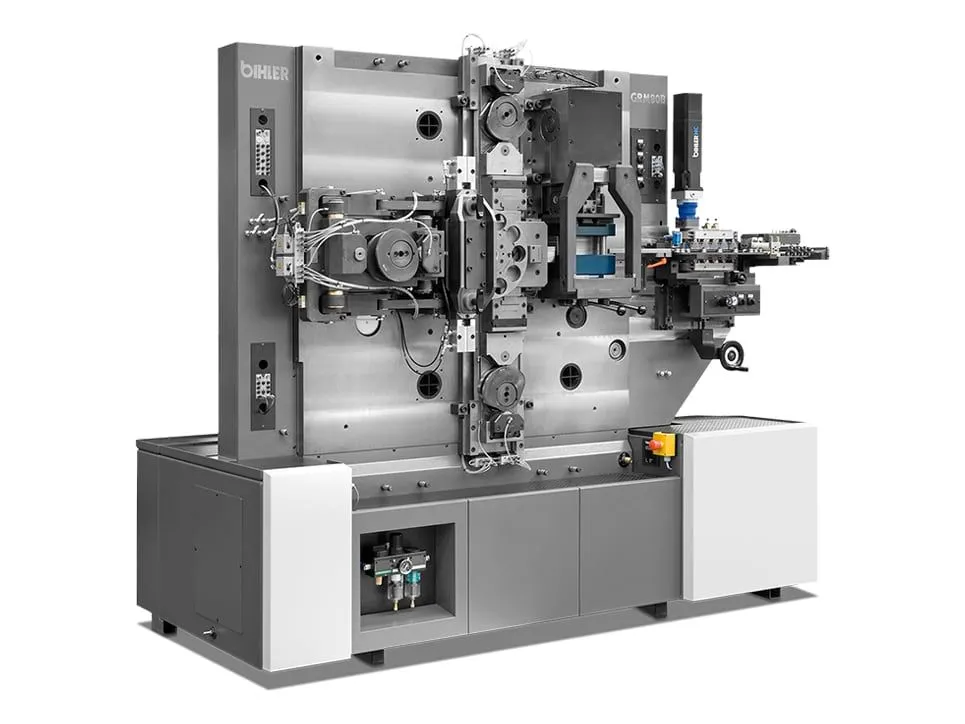
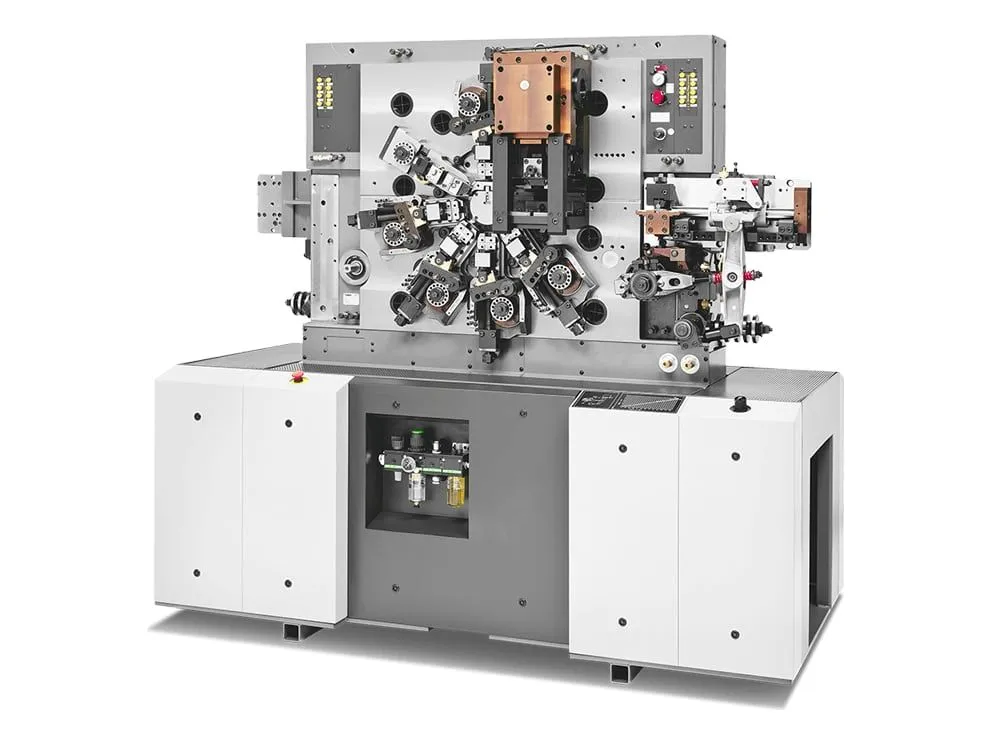
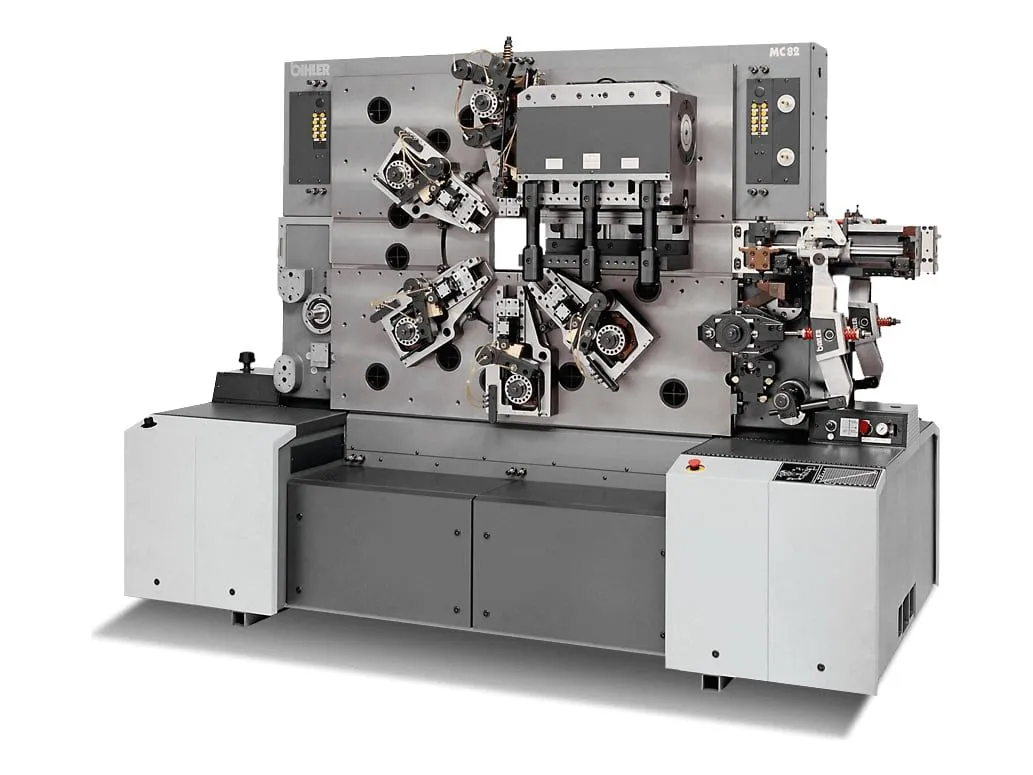
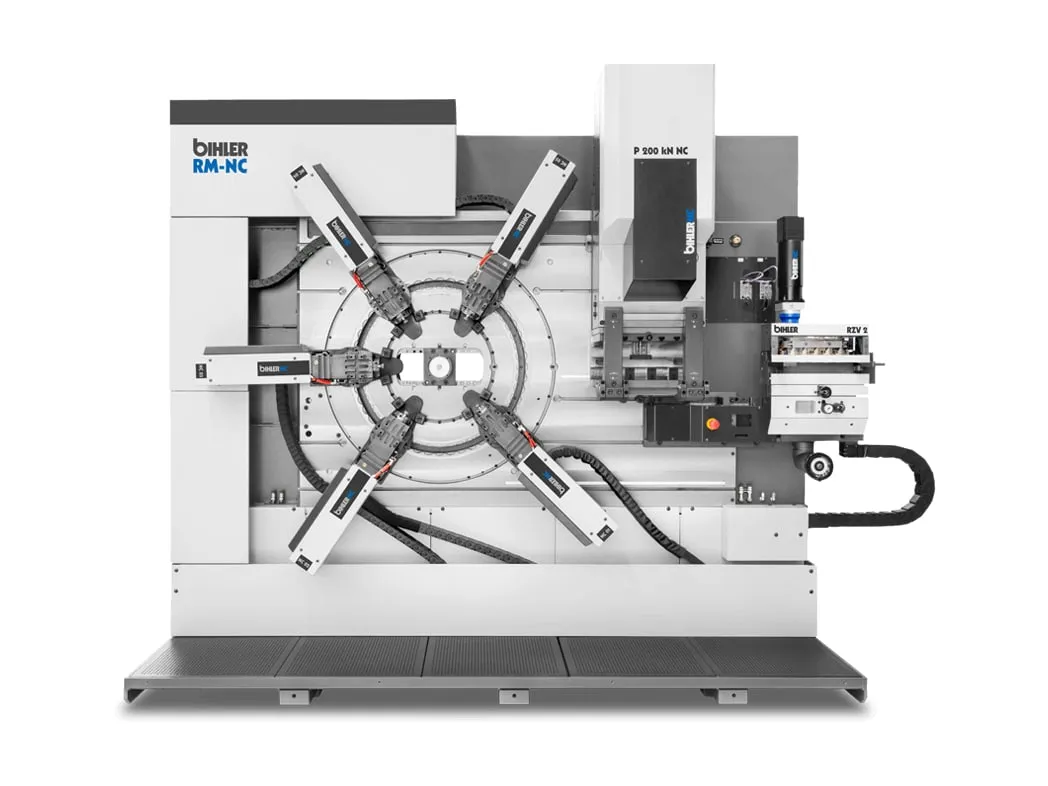
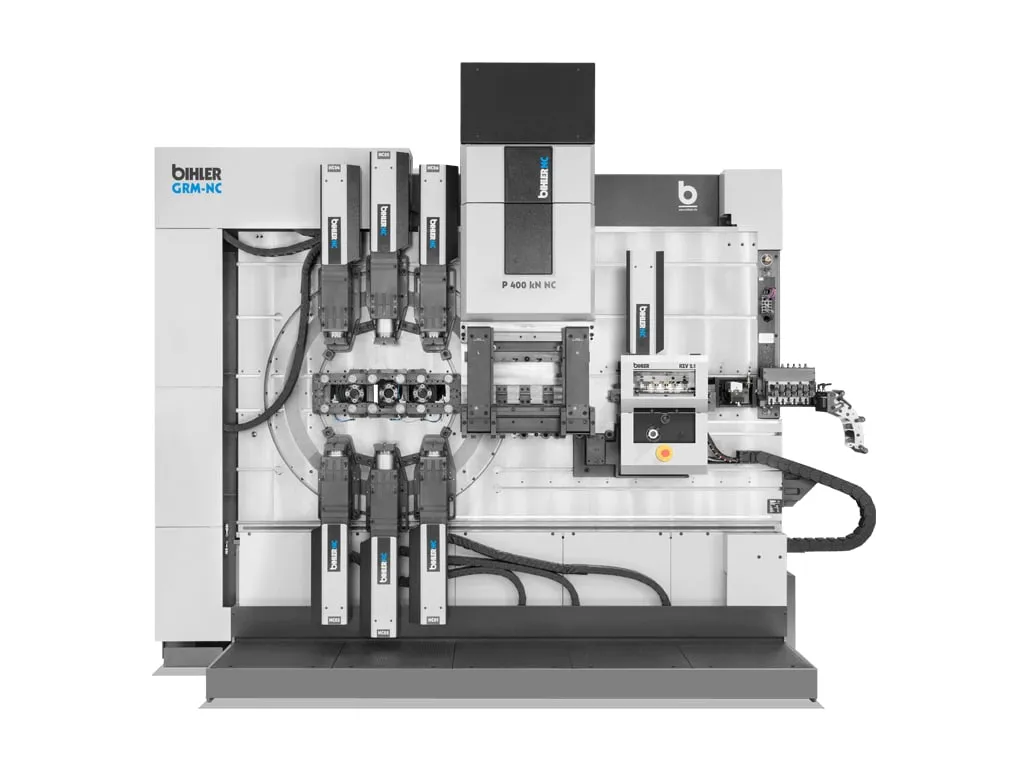
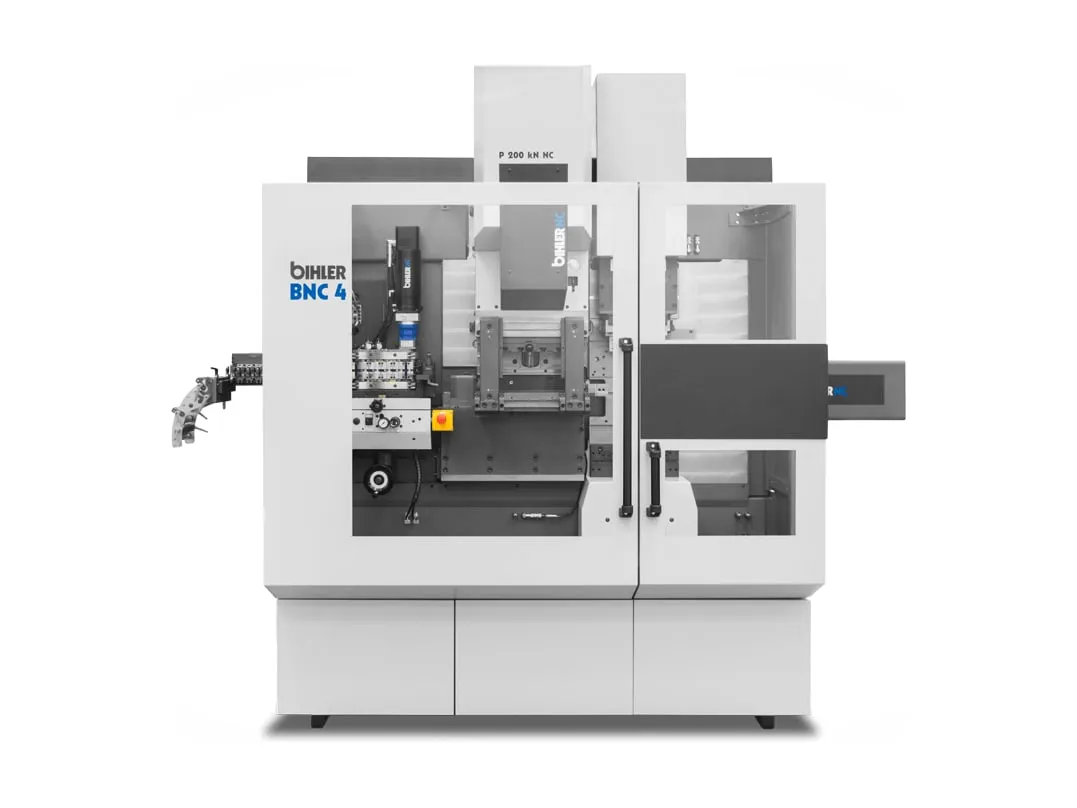
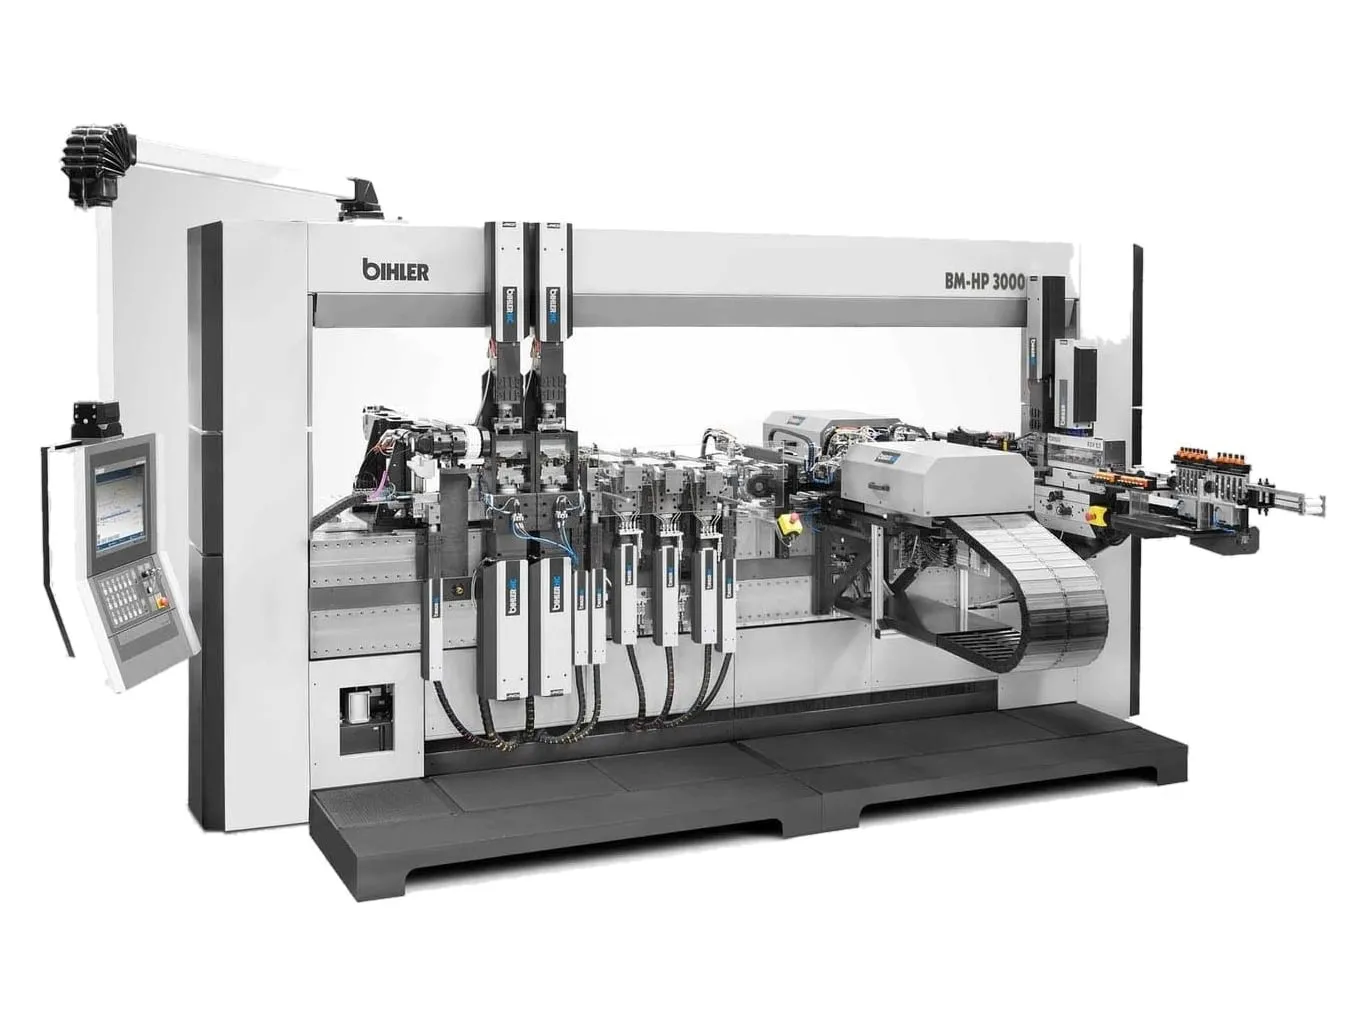
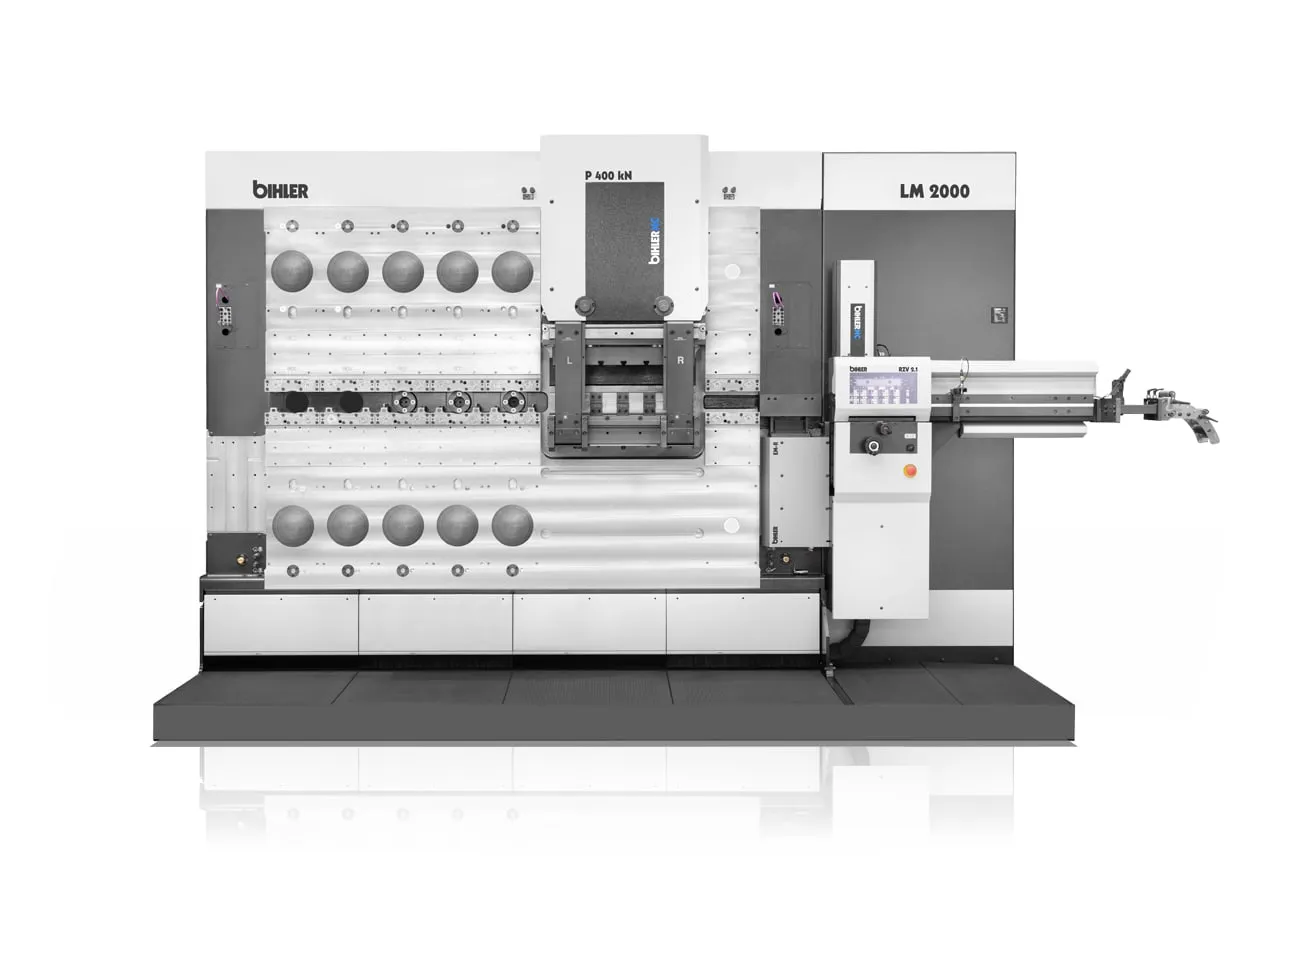
Today, with more than 750 employees, Bihler offers mechanical and hybrid GRM/RM machines, servo-controlled RM-NC and GRM-NC machines, LM 2000 linear machines, Multicenter machines and processing centres, BIMERIC production and assembly systems and the BM-HP 3000 line for electric-motor hairpins.
IndustriesE-mobilityAutomotiveElectrical engineeringConnectors and contactsMetal goodsHousehold technologyMedical technologySprings and wire goods

Headquarters
Germany – Halblech/Füssen
Founded
1953
Employees
750+
Web
www.bihler.de
Bihler – Multi-slide forming, welding and assembly systems

Workpieces

Workpieces produced on Bihler machines

Choose your industry; the cards are filtered accordingly.

24 workpieces
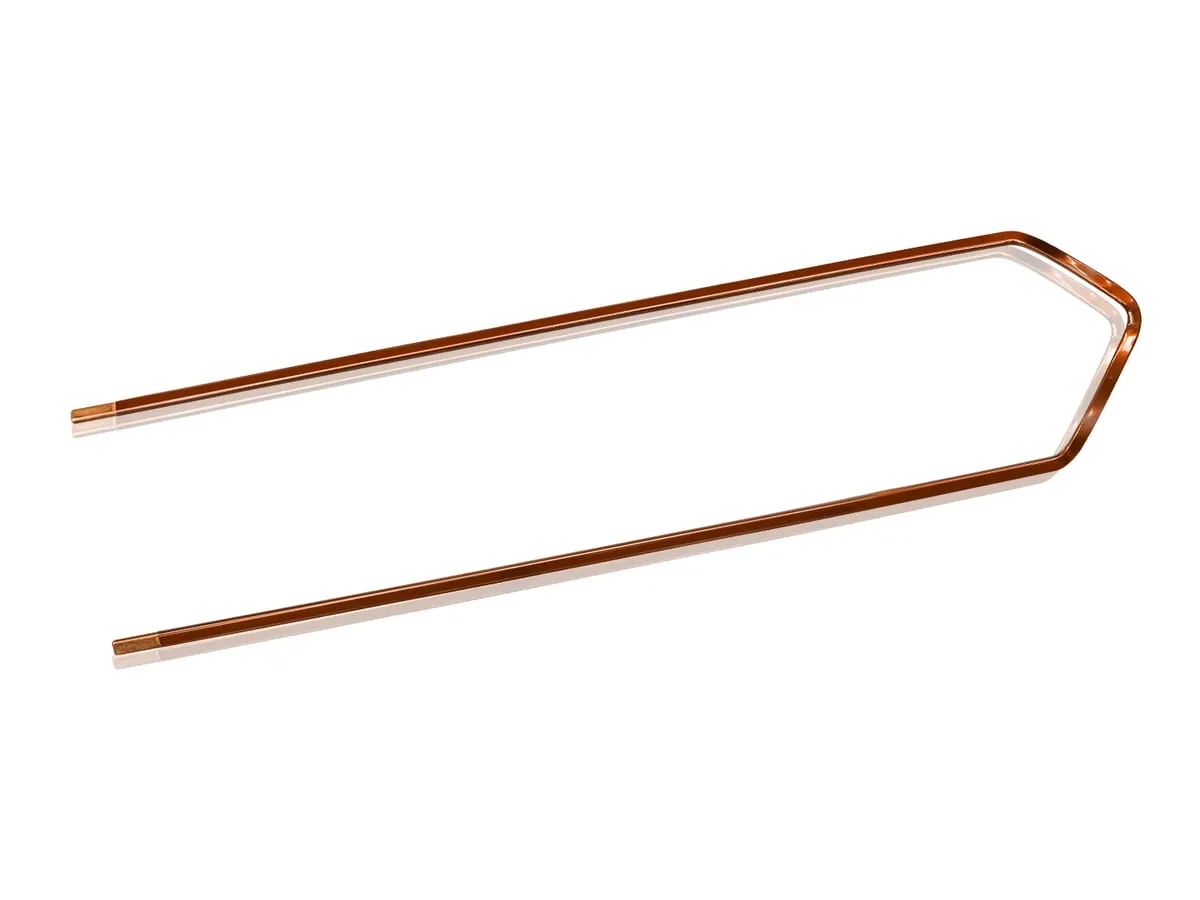
Hairpin stator winding elements

Hairpin stator winding elements

Winding elements for electric motor stators. Straightening, feeding, cutting, enamel stripping, 2D pre-bending and 3D bending of flat wire in one line; 60–120 hairpins per minute, type change on the fly.

Copper and aluminium busbars

Copper and aluminium busbars

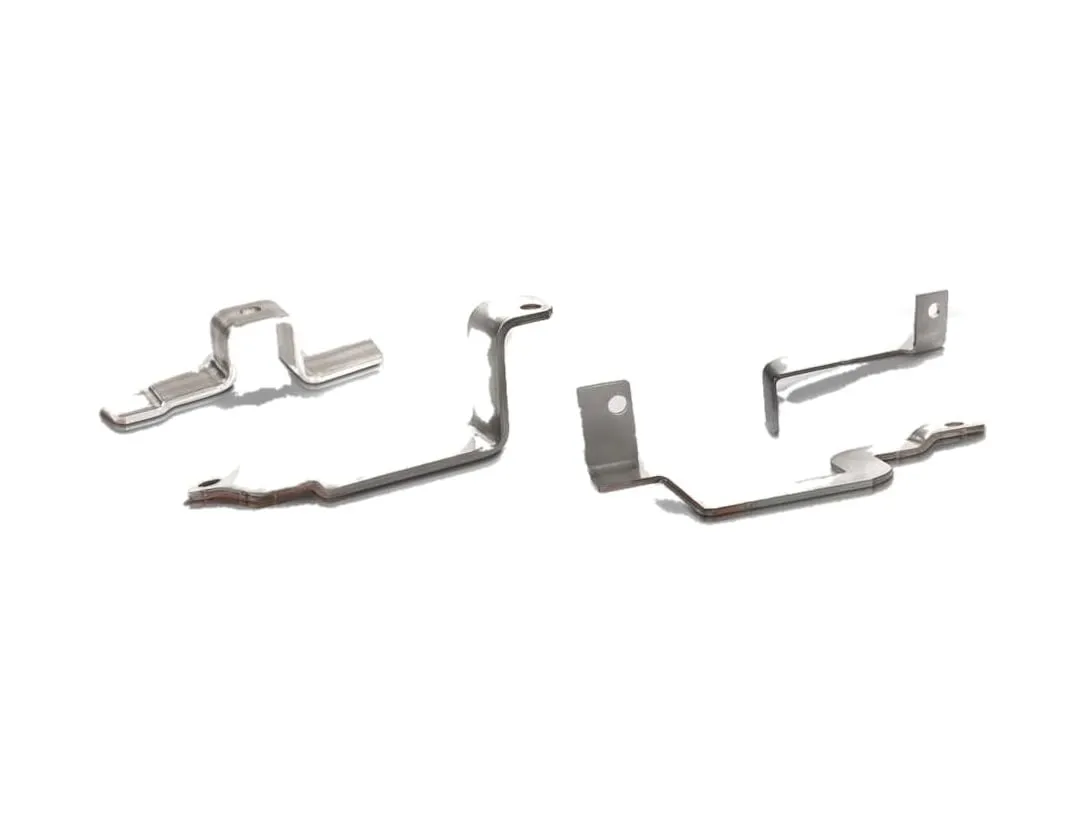
Current-carrying copper and aluminium busbars for e-mobility, up to 4 mm thick. In radial production the strip is as wide as the part, saving up to 50% material.

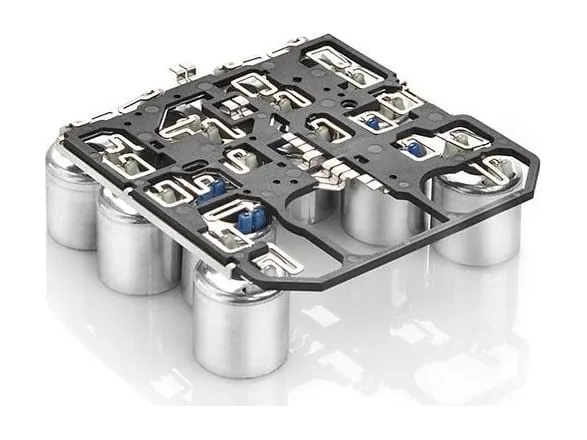
Battery cell and module connectors

Battery cell and module connectors

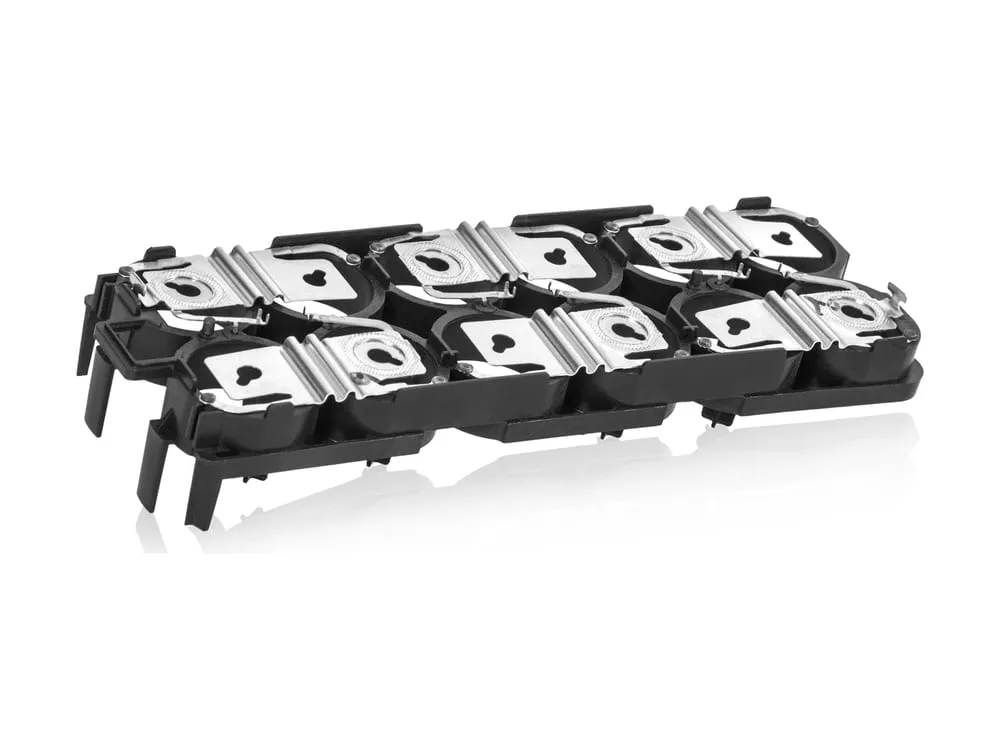
The cell-contacting system that links the cells of a traction battery: low losses, tolerance compensation between cells, fast assembly. Connectors come out produced and mounted in the carrier frame.

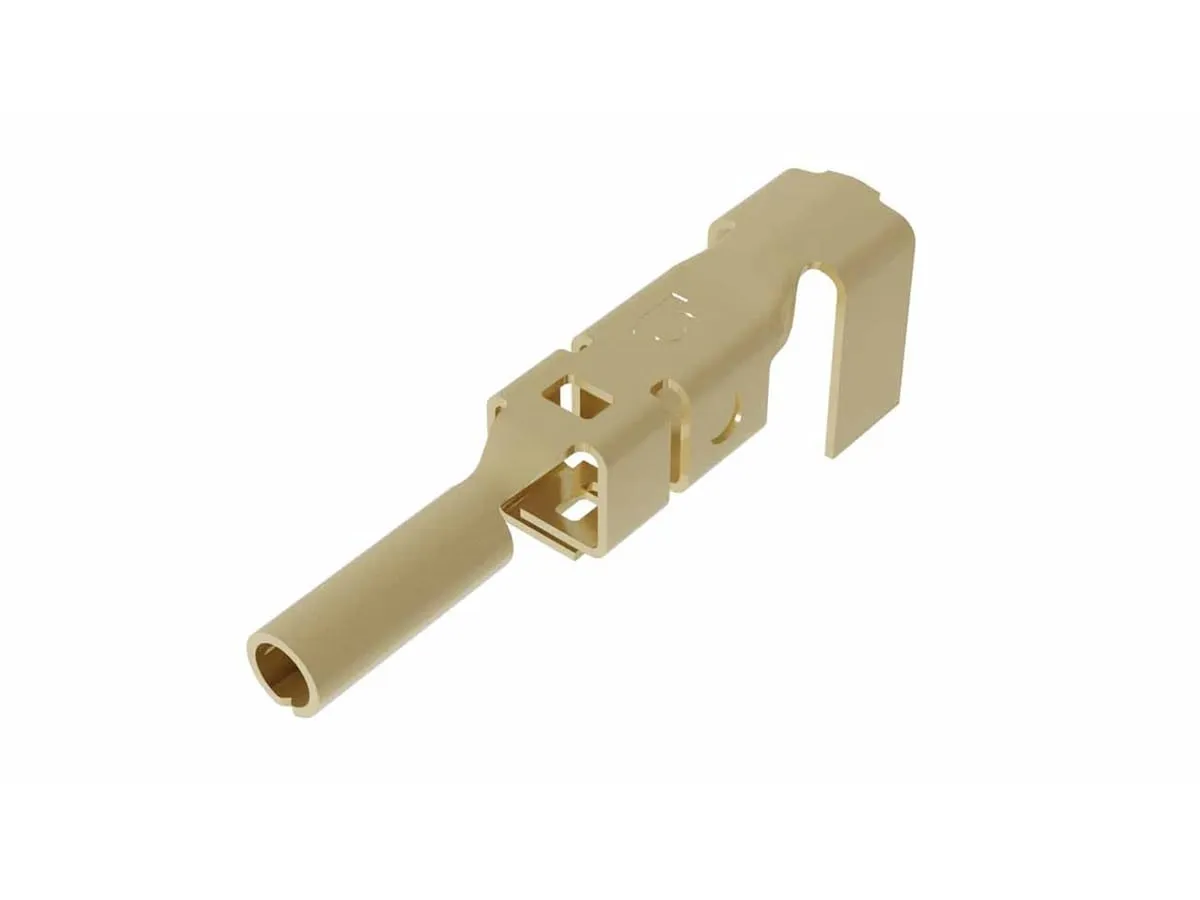
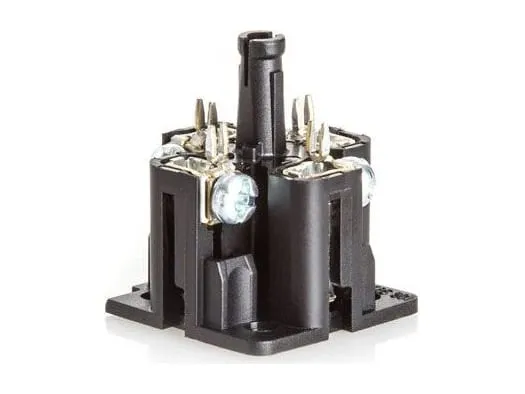
Socket, switch and earthing contacts

Socket, switch and earthing contacts

For example the six-part Schuko earthing contact, which touches before the live pins. The bracket is stamped and bent; contact lugs, retaining spring and plastic part are fed in, assembled and camera-checked.
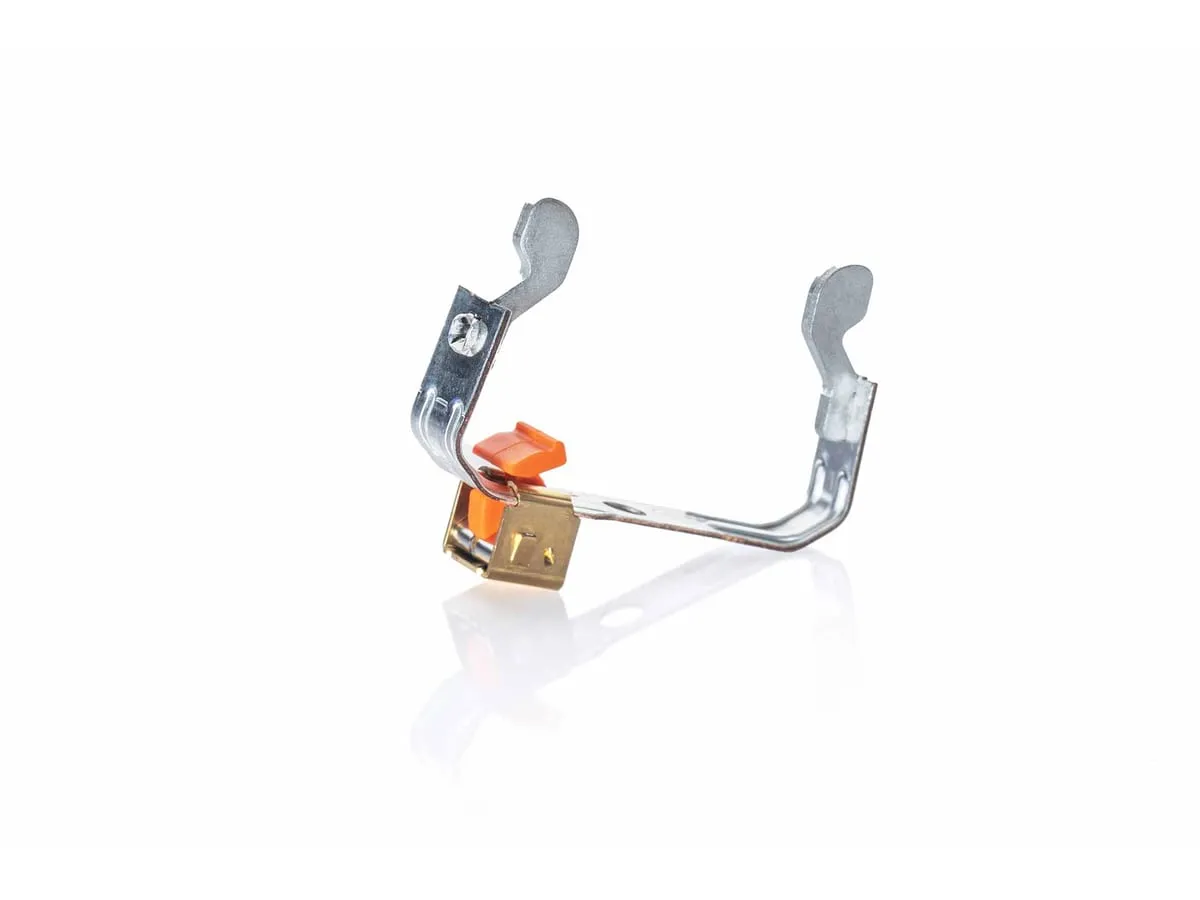
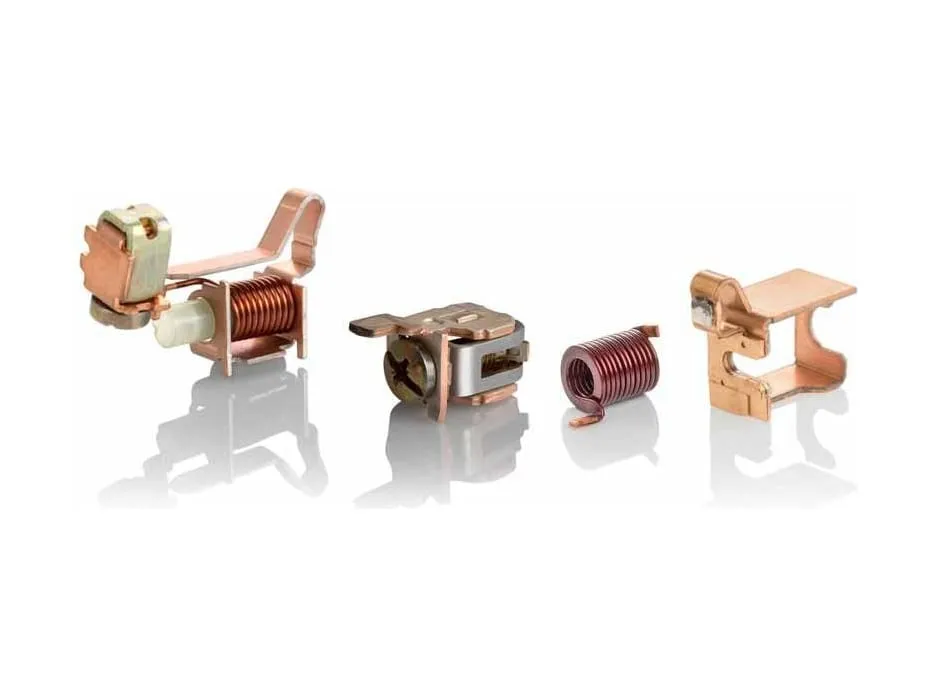
Circuit breaker components

Circuit breaker components

Magnetic assembly, trip mechanism, thermal assembly, arc-extinguisher plates and terminals of circuit breakers, which cut the current on overload (bimetal) or short circuit (electromagnetic).

ESP coil assemblies

ESP coil assemblies

ESP valves need precise control. The coil assembly is built in one system from component feeding to finished parts on pallets, at 1.5 s per part; retooling takes minutes.
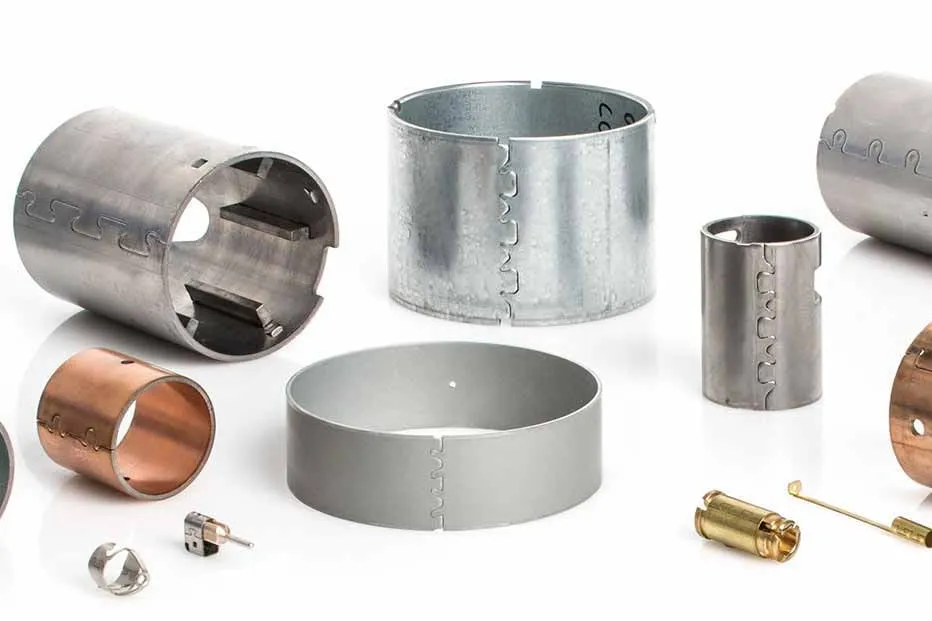
Plain bearing bushings

Plain bearing bushings

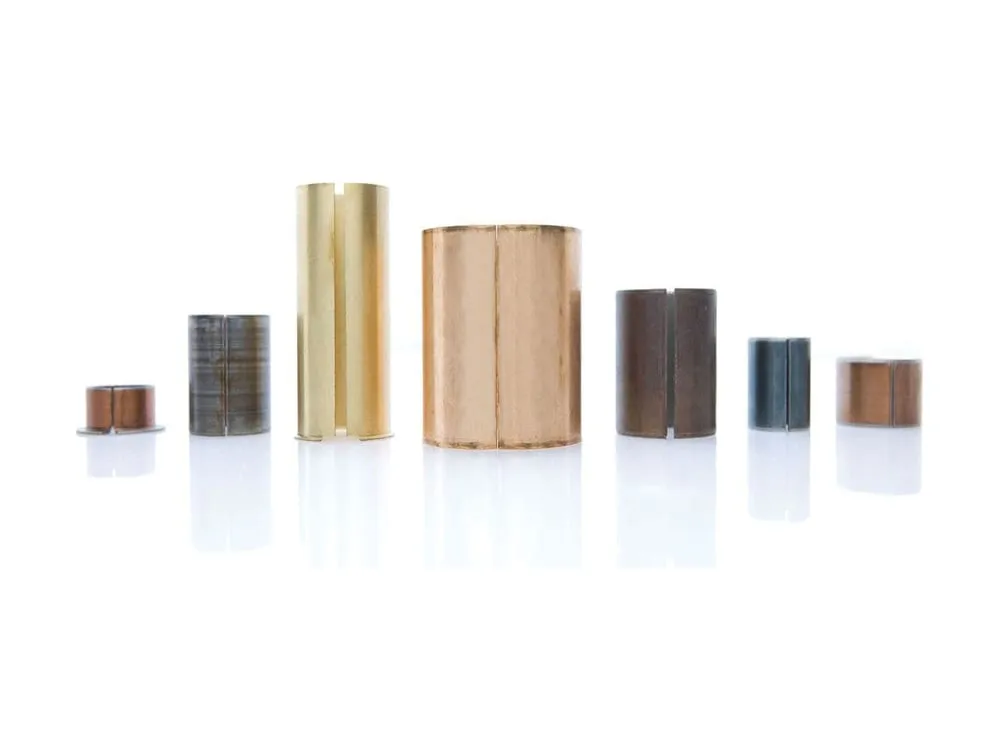
Cylindrical plain bearing bushes, with or without flange, cut, bent and calibrated from composite sintered strip. A bushing machine makes 220 straight or 160 flanged bushes per minute.
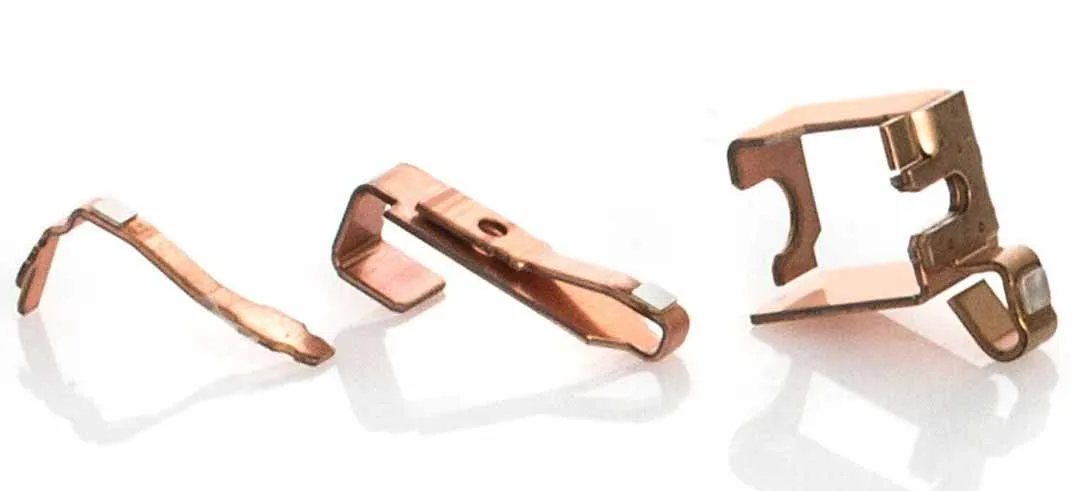
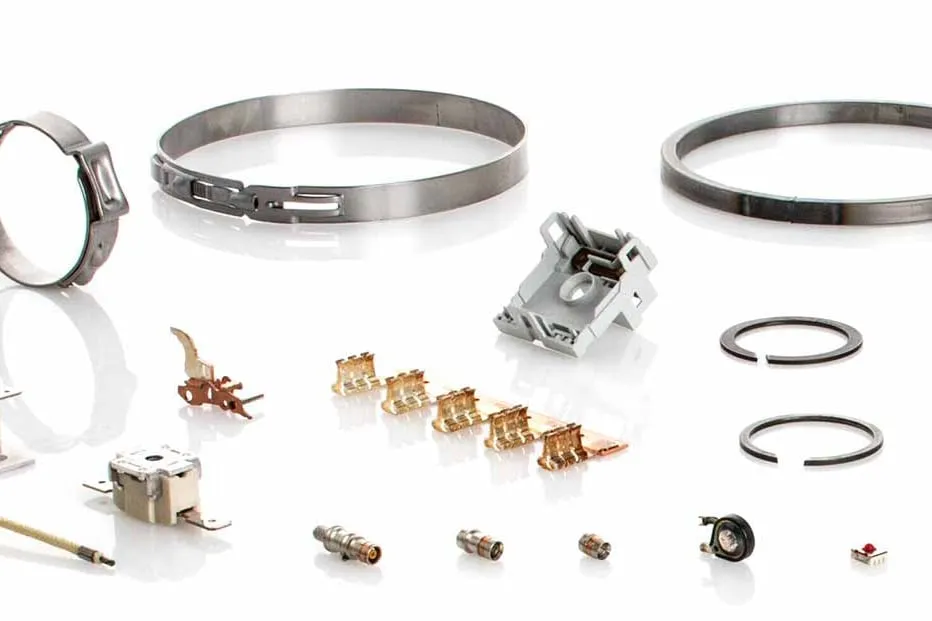
Hose clamps

Hose clamps

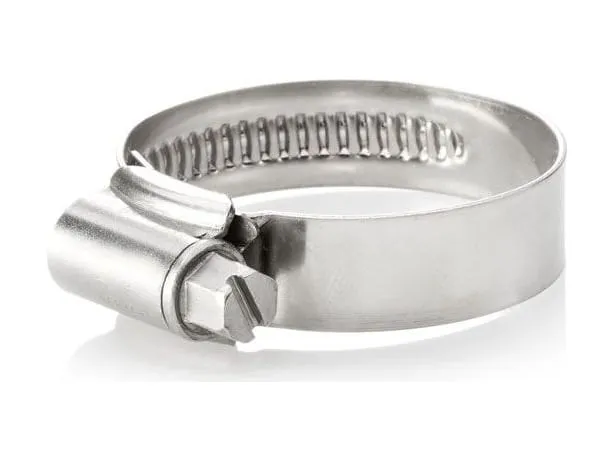
Worm-gear hose clamps whose screw engages perforations or embossed grooves in the band. One system delivers 100 fully assembled clamps per minute, Ø 8–120 mm; setup under 30 minutes.

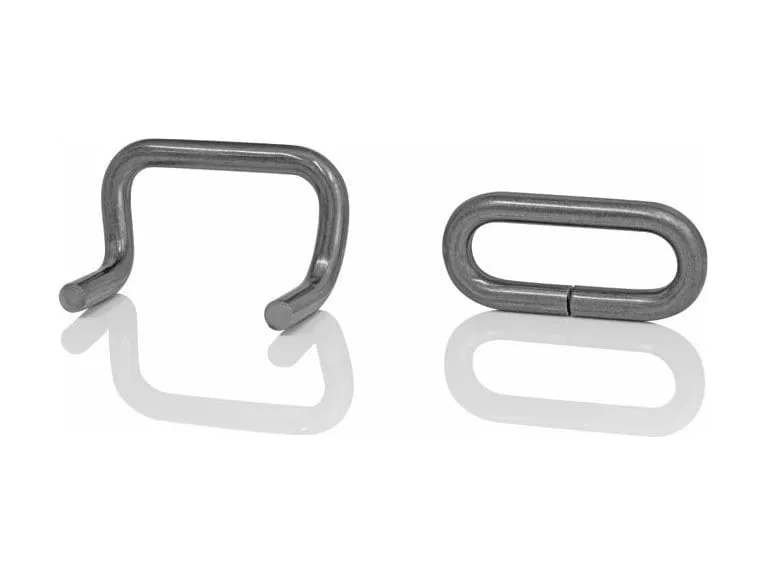
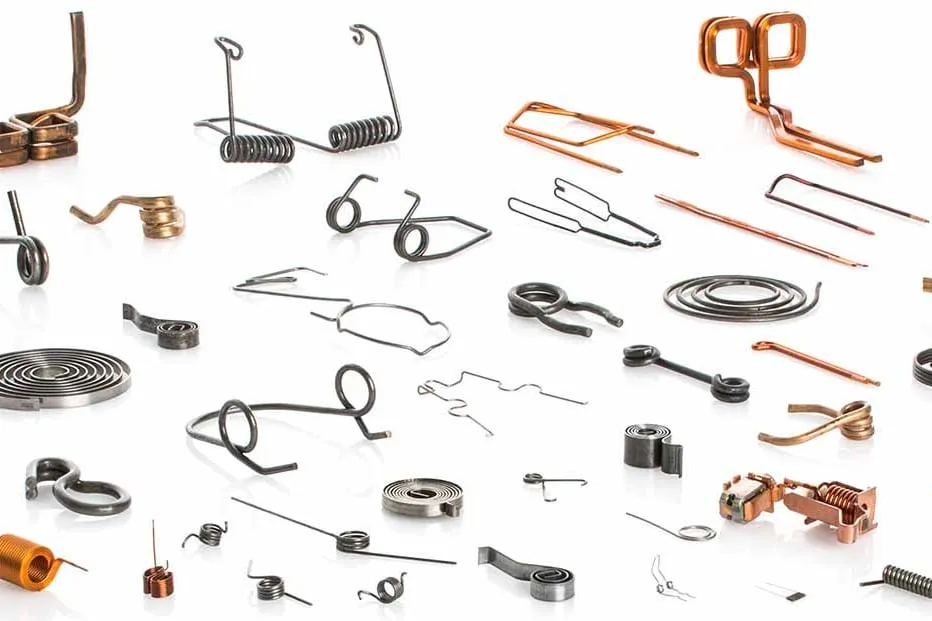
Wire springs and wire-formed parts

Wire springs and wire-formed parts

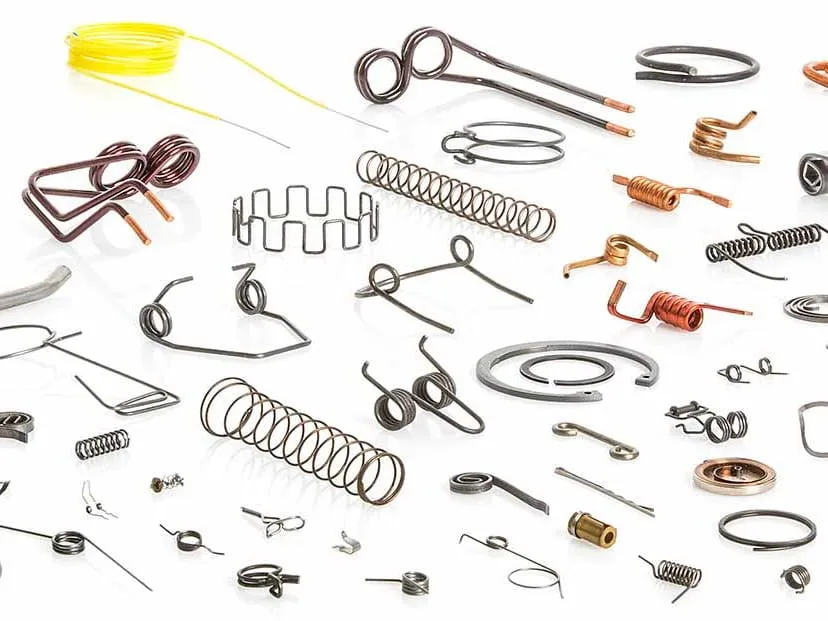
Bihler's speciality since its first spring-winding machine in 1953. Simultaneous forming gives very high speeds and forming from the inside out avoids twist; wire parts can also be coined, cut and welded.

Medical safety clips

Medical safety clips

A self-activating 0.1 mm spring-steel safety clip that encloses the used needle tip. 300 per minute in seven sizes; clean-room production, 15-minute tool change.

Electric motor housings

Electric motor housings

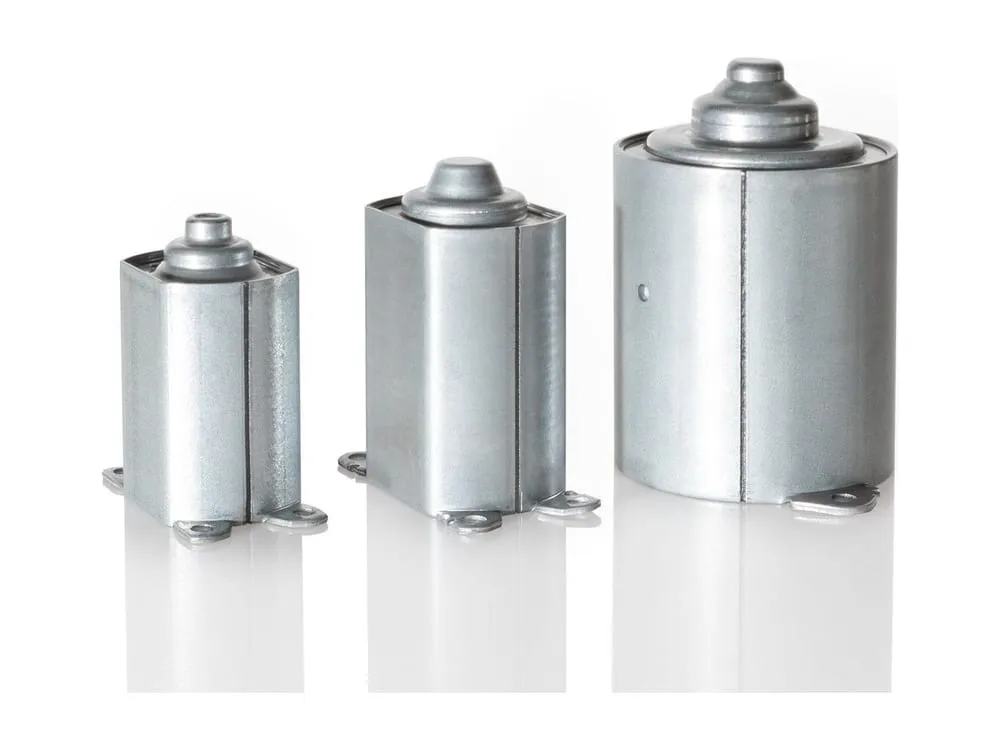
Made from strip instead of deep drawing: stamping, forming, laser welding and assembly in one system; less material and weight, no drawing oil. Double-walled housings raise motor performance.

Stator interconnection circuits (ZSB)

Stator interconnection circuits (ZSB)

Circuit elements that contact single-tooth stator coils at embossed humps: the interface between stator and inverter. 3–4 finished parts per minute.

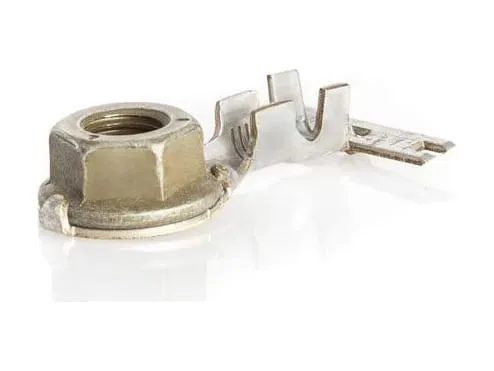
Battery grounding busbars

Battery grounding busbars

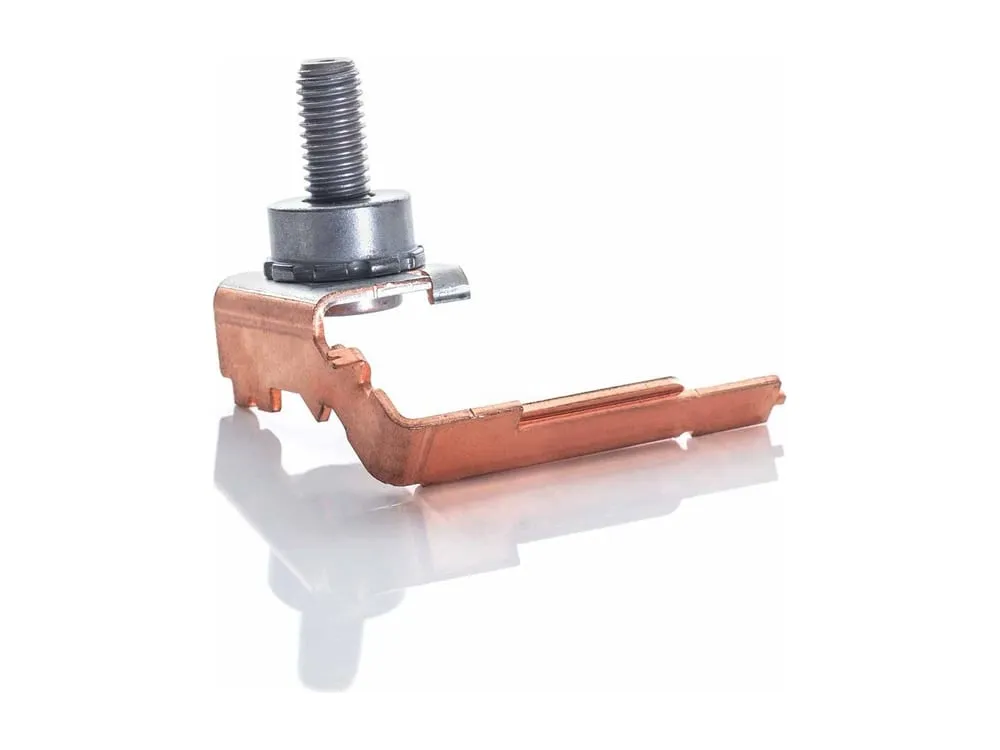
Connects the EV battery to the chassis for potential equalisation, spark and EMI protection. Stamping, bending, bolt and washer feeding and force-monitored press-fitting in one system; three variants, 60 per minute.

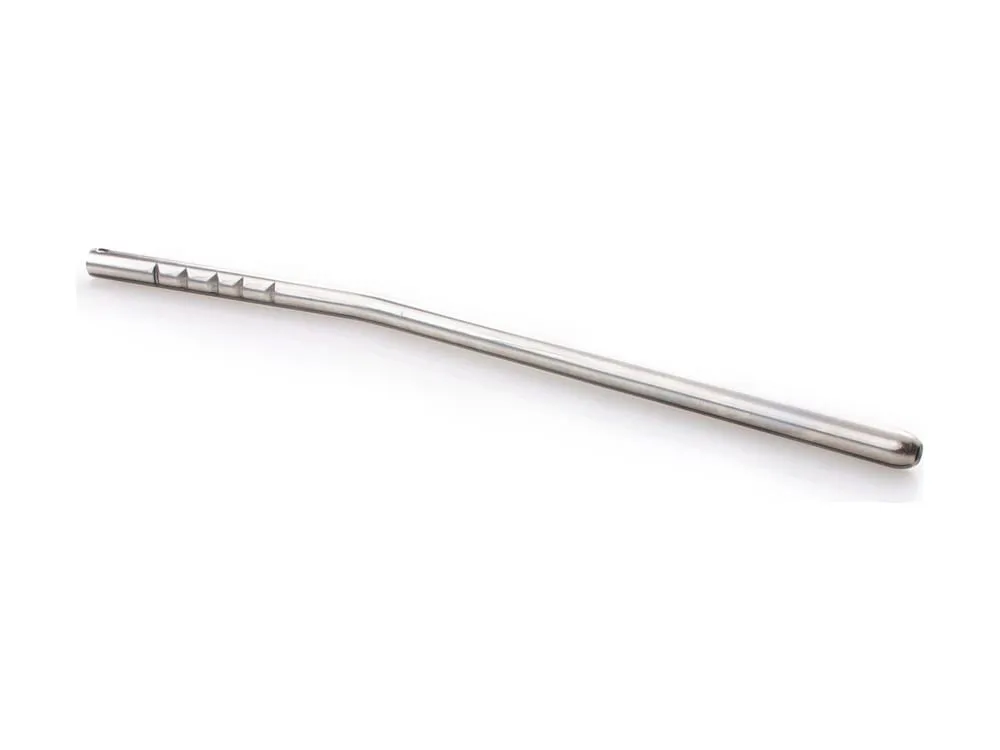
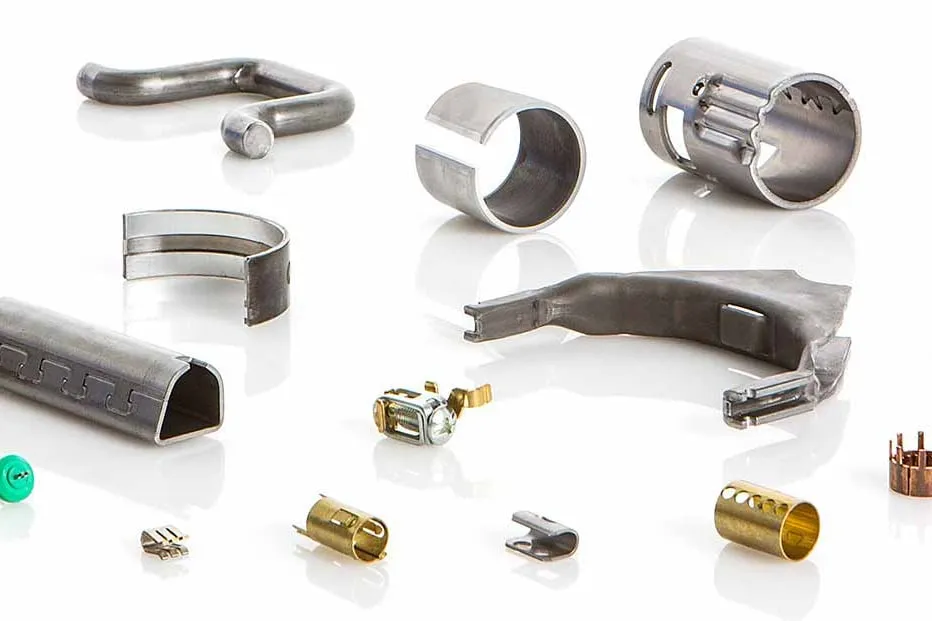
Head restraint tubes

Head restraint tubes

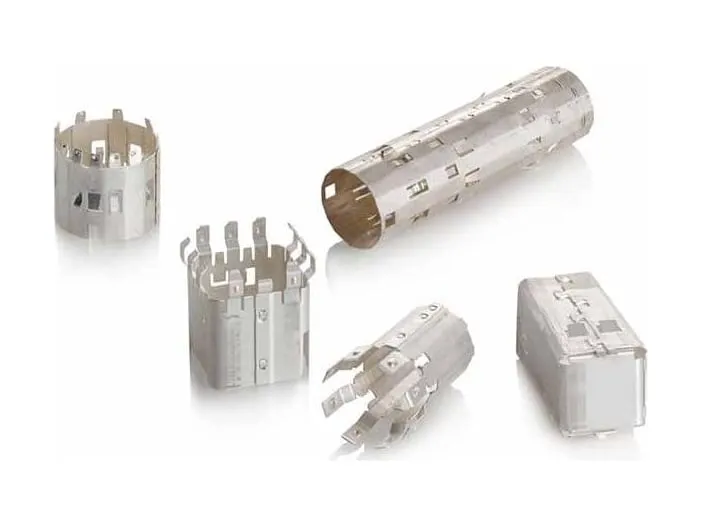
Length check, weld-seam detection, cutting, stamping, laser marking, radial riveting and bending in one system; 40 tubes per minute, 44 NC axes, variant change in 15–60 minutes.

Battery terminal clamps

Battery terminal clamps

Punching, bending, stamping, feeding and assembly in one processing centre; about 150 clamps per minute with minimal scrap.

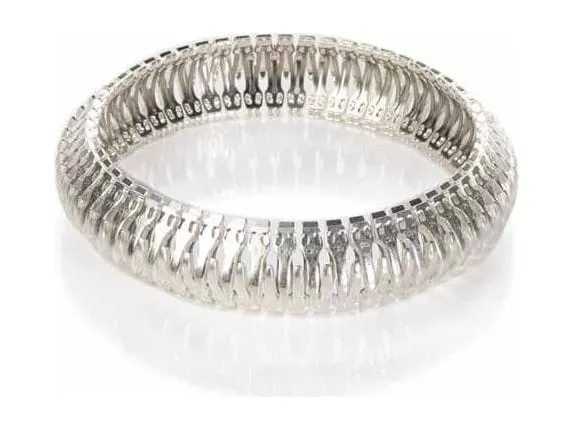
Ring-shaped high-current contact lamellae

Ring-shaped high-current contact lamellae

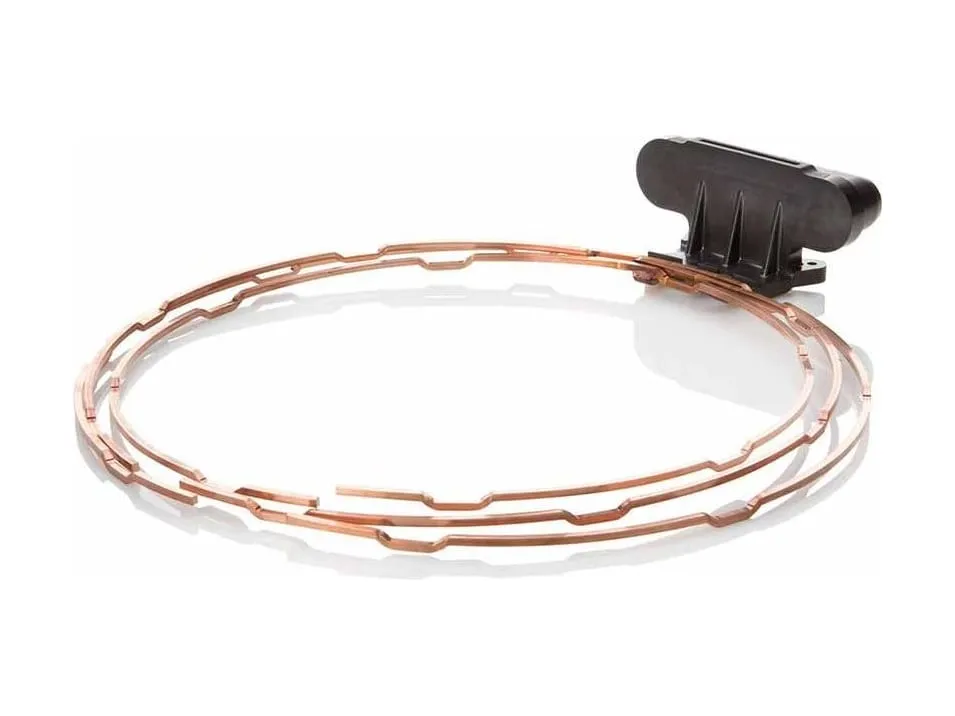
Contact lamellae riveted onto a stainless carrier strip, for transformers, switchgear and circuit breakers; 100 per minute.

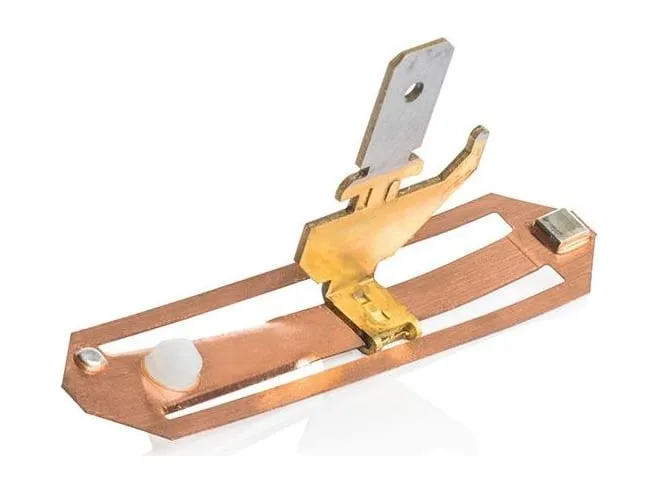
Kick-over spring contacts for pressure switches

Kick-over spring contacts for pressure switches

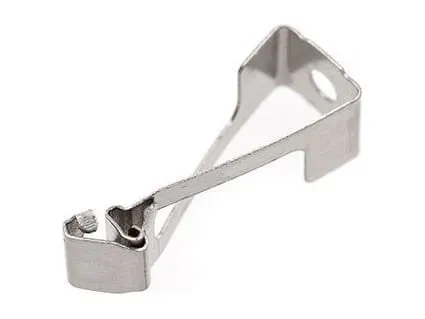
The kick-over spring contact of a washing-machine pressure switch: forming, five weld points, riveting and assembly; 100–120 per minute.

Child-seat anchor brackets

Child-seat anchor brackets

Safety brackets of Ø 6 mm wire for child-seat anchorage in cars; 80 per minute, switching between open and closed type by program.

Technologies

Bihler technologies

Strip or wire is processed by these steps one after another on the same machine; process modules are chosen per machine.

Bihler: Stamping

Stamping

Cutting in the press area: strip or wire in copper, non-ferrous metals, aluminium, precious metals, high-strength CrNi steels and bimetals. Up to 800 kN on servo press modules.

Bihler: Bending

Bending

In radial or linear tools; stroke, duration and speed of each station are set separately by cams or NC units. Precise, repeatable, long tool life.

Bihler: Tapping

Tapping

The servo GSE unit forms threads without chips in pre-punched holes, giving strong threads. Up to 260 threads per minute, M2–M20.

Bihler: Screw fastening

Screw fastening

The MSE unit feeds, separates, positions, inserts and torques screws; up to 140 complete operations per minute, up to M8. Drawn collars add thread turns in thin sheet.

Bihler: Welding

Welding

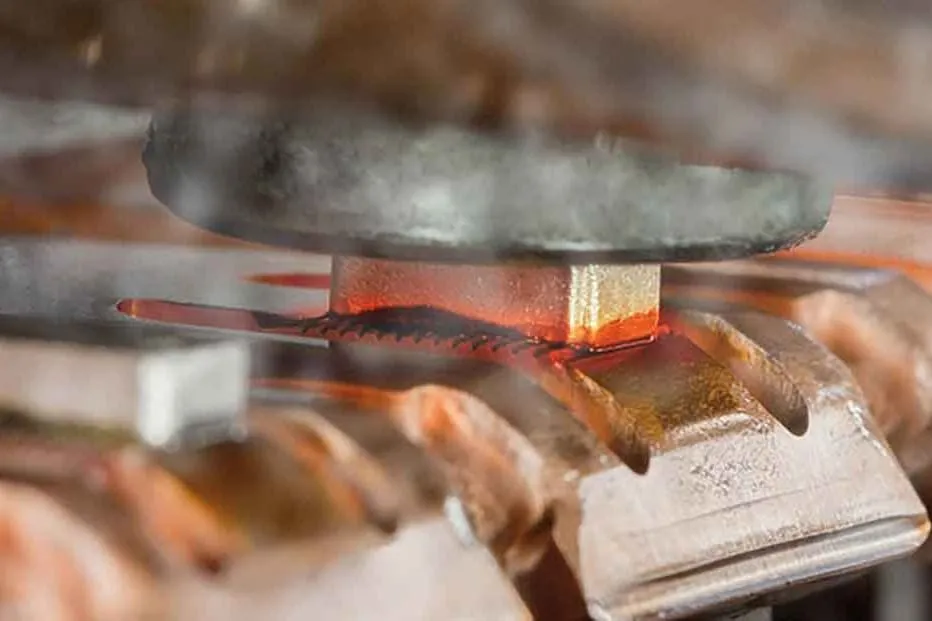
Resistance butt, mash-seam, projection, contact and precious-metal welding, strand compacting, nut welding and soldering; laser welding with TRUMPF technology. B 20K control.

Bihler: Assembly

Assembly

Many process steps in one machine: BIMERIC systems with pick & place and lift-rotate units turn out ready-to-install assemblies.

Bihler: Feeding

Feeding

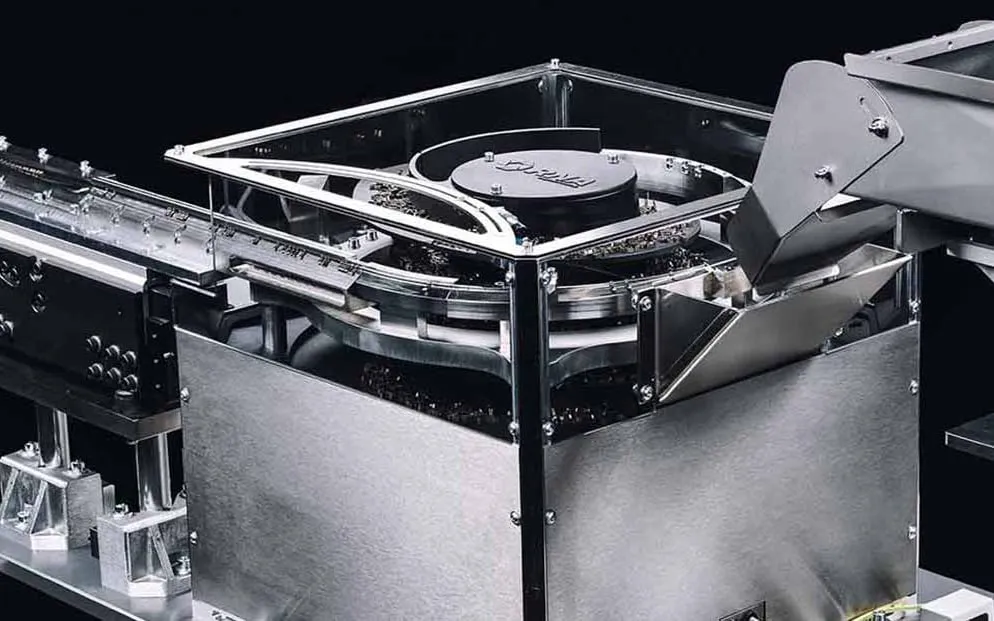
Feeding systems are elementary building blocks of subassembly production; Bihler has integrated them into its complete solutions for more than 50 years. Bowl feeders, linear conveyors, conveyor belts and bunkers are designed with RNA components.

Bihler: Stripping

Stripping

The servo ANC 5 unit strips enamel from round wire: Ø 0.5–5 mm, up to 12,000 rpm, 0.5–50 mm length. Cutting values are entered in the VC 1 control.

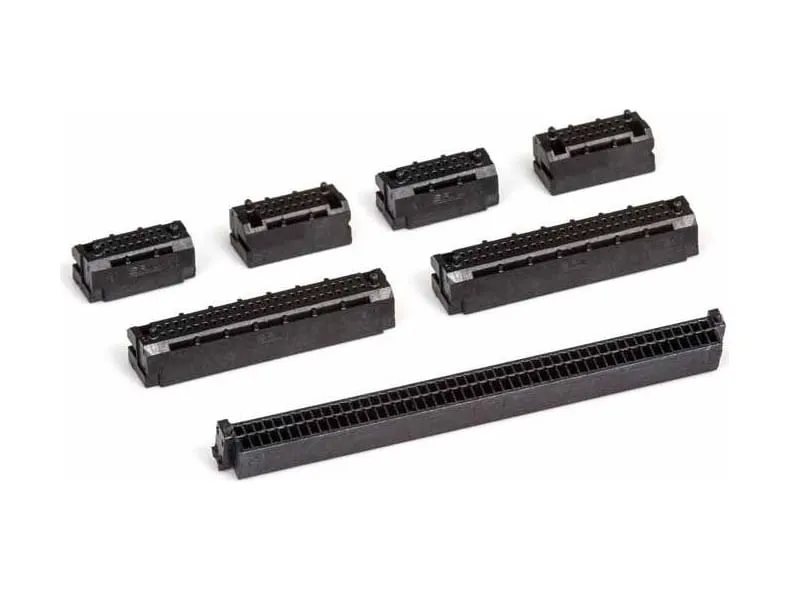
Bihler: Stitching

Stitching

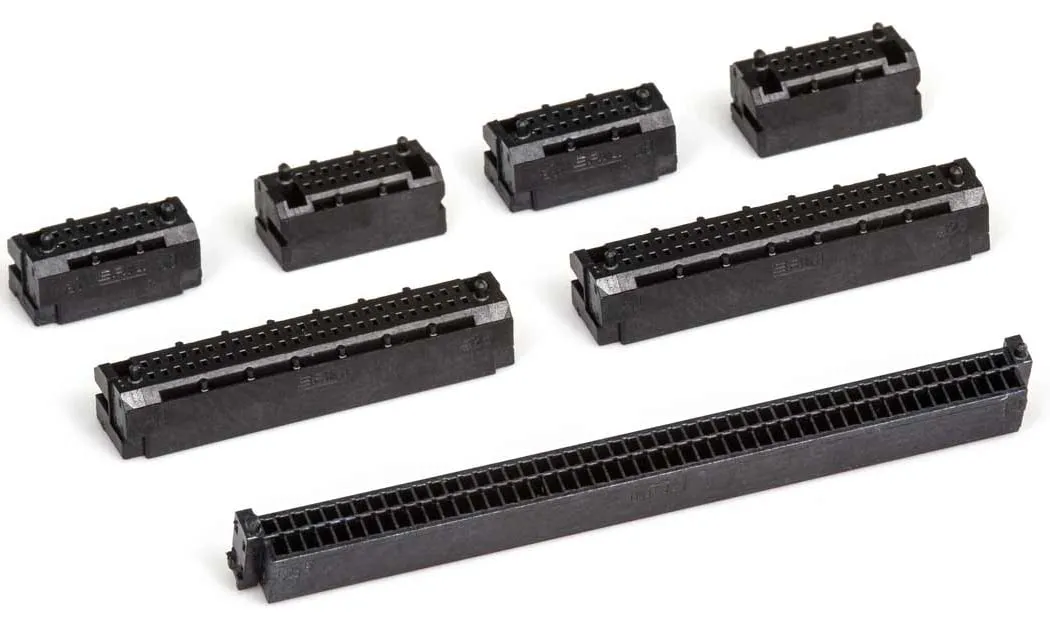
Developed by Bihler for plug connectors: up to 600 pins per minute are inserted into the housing, NC-assisted, horizontally and vertically. The insertion module is used on BIMERIC and BMK-NC.

Bihler: Clinching

Clinching

Joins sheet metal without filler material, by forming. At Bihler it is used primarily in round body production: the blank ends are punched and joined together like a puzzle.

Bihler: Spring winding

Spring winding

Where it all began for Bihler: since the first spring winding machine UFA 1 in 1953, thousands of manufacturing solutions for springs. Flat, shaped and leaf springs, spring clips and contact springs.

Bihler: Contact soldering

Contact soldering

Resistance soldering is used in particular for copper materials, for example switch contacts with a fusion surface larger than 4 mm²; it requires a solder additive, usually L-Ag15P.

Bihler: Calibrating

Calibrating

In bushing production the outer or inner diameter is calibrated for roundness in a radial press; its enclosed design transmits 100% of the force centrally to the component. Tool parts use a quick-change system.

Bihler: Measuring

Measuring

Measuring and production data acquisition integrated in the VC 1 control allow continuous process monitoring. Different measuring sensors monitor the production processes.

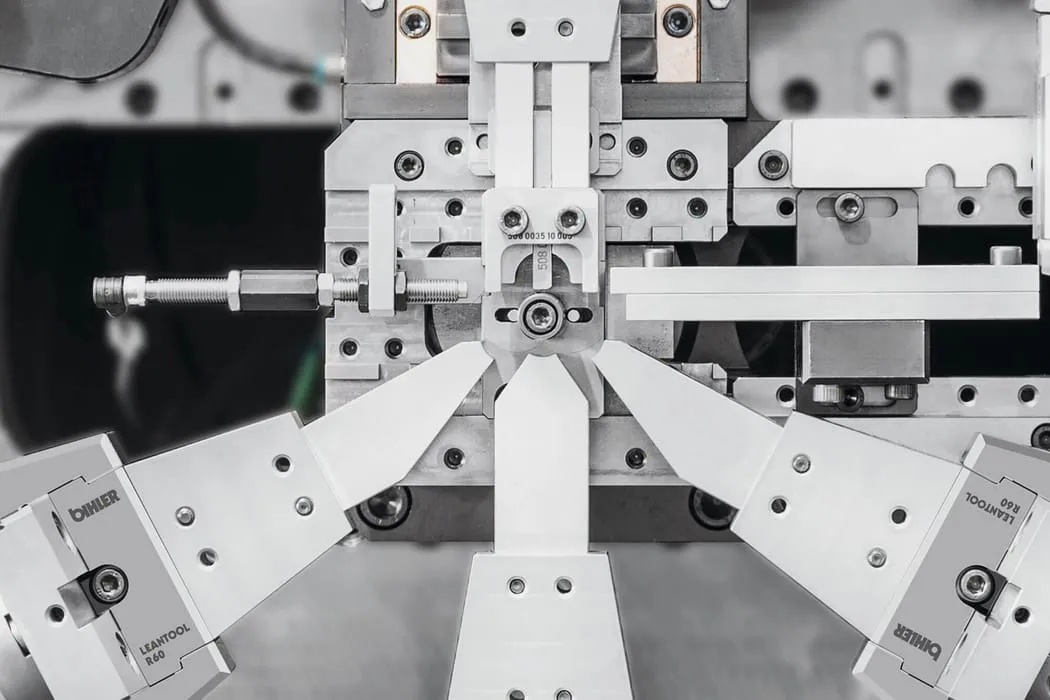
Bihler: LEANTOOL
Tooling system

LEANTOOL

Standardised radial and linear tooling: up to 70% standard tool parts; Meusburger die sets for NC presses up to 400 kN.

Other processes

Laser markingRivetingCrimpingDeburringDrawingCoiningRollingBroachingResistance annealingShearingCountersinkingHeadingWobblingPress fittingPalletizingBlister packaging

Machines

Bihler models and technical data

Each card leads to the model page: comparative technical data table, variants and a PDF data sheet.

Mechanical and hybrid production systemsFor mass production

Servo production systemsFor small, medium and large batches

Linear machinesCam-controlled and servo-controlled

Technical data is taken from information published by the manufacturer. The manufacturer may change it without notice, and values may vary with the model and the machine configuration. The data is for information only and is not binding on Boztaş; binding values are stated only in a written quotation.

News

Bihler news

Short summaries of the news and announcements the manufacturer publishes on its own website. Click a title; the full item opens on the manufacturer’s site.

News and trade fairs

News

Fourth Bihler Forum in Italy (opens in a new tab)

More than 90 people attended the forum in Arese. Talks covered adapting 125 existing tools to a GRM-NC, the BC R retrofit package, a solution with integrated laser welding and bNX training.

News

Bihler Forums in the UK, Sweden and Spain (opens in a new tab)

More than 80 people took part in the three forums. Topics: standardisation, modularisation, material efficiency, sustainability, digital services, resistance welding, and machine and control modernisation.

News

First Bihler Coating Day in Halblech (opens in a new tab)

More than 50 people from 22 companies in Germany and Austria attended the first coating day on 30 April. Bihler presented its new PVD coating system for tool parts and four coatings.

News

Stamping and forming forum in Dortmund (opens in a new tab)

120 people attended the forum on 16 October. Highlights were a new LM 2000-KT, four knowledge stations including a GRM 50 modernisation, and talks on resistance welding and next-generation tools.

Application stories from the customer magazine

Customer magazine

Box terminals for boards on the LM 2000-KT (opens in a new tab)

Box terminals for boards have been produced on an LM 2000-KT since July 2024, with a target of 400 strokes per minute. Switching to the second variant of the part needs only one disk cam to be changed.

Customer magazine

Intelligent stripping of hairpins (opens in a new tab)

A new sensor unit continuously measures the enamel thickness and the total wire thickness; the mechanical stripping station on the BM-HP system strips each hairpin accordingly. Typical total cross-sectional loss is less than 0.05 mm.

Software, training and resources

The summaries are compiled from texts published by the manufacturer; dates, venues and content may change. The text on the manufacturer’s website prevails.

Ask about Bihler

Describe your workpiece, material and annual quantity; we will get back to you.

Catalogue

We will e-mail you the catalogue

Enter your details and we will send the download link to your e-mail address straight away.

Your details are used only to send this catalogue and to contact you about your request. KVKK Notice