Since 198343 years serving Turkish industry

Servo multi-slide

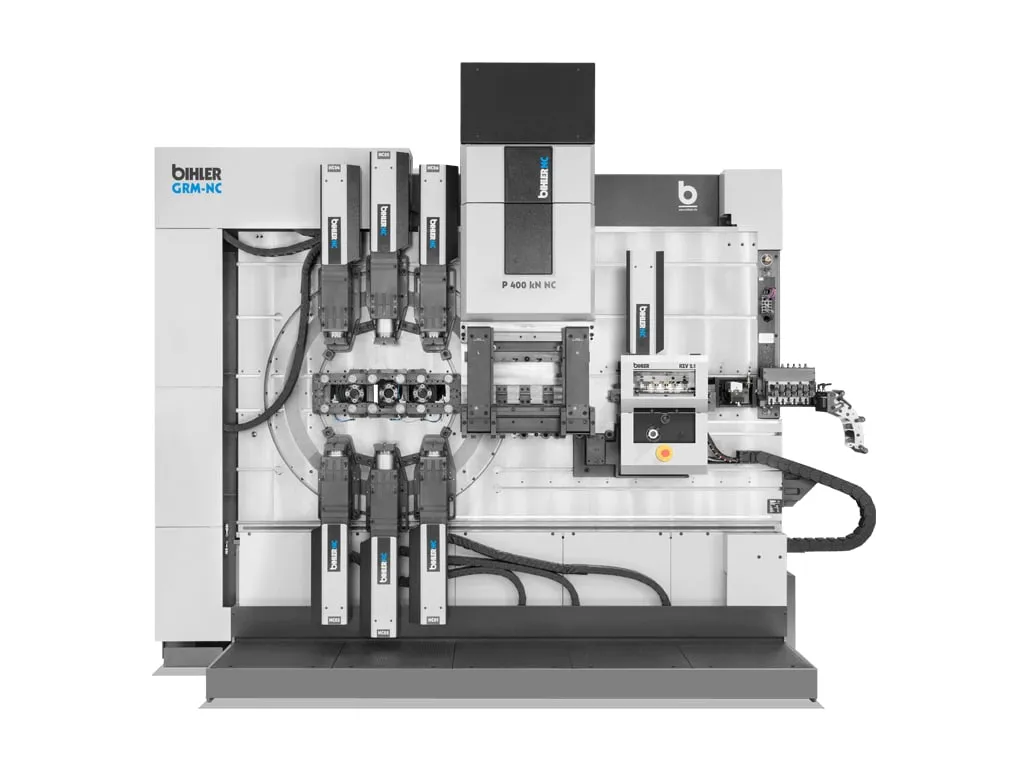
Bihler GRM-NC

Universal servo multi-slide machine for small and medium batches

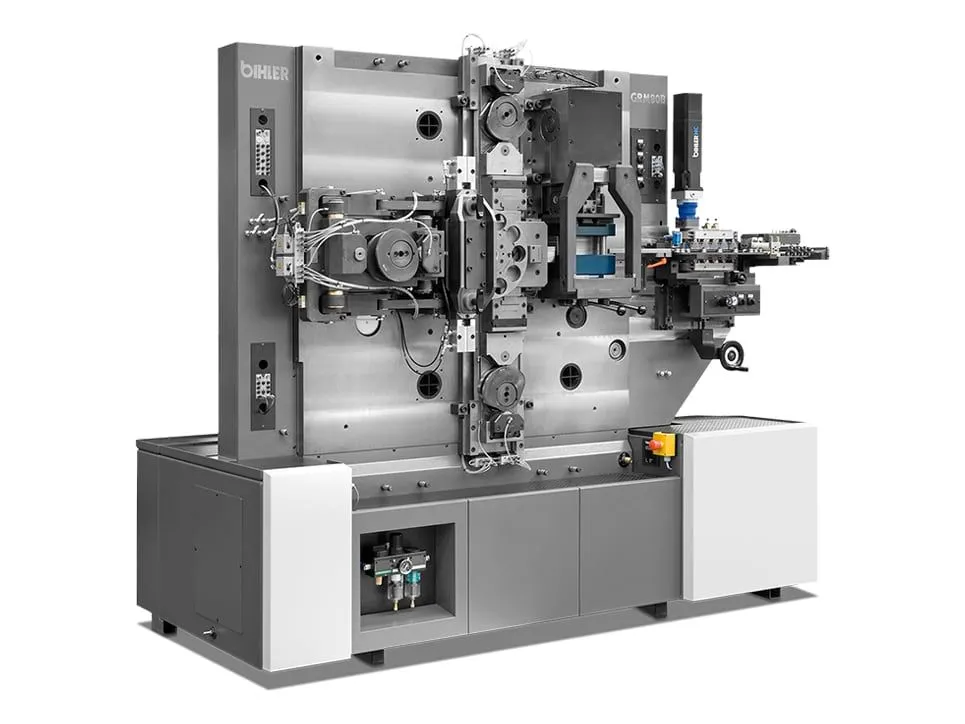
Bihler GRM-NC servo multi-slide machine, linear configuration
250 1/min Stroke rate
400 kN Press force
90 mm Strip width
Ø 6 mm Wire diameter (approx.)
> 2,000 mm Linear process length

ⓘ Manufacturer data (Bihler product pages; RM-NC / GRM-NC brochure 10/21). Values may change and vary; not binding on Boztaş.

Why GRM-NC?

GRM tool compatibility

Full tool compatibility with the mechanical GRM series; existing tools are adapted and optimised. The manufacturer reports an average 160 % output increase and 80 % set-up time reduction across 175 tools adapted to the RM-NC and GRM-NC.
Radial and linear LEANTOOL

Standard platform for LEANTOOL Radial R100 and Linear L250; interfaces in the forming area are 100 % compatible with L250 linear tools (Modular Series); process lengths of more than 2,000 mm in linear production with three bending modules and two servo presses.

Programmable servo axes

Working stroke, position and motion profile of the NC units are freely programmable; the adjustment and positioning unit reproduces all unit positions 100 % at the push of a button; up to 3 central mandrels, set up from the front.

Variants

GRM-NC radial

LEANTOOL Radial R100 or adapted GRM radial tools; in radial production the strip width equals the part width (for busbars, up to 50 % material savings according to the manufacturer)

Suited to: Busbars, contacts, clips

GRM-NC linear

LEANTOOL Linear L250; more than 2,000 mm process length with 3 bending modules + 2 servo presses; linear tools shared with the LM 2000-KT, LM 2000-NC and BIMERIC Modular

Suited to: Long parts, large busbars, multi-variant linear production

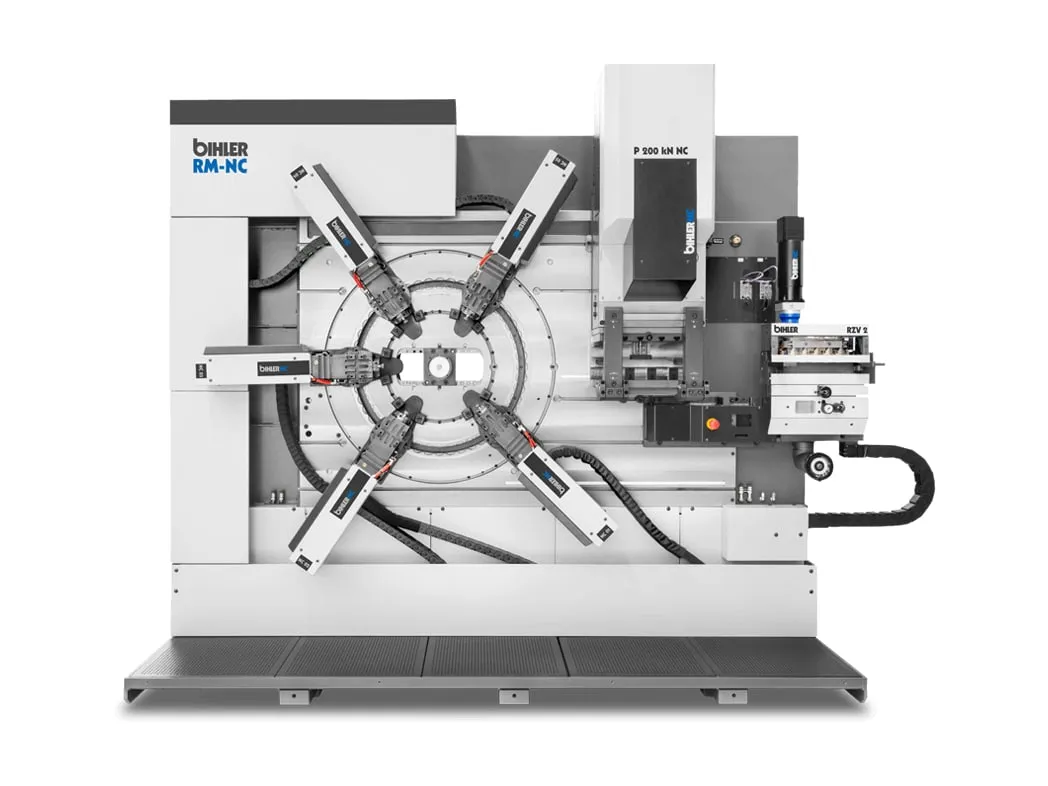
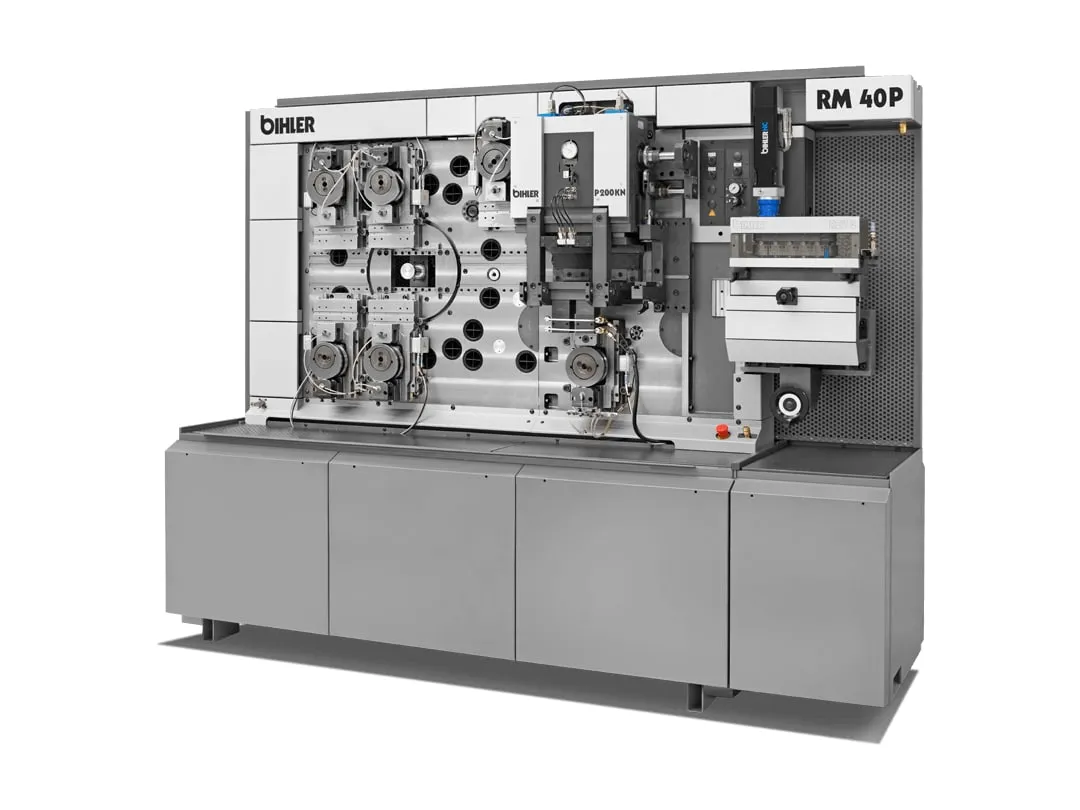
RM-NCsmaller sibling

200 kN servo eccentric press, 300 1/min, 20 kN units, 4 × 80 mm strip, Ø 4 mm wire; RM series and FINZER tool compatibility, LEANTOOL Radial R60

Suited to: Smaller radial parts

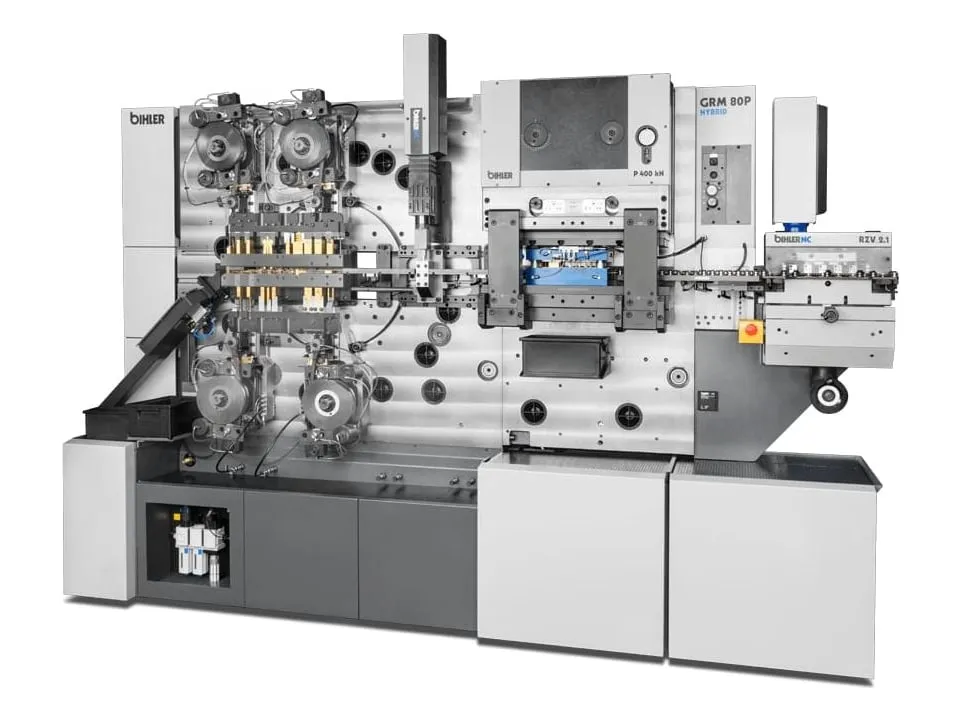
Mechanical GRM 80tool source

Cam-controlled GRM 80E / 80P: 250 1/min, 300–400 kN eccentric press; its tools can be adapted to the GRM-NC

Suited to: High-volume jobs with established tooling

Technical data

Columns to compare
FeatureGRM-NCRM-NC
Performance
Stroke rate stepless, max. 250 1/min (depending on tool concept and forces)stepless, max. 300 1/min (depending on tool concept and forces)
Press Servo spindle press 400 kN; freely programmable working stroke, max. 60 mm (standard 16 mm), no fixed BDC; optional 300 kN servo eccentric pressServo two-point eccentric press 200 kN; fixed stroke 12 mm with BDC
NC units (servo axes) 31–47 kN (standard 31 kN), stroke max. 100 mm; 6 axes standard, max. 12max. 20 kN, stroke max. 120 mm; 6 axes standard, max. 14 (more than 12 with an additional axis cabinet)
Tool area and feed
Central mandrel max. 3, 31–47 kN, stroke max. 100 mm; set-up from the frontmax. 3, 20 kN, stroke max. 120 mm; set-up from the front
Tooling system LEANTOOL Radial R100 and Linear L250; adapted mechanical GRM tools; press plate for Meusburger SBP / SBH 400 die setsLEANTOOL Radial R60; adapted mechanical RM and FINZER (ZUBHS 100/200, ZUB 200/220/250) tools
Linear process length > 2,000 mm (3 bending modules, 2 servo presses)—
Feed RZV 2.1 servo radial gripper feed, any length; up to 3.2 m/s, repeatability ±0.02 mmRZV 2.1 servo radial gripper feed, any length
Material
Strip thickness / width max. 4 mm / 90 mmmax. 4 mm / 80 mm
Wire diameter approx. Ø 6 mmmax. Ø 4 mm
Control
Control VariControl VC 1; control cabinet in the machine housing; recording of measurement and production data (OPC UA)VariControl VC 1; control cabinet in the machine housing; recording of measurement and production data (OPC UA)
Monitoring Press force and bearing temperature monitoring; absolute measuring system and software overload protection on the NC unitsPress force and bearing temperature monitoring; absolute measuring system and software overload protection on the NC units
Dimensions and weight
Dimensions (W×D×H, without sound enclosure) 3,282 × 1,820 × 3,055 mm (with press; height without press 2,740 mm)3,050 × 1,820 × 2,600 mm (with press; height without press 2,540 mm)
Weight (without tools) approx. 9,500 kgapprox. 6,000 kg

Manufacturer data (Bihler product pages; RM-NC / GRM-NC brochure 10/21). The brochure gives 240 1/min for the GRM-NC, the current product page 250 1/min; depends on material and process.

Processes that can be combined on this machine

  • Stamping
  • Bending
  • Contact welding (Quickchange D1Q–D3Q)

Typical workpieces

  • Copper, tinned-copper and aluminium busbars up to 4 mm (Stromschienen)
  • Shielding sleeves for charging plugs (Schirmhülsen für Ladestecker)
  • EV charging connectors (Ladesteckverbinder für Elektrofahrzeuge)
  • Contact parts for electrical connectors (Kontaktteile für Steckverbinder)
  • Double-walled electric motor housings (doppelwandige Elektromotorgehäuse)
  • Springs for automotive brake systems (Federn für Kfz-Bremssysteme)
  • Technical springs (Technische Federn)
  • Fixing clips for the aviation industry (Befestigungsclips für die Luftfahrtindustrie)
  • Flat roof tile clips (Clips zur Halterung von Flachdachziegeln)

Related industries: AutomotiveAerospaceElectricalElectronics and Connectors

Frequently asked questions

What is the difference between the GRM-NC and the RM-NC?

The GRM-NC is for larger parts: 400 kN servo spindle press (programmable stroke up to 60 mm), 31–47 kN NC units, 4 × 90 mm strip and approx. Ø 6 mm wire, and process lengths of more than 2,000 mm in linear production. The RM-NC reaches 300 1/min with a 200 kN servo eccentric press, 20 kN units, 4 × 80 mm strip and Ø 4 mm wire, and is the platform for LEANTOOL Radial R60.

Will my mechanical GRM 80 tools run on the GRM-NC?

Yes; the GRM-NC is fully compatible with mechanical GRM series tools, and existing tools are adapted and optimised. The manufacturer reports an average 160 % output increase and 80 % set-up time reduction across 175 tools adapted to the RM-NC and GRM-NC.
Which tooling technologies does the GRM-NC work with?

Adapted mechanical GRM tools (radial and linear), LEANTOOL Radial R100 and LEANTOOL Linear L250. L250 linear tools can be moved to the other Modular Series machines (LM 2000-KT, LM 2000-NC, BIMERIC Modular).

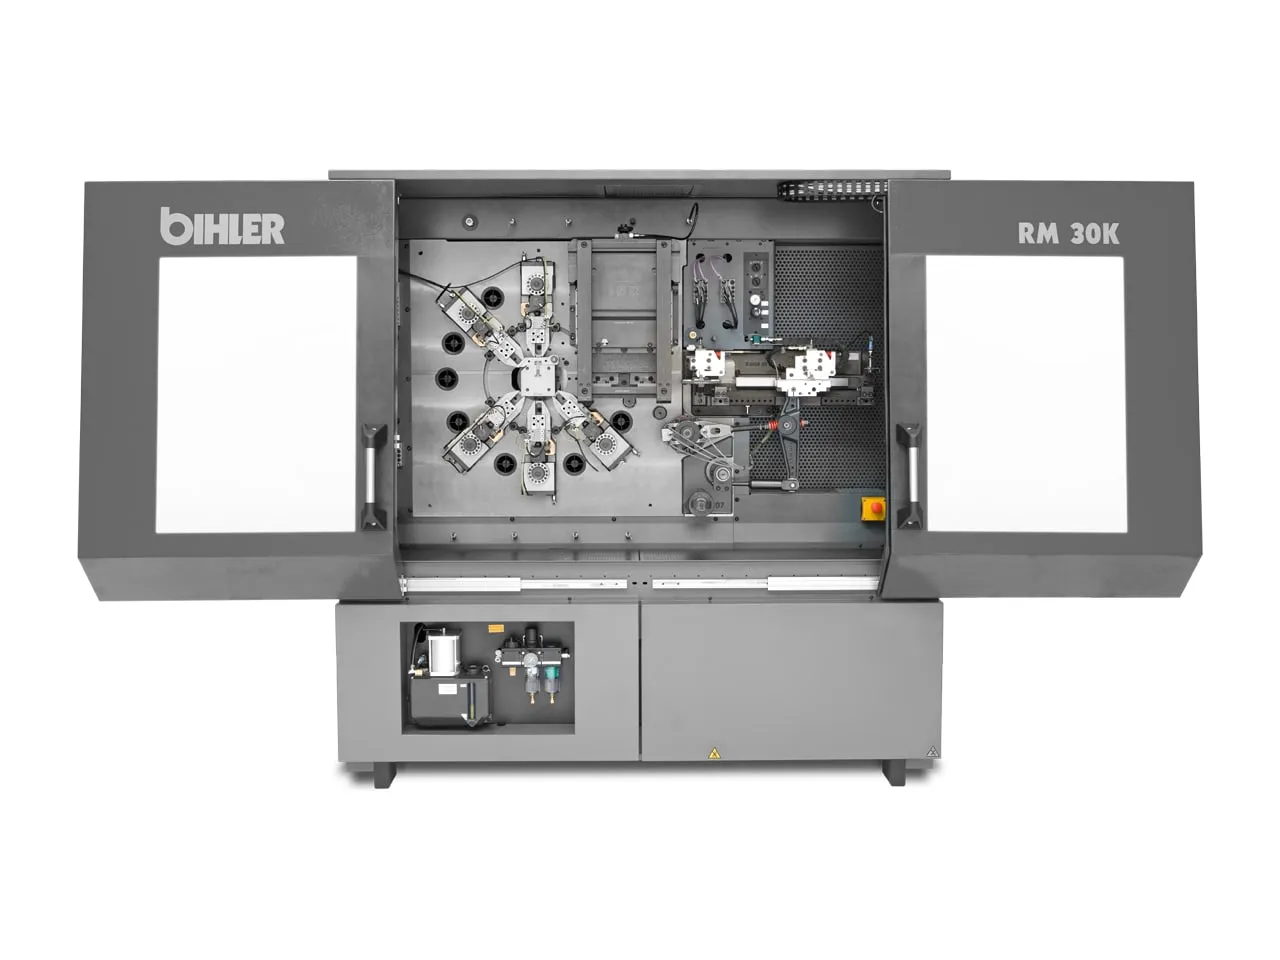
Other Bihler models

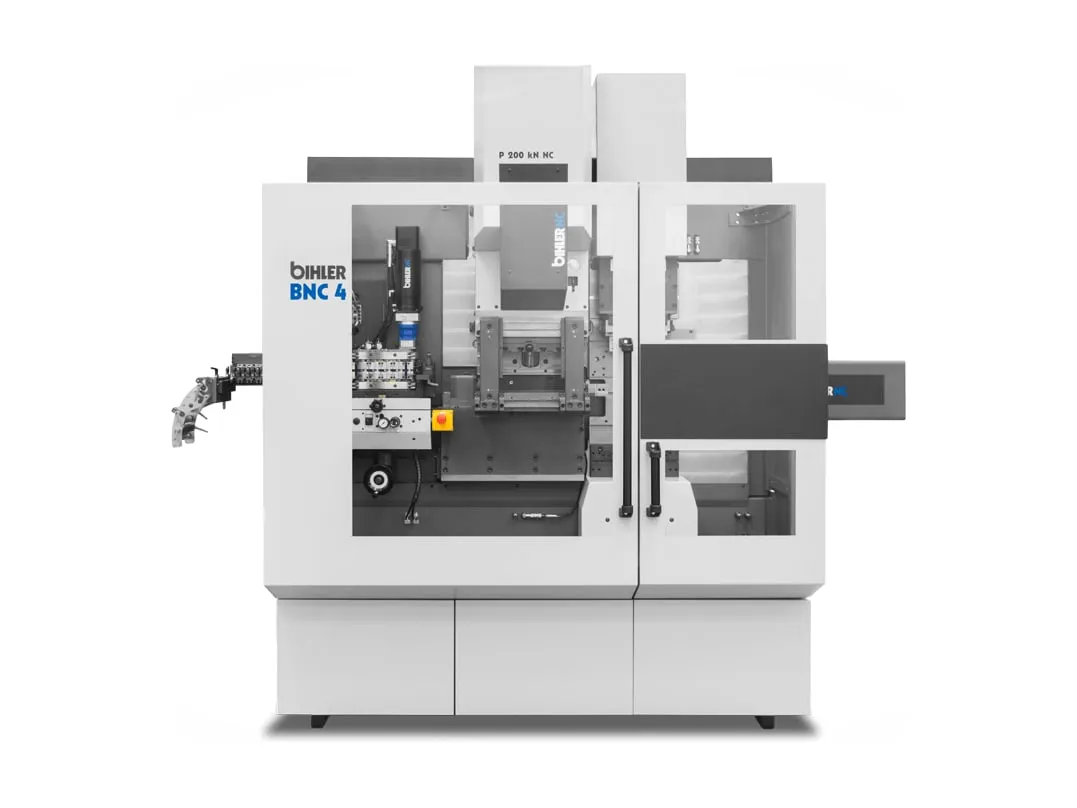
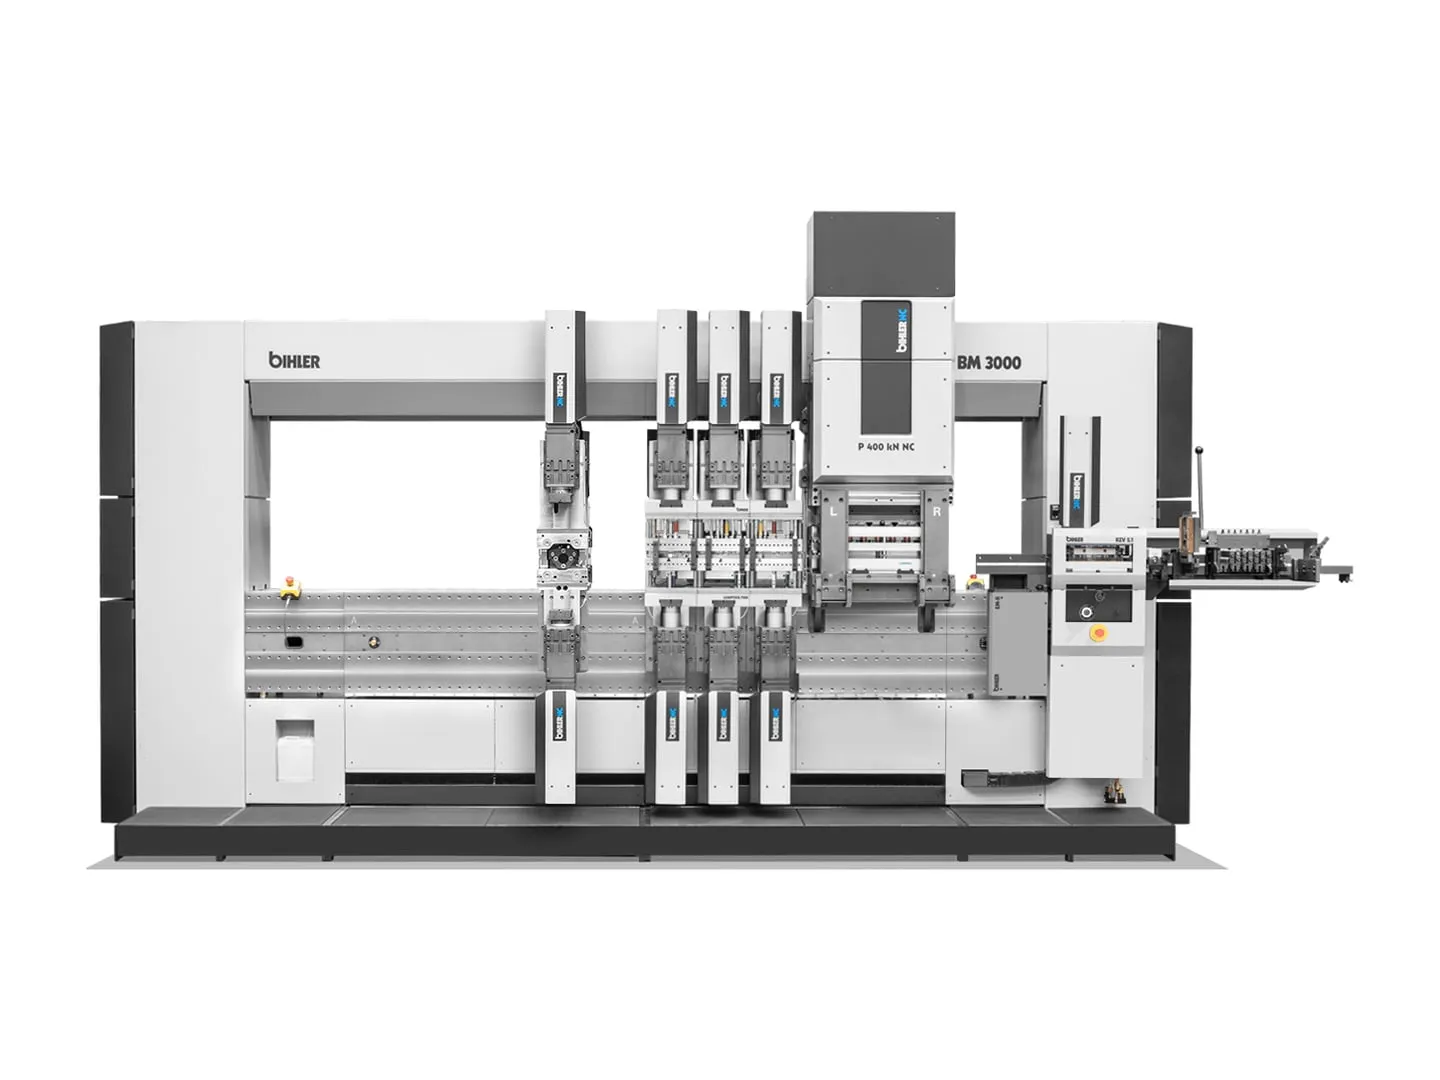
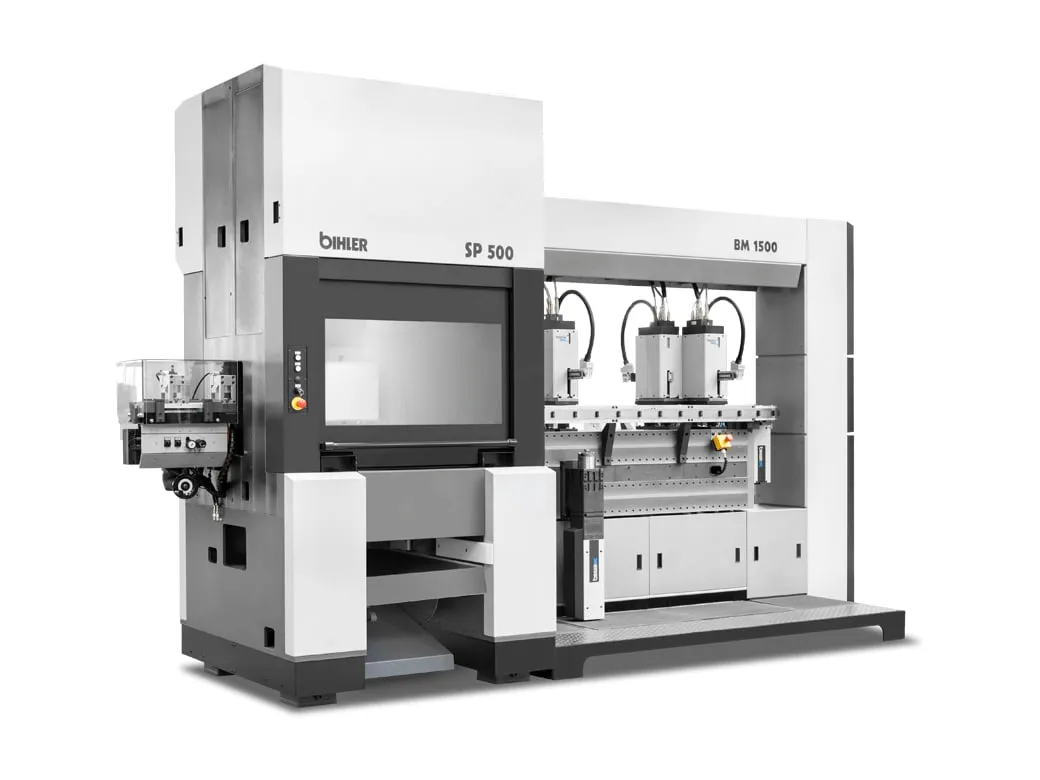
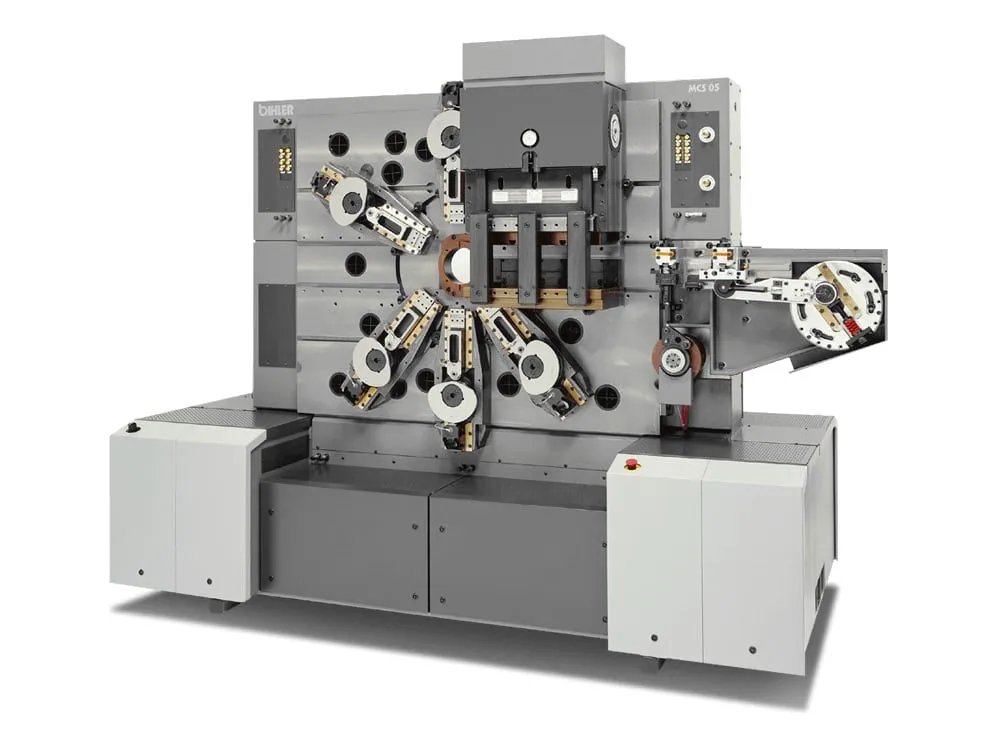
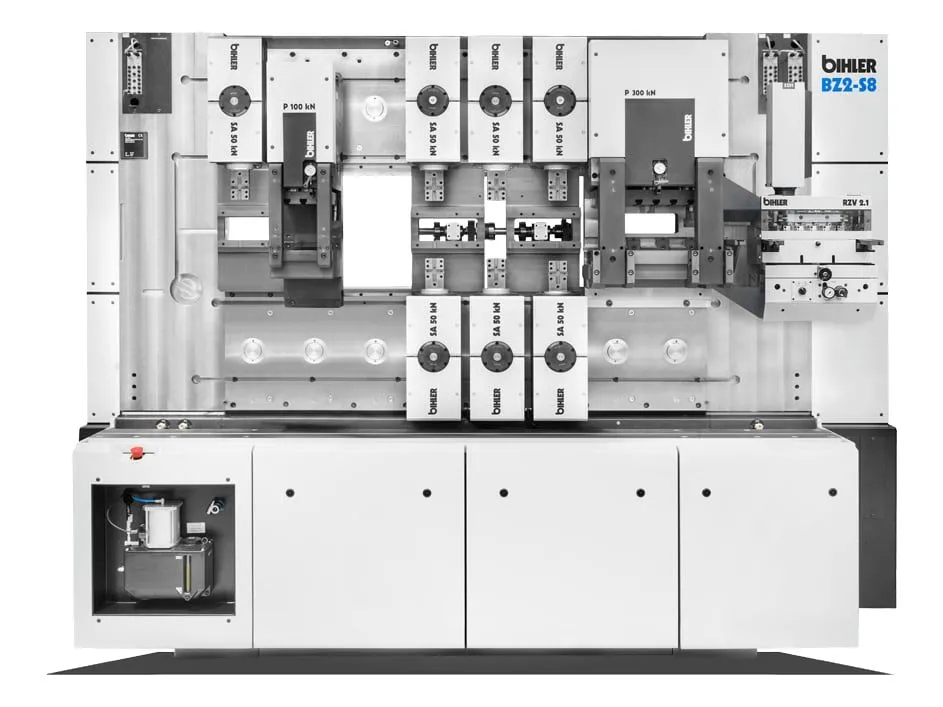
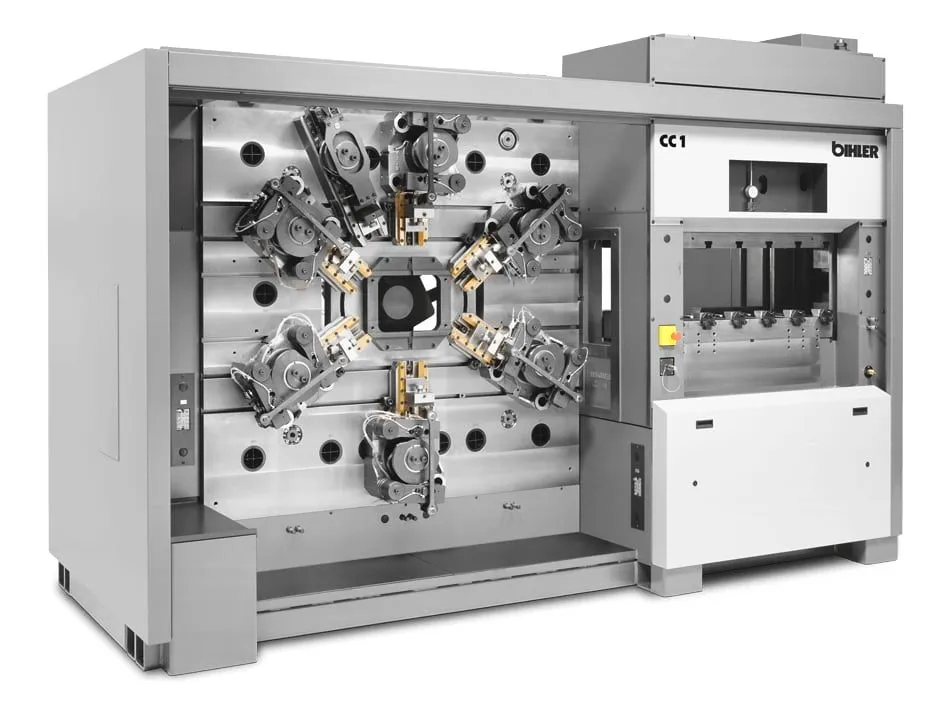
Bihler GRM 80 Bihler GRM 80 Universal multi-slide machine for large stamped and bent parts 250 1/min300–400 kN80 mm Technical data Bihler RM 40 Bihler RM 40 Compact multi-slide machines for mass production of small precision stamped and formed parts 350 1/min90–200 kN60 mm Technical data Bihler RM 30K Bihler RM 30K Compact multi-slide machine for mass production of small stamped and formed metal parts 350 1/min90 kN900 mm Technical data Bihler RM-NC Bihler RM-NC Servo multi-slide machine for small and medium batches with radial tooling 300 1/min200 kN80 mm Technical data Bihler BNC 4 Bihler BNC 4 Servo multi-slide production system compatible with MRP tooling 300 1/min200 kN31 kN Technical data Bihler BIMERIC BM Bihler BIMERIC BM Modular servo production and assembly system from raw material to ready-to-install assemblies 250 1/min400 kN80 mm Technical data Bihler BIMERIC SP Bihler BIMERIC SP Sub-assembly production system combining a servo press with the BIMERIC platform for progressive dies 250 1/min500 kN15–63 mm Technical data Bihler BM-HP 3000 Bihler BM-HP 3000 Servo system producing complete electric-motor hairpins from flat wire on the coil 60–120/min3.2 m/s±0.02 mm Technical data Bihler LM 2000-KT / LM 2000-NC Bihler LM 2000-KT / LM 2000-NC Modular linear machine platform with cam-controlled (KT) or servo-controlled (NC) units 500 1/min250 1/min2,000 mm Technical data Bihler SP 800 Bihler SP 800 800 kN servo press for progressive tools; stand-alone or combined with the BIMERIC 800 kN200 1/min30 mm Technical data Bihler RM S Bihler RM S High-speed multi-slide machine for stamped and formed parts made from high-tensile steels 600 1/min150 kN900 mm Technical data Bihler GRM 80B Bihler GRM 80B Bushing machine with a standardised tooling concept for mass production of straight and flanged bushings 220 1/min160 1/min15–40 mm Technical data Bihler MC 42 Bihler MC 42 Multi-slide machine with two processing faces for small stamped and formed parts and sub-assemblies 350 1/min90 kN60 kN Technical data Bihler MC 82 Bihler MC 82 Multi-slide machine with two processing faces for larger stamped and formed parts and sub-assemblies 250 1/min300 kN90 kN Technical data Bihler MC 120 Bihler MC 120 Multi-slide machine with a 700 kN press and two processing faces for large stamped and formed parts and sub-assemblies 150 1/min700 kN160 kN Technical data Bihler MCS 1 Bihler MCS 1 High-speed multi-slide machine with two processing faces, running at up to 800 strokes per minute 800 1/min70 kN30 kN Technical data Bihler MCS 05 Bihler MCS 05 High-speed multi-slide machine with two processing faces for large stamped and formed parts and sub-assemblies 500 1/min300 kN50 kN Technical data Bihler BZ2-S8 Bihler BZ2-S8 High-performance processing centre driven by servo motors for mass production of stamped and formed parts and sub-assemblies 700 1/min300 kN50 kN Technical data Bihler CC 1 Bihler CC 1 COMBITEC processing centre with a separate 800 kN press module for long, bulky stamped and formed parts and sub-assemblies 200 1/min800 kN160 kN Technical data

Catalogue

We will e-mail you the catalogue

Enter your details and we will send the download link to your e-mail address straight away.

Your details are used only to send this catalogue and to contact you about your request. KVKK Notice