MRP tool compatibility
Existing tool applications from MRP (Meyer, Roth & Pastor) UB2, UB2B, UB3, UB3B, UB4 and UB4B machines are adapted and optimised for the BNC 4; UB2/3/4 cutting die sets are mounted using adapter sets.
Since 198343 years serving Turkish industry
Servo multi-slide
Servo multi-slide production system compatible with MRP tooling
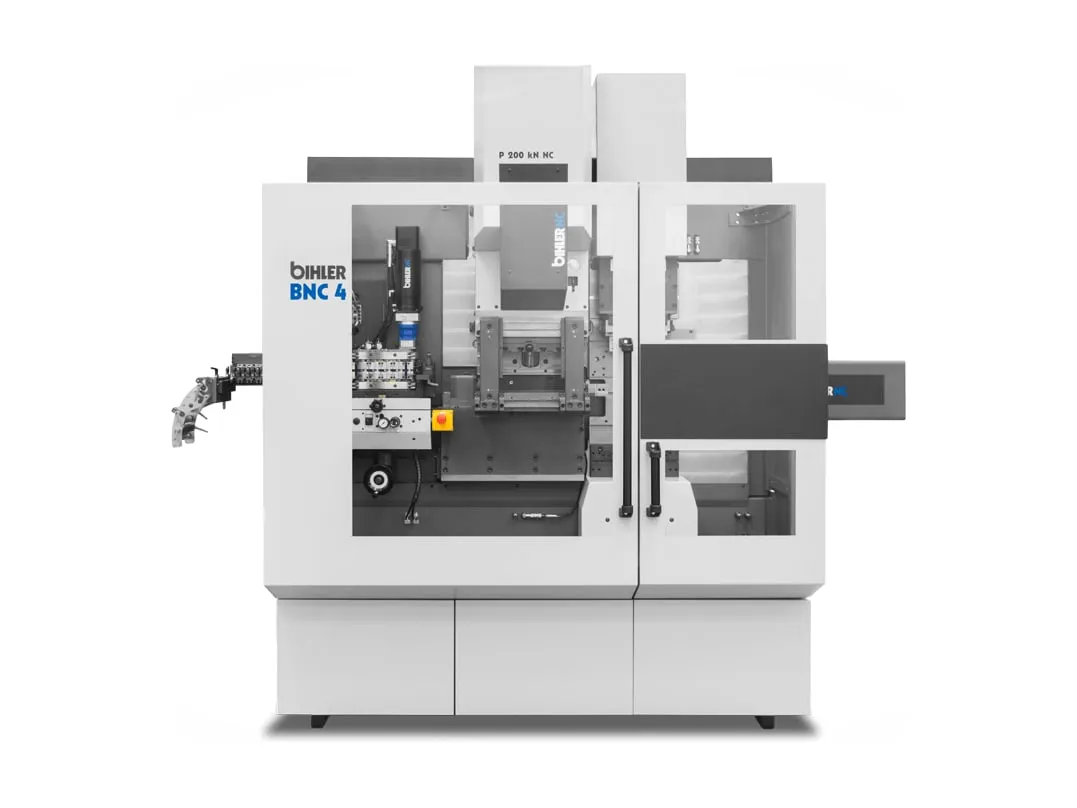
ⓘ Manufacturer data (Bihler BNC 4 product page, BNC 4 brochure 07/23); the brochure gives stroke values separately for UB3/UB3B and UB4/UB4B tool layouts. Values may change and vary; not binding on Boztaş.
Existing tool applications from MRP (Meyer, Roth & Pastor) UB2, UB2B, UB3, UB3B, UB4 and UB4B machines are adapted and optimised for the BNC 4; UB2/3/4 cutting die sets are mounted using adapter sets.
Working stroke, position and motion profile are freely programmable over the entire operating range; the NCA units carry adapted mounting plates and a quick-change system for UB2/3/4 tools.
Integrated cooling and central lubrication on all units, software overload protection and absolute measuring system; process-related thermal effects are compensated.
200 kN NC eccentric press (table 440 mm), triple NC slide unit on top, horizontal NC units from left and right, rear and front NC central mandrels, NC hold-down; RZV 2.1 servo feed
Suited to: Operations producing with MRP UB2–UB4 tools
Mounted on a pivoting holder; swung aside into a parking position when not needed and for tool assembly and maintenance
Suited to: Tools requiring a bending movement from the front
Servo platform for Bihler RM series and FINZER tools; 200 kN servo press, 4 × 80 mm strip, LEANTOOL Radial R60
Suited to: Existing tools are Bihler RM or FINZER
| Feature | UB3 / UB3B tool layout | UB4 / UB4B tool layout |
|---|---|---|
| Performance | ||
| Stroke rate | stepless 1–300 1/min (depending on motion profiles, forces and tool paths) | stepless 1–300 1/min (depending on motion profiles, forces and tool paths) |
| NC two-point eccentric press | max. 200 kN, stroke max. 12 mm, table length 440 mm | max. 200 kN, stroke max. 12 mm, table length 440 mm |
| Upper triple NC slide unit | left / right axis 19 kN, stroke 80 mm; centre axis 31 kN, stroke 77 mm | left / right axis 19 kN, stroke 80 mm; centre axis 31 kN, stroke 77 mm |
| Lower NCA4 slide unit (triple layout possible) | 19 kN per axis, stroke 100 mm | 19 kN per axis, stroke 100 mm |
| Horizontal NC units | from left NCA4 19 kN, stroke 70 mm; from right NCA4 19 kN, stroke 100 mm | from left NCA4 19 kN, stroke 64 mm; from right NCA4 19 kN, stroke 100 mm |
| Tool area and feed | ||
| NC central mandrel (rear) | Carriage NCA4 12 kN, stroke 79 mm; lever NCA3 3.5 kN, stroke 100 mm | Carriage NCA4 12 kN, stroke 70.5 mm; lever NCA3 3.5 kN, stroke 156 mm |
| NC central mandrel (front) | NCA4 19 kN, stroke 120 mm; optional on pivoting holder | NCA4 19 kN, stroke 120 mm; optional on pivoting holder |
| NC hold-down device | NCA3, clamping force max. 8.9 kN, stroke max. 25 mm | NCA3, clamping force max. 8.9 kN, stroke max. 33 mm |
| Feed | RZV 2.1 servo; strip and wire without retooling mechanical parts; any length | RZV 2.1 servo; strip and wire without retooling mechanical parts; any length |
| Material | ||
| Strip thickness / width | max. 4 mm / 40 mm | max. 4 mm / 40 mm |
| Wire diameter | max. Ø 4 mm | max. Ø 4 mm |
| Control | ||
| Control | VariControl VC 1, swivelling touch-screen terminal; function chart optimisation; remote maintenance optional | VariControl VC 1, swivelling touch-screen terminal; function chart optimisation; remote maintenance optional |
| Dimensions and weight | ||
| Dimensions (W×D×H) | 2,600 × 1,900 × 2,650 mm | 2,600 × 1,900 × 2,650 mm |
| Weight (without tools) | approx. 4,500 kg | approx. 4,500 kg |
Manufacturer data (Bihler BNC 4 product page, BNC 4 brochure 07/23); the brochure gives stroke values separately for UB3/UB3B and UB4/UB4B tool layouts. Forces are short-term peak values; depends on material and process.
Technical data is taken from information published by the manufacturer. The manufacturer may change it without notice, and values may vary with the model and the machine configuration. The data is for information only and is not binding on Boztaş; binding values are stated only in a written quotation.
Existing tool applications from MRP UB2, UB2B, UB3, UB3B, UB4 and UB4B machines are adapted and optimised for use on the BNC 4. UB2/3/4 cutting die sets are mounted with adapter sets, forming tools via adapted mounting plates on the NCA units.
Both run at up to 300 1/min with a 200 kN servo eccentric press. The BNC 4 is configured to the MRP standard (4 × 40 mm strip, NC units up to 31 kN); the RM-NC is the LEANTOOL Radial R60 platform for Bihler RM and FINZER tools (4 × 80 mm strip, 20 kN / 120 mm units, up to 14 axes).
Yes; the RZV 2.1 servo feed is designed for strip and wire material without retooling mechanical components, and material guides for different dimensions are changed quickly. Capacity is 4 × 40 mm strip and Ø 4 mm wire.
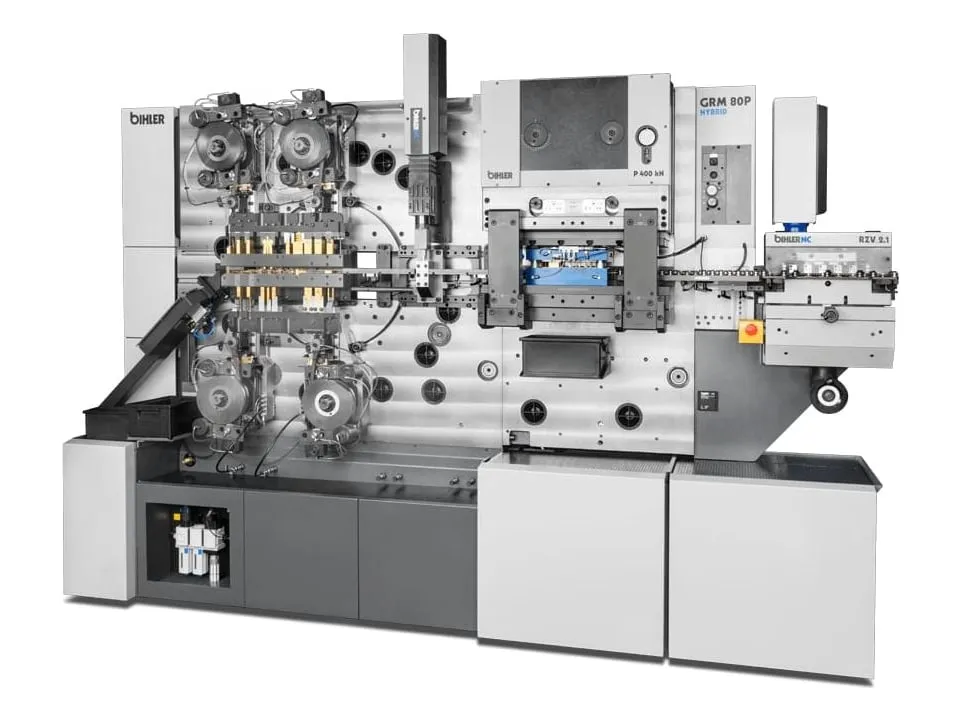 Bihler GRM 80 Universal multi-slide machine for large stamped and bent parts 250 1/min300–400 kN80 mm Technical data
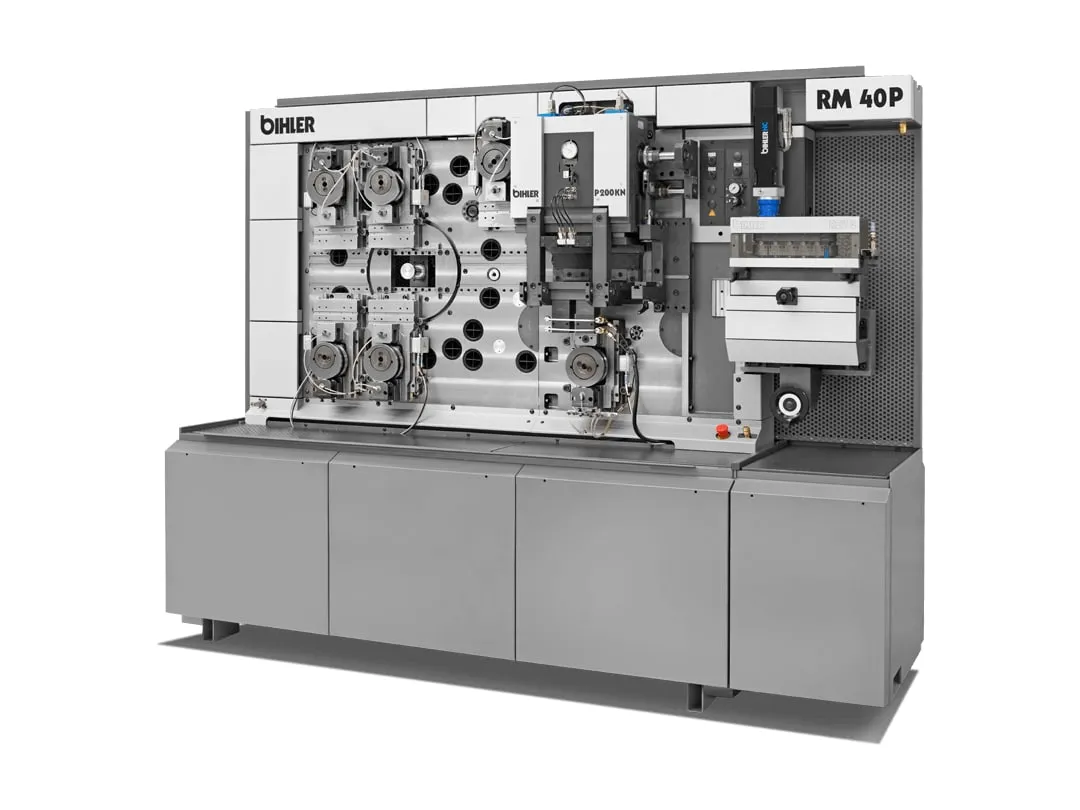 Bihler RM 40 Compact multi-slide machines for mass production of small precision stamped and formed parts 350 1/min90–200 kN60 mm Technical data
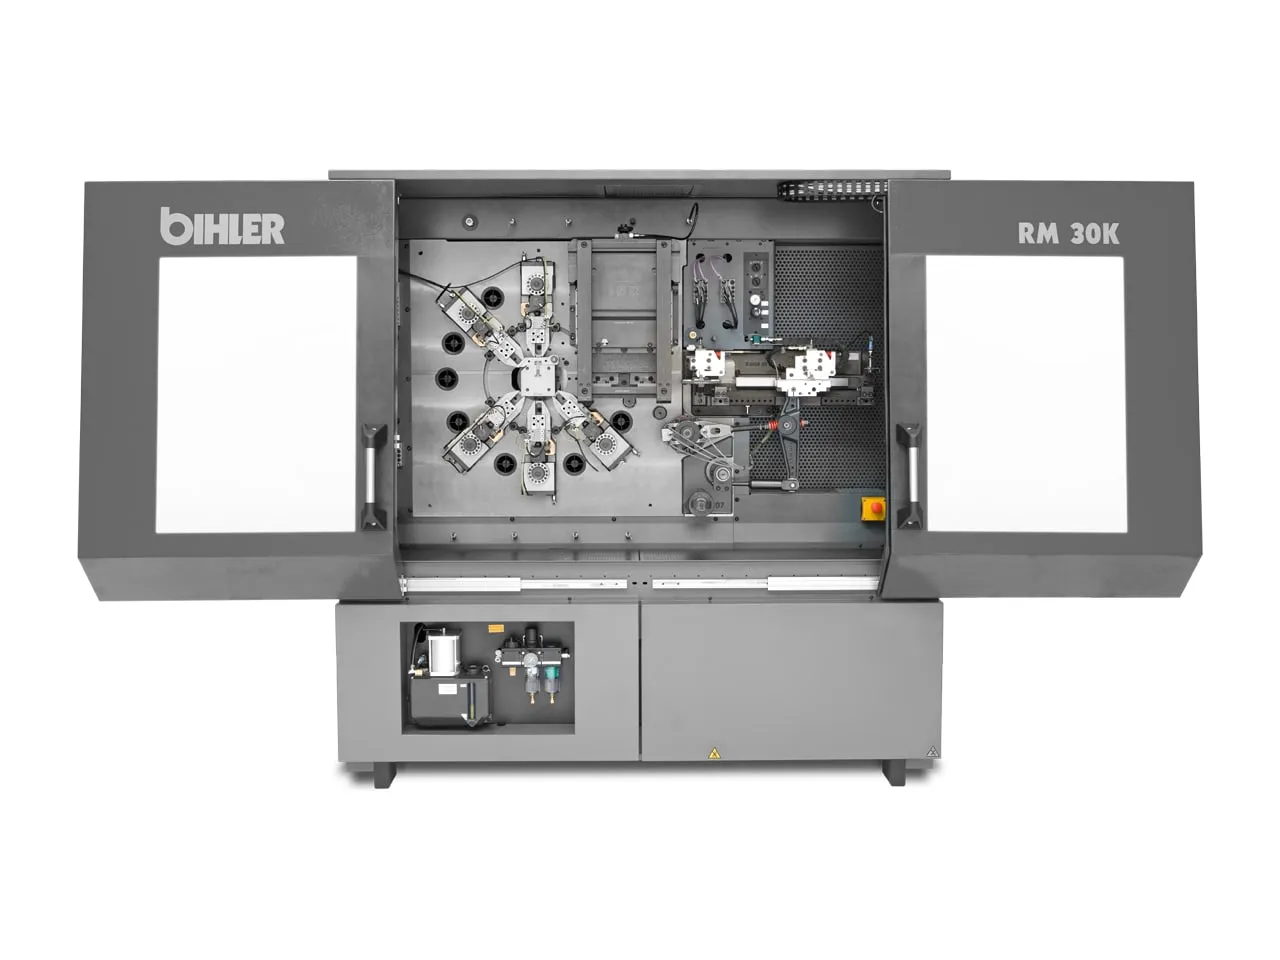 Bihler RM 30K Compact multi-slide machine for mass production of small stamped and formed metal parts 350 1/min90 kN900 mm Technical data
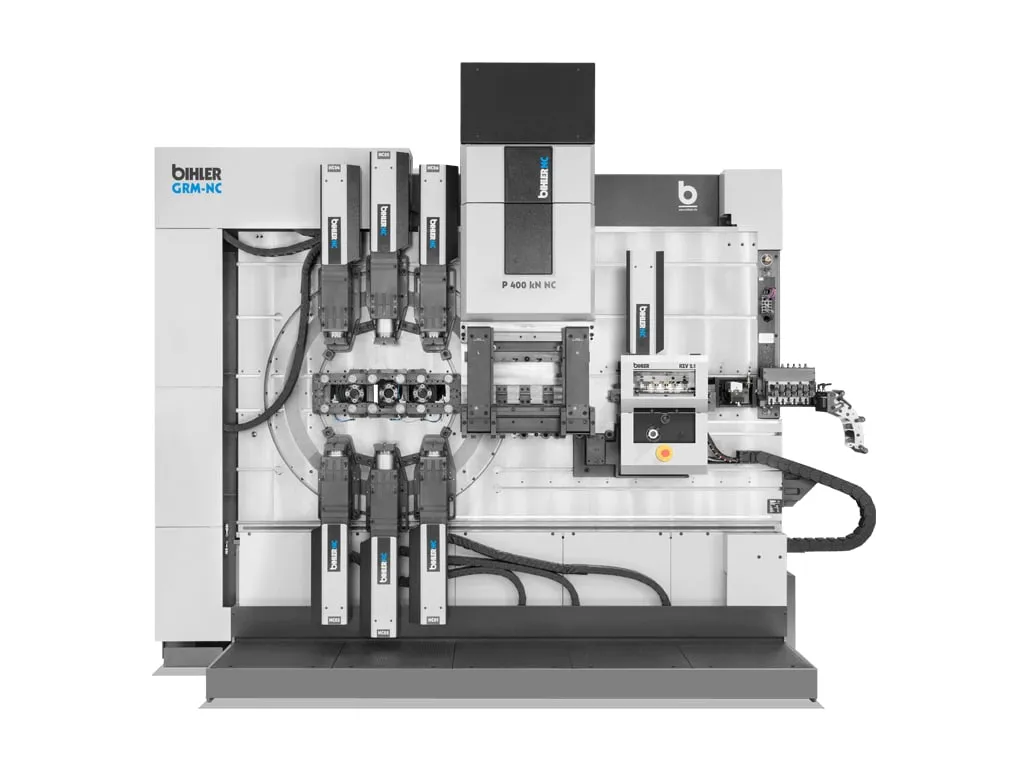 Bihler GRM-NC Universal servo multi-slide machine for small and medium batches 250 1/min400 kN90 mm Technical data
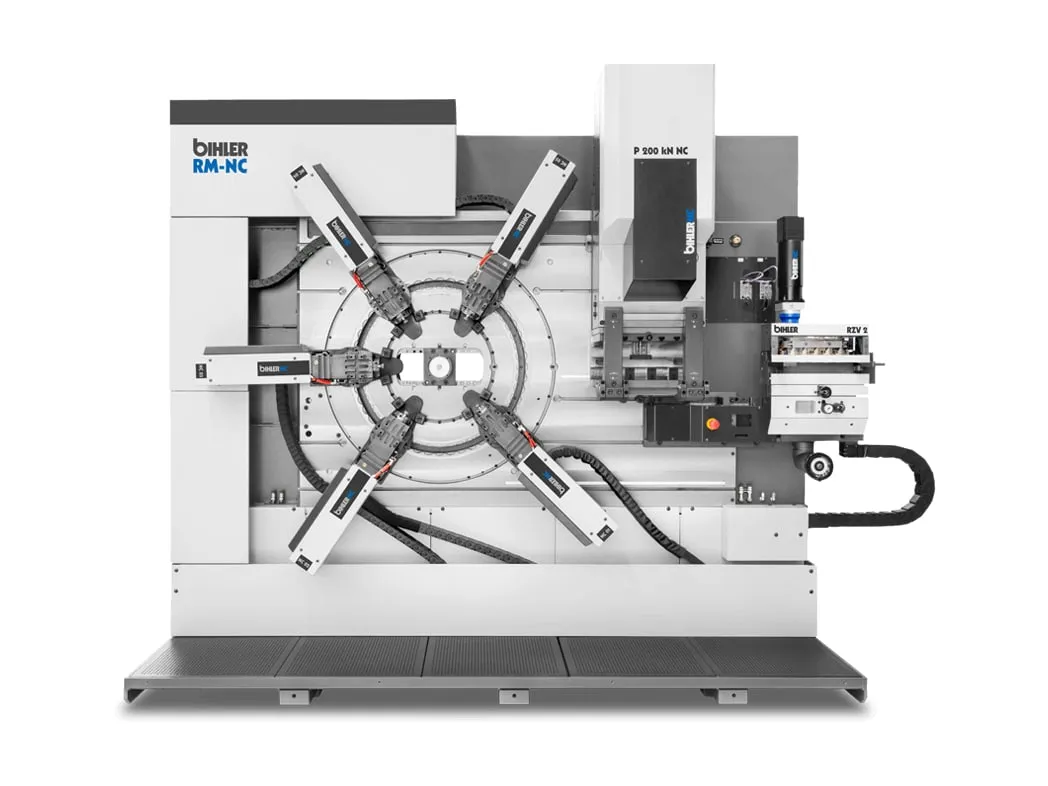 Bihler RM-NC Servo multi-slide machine for small and medium batches with radial tooling 300 1/min200 kN80 mm Technical data
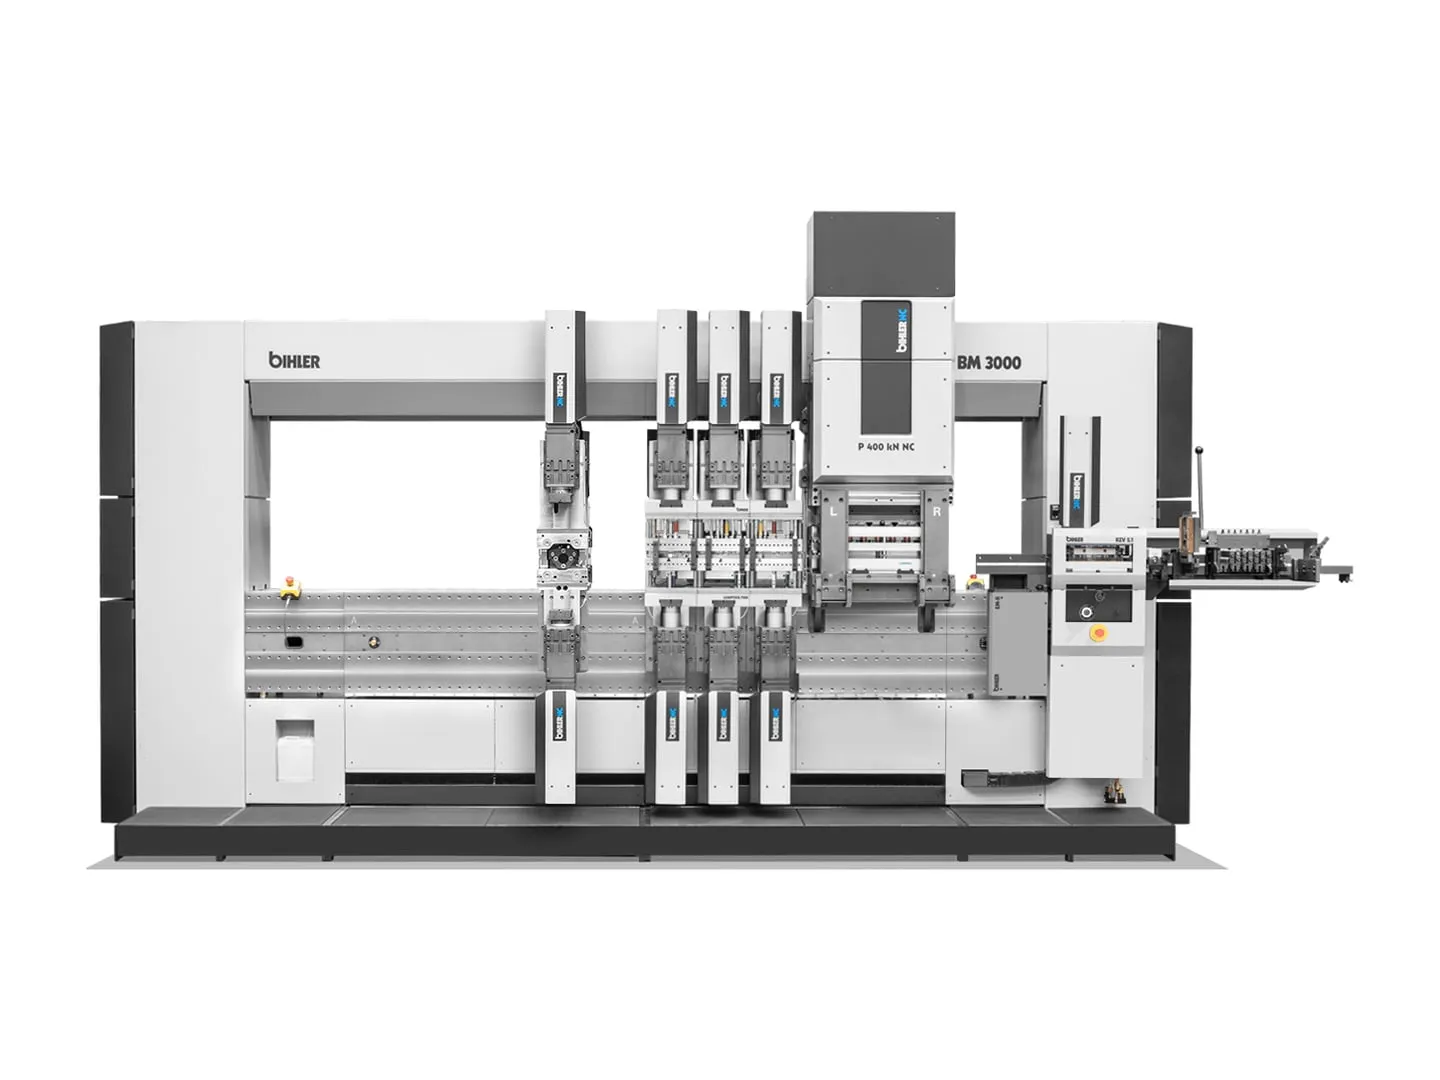 Bihler BIMERIC BM Modular servo production and assembly system from raw material to ready-to-install assemblies 250 1/min400 kN80 mm Technical data
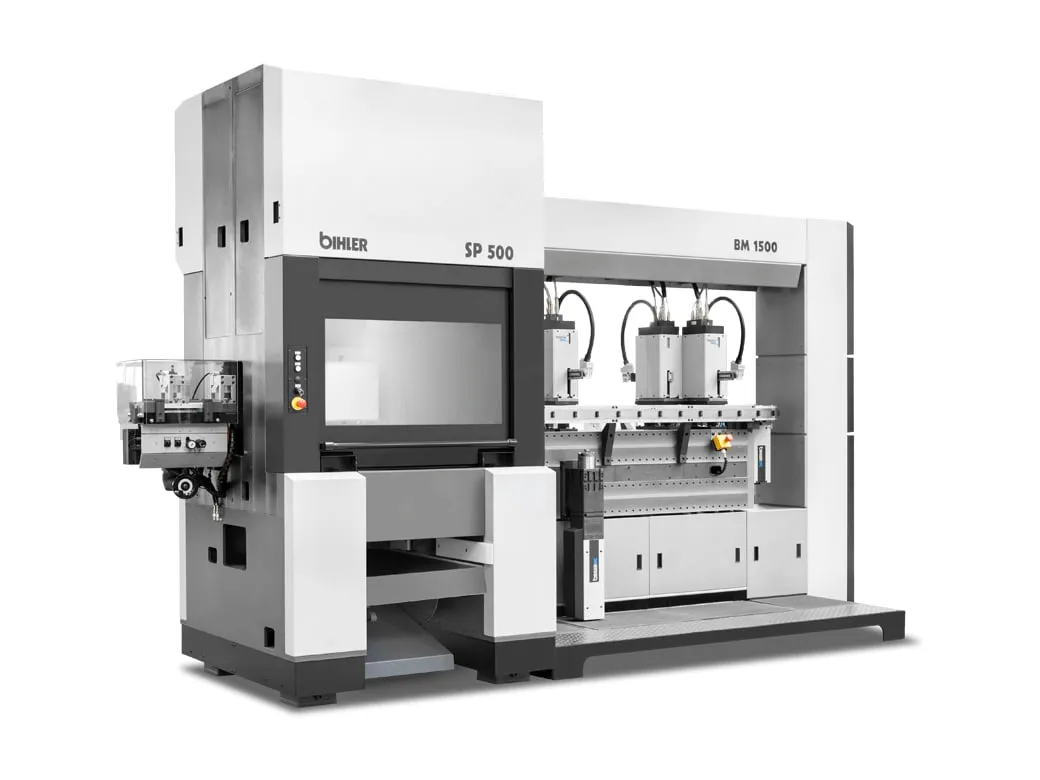 Bihler BIMERIC SP Sub-assembly production system combining a servo press with the BIMERIC platform for progressive dies 250 1/min500 kN15–63 mm Technical data
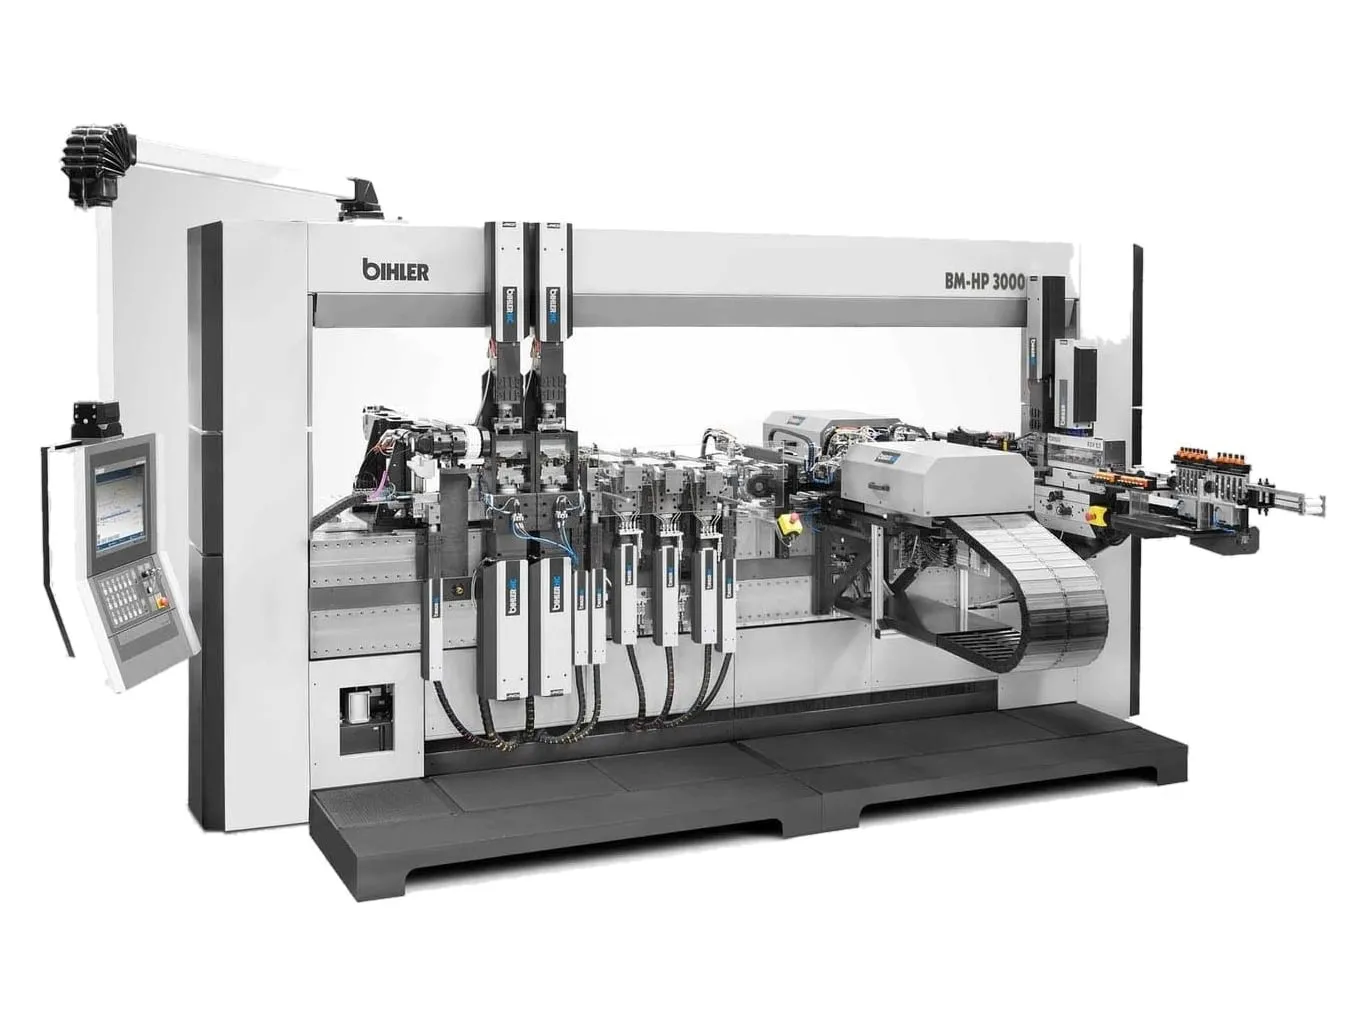 Bihler BM-HP 3000 Servo system producing complete electric-motor hairpins from flat wire on the coil 60–120/min3.2 m/s±0.02 mm Technical data
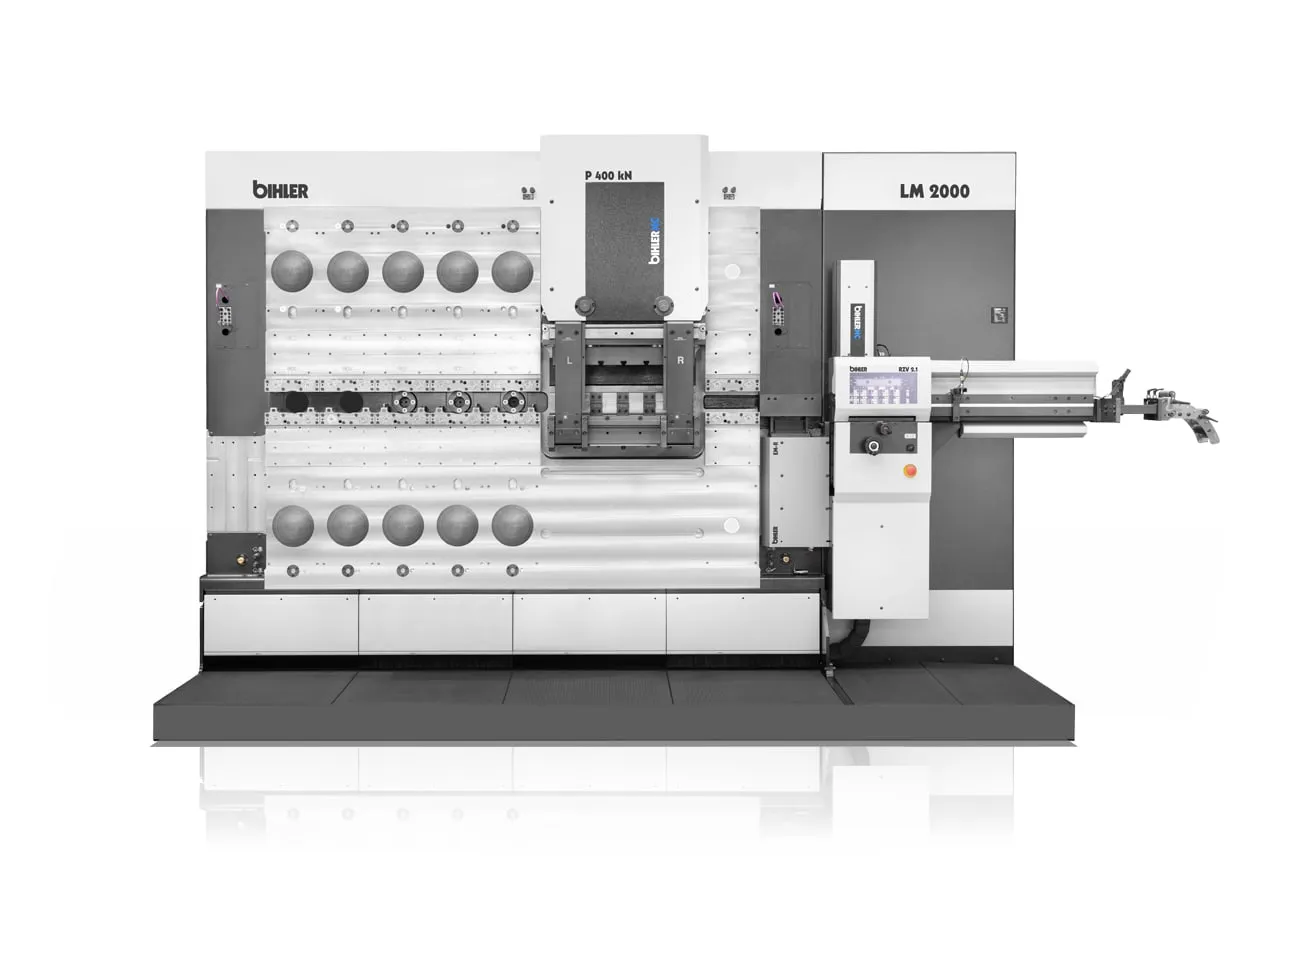 Bihler LM 2000-KT / LM 2000-NC Modular linear machine platform with cam-controlled (KT) or servo-controlled (NC) units 500 1/min250 1/min2,000 mm Technical data
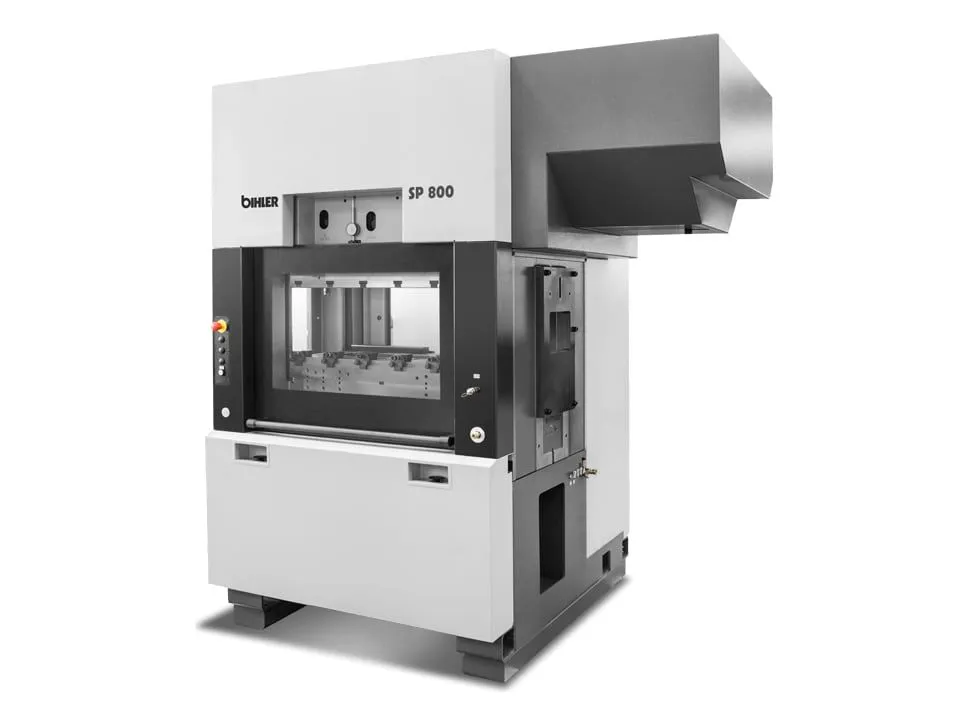 Bihler SP 800 800 kN servo press for progressive tools; stand-alone or combined with the BIMERIC 800 kN200 1/min30 mm Technical data
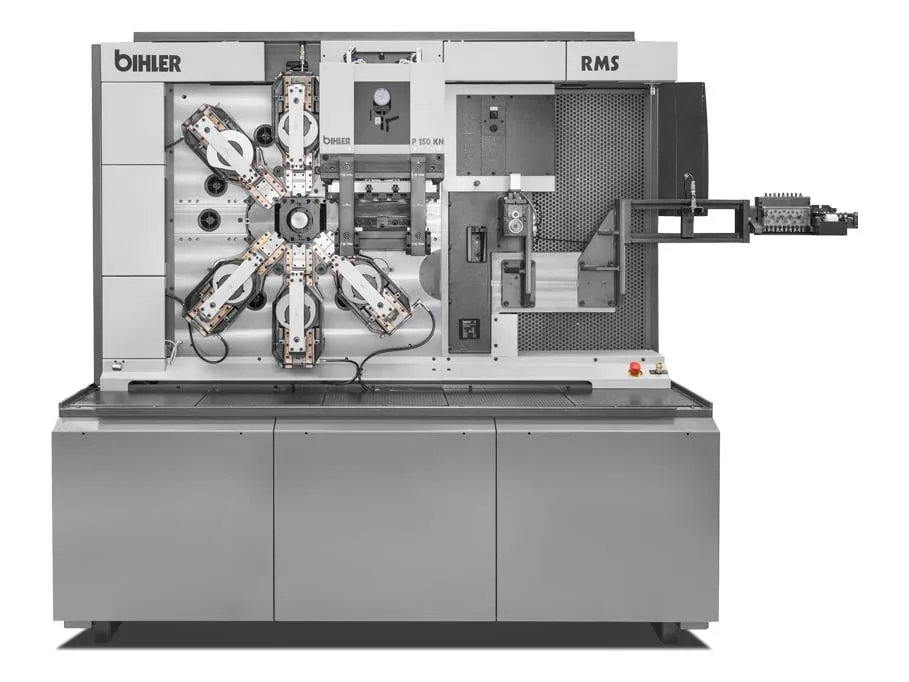 Bihler RM S High-speed multi-slide machine for stamped and formed parts made from high-tensile steels 600 1/min150 kN900 mm Technical data
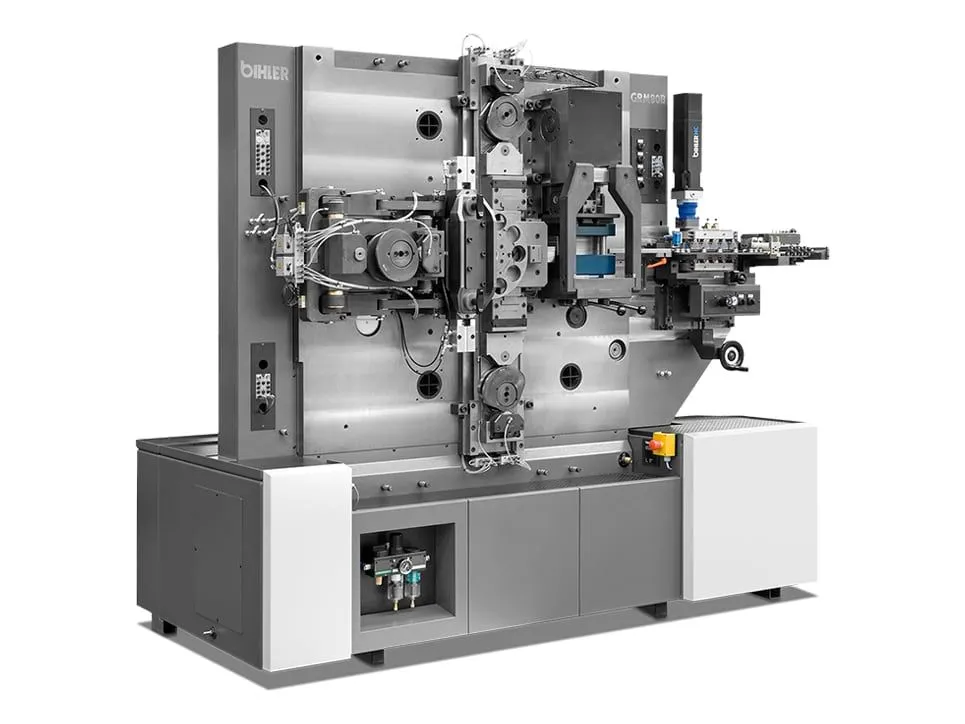 Bihler GRM 80B Bushing machine with a standardised tooling concept for mass production of straight and flanged bushings 220 1/min160 1/min15–40 mm Technical data
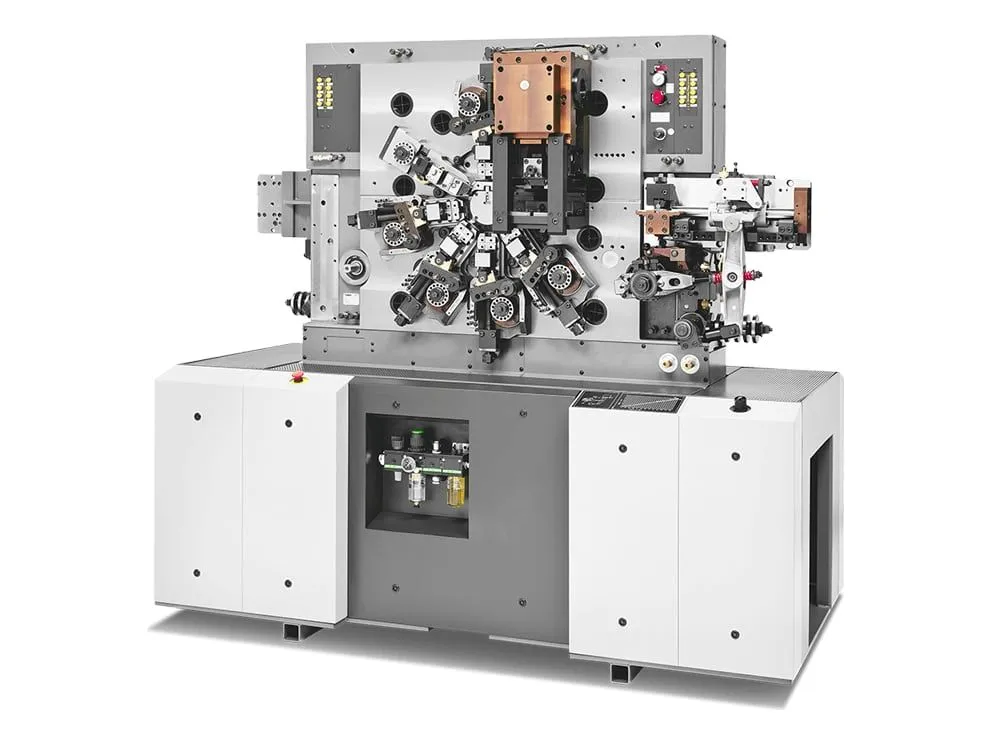 Bihler MC 42 Multi-slide machine with two processing faces for small stamped and formed parts and sub-assemblies 350 1/min90 kN60 kN Technical data
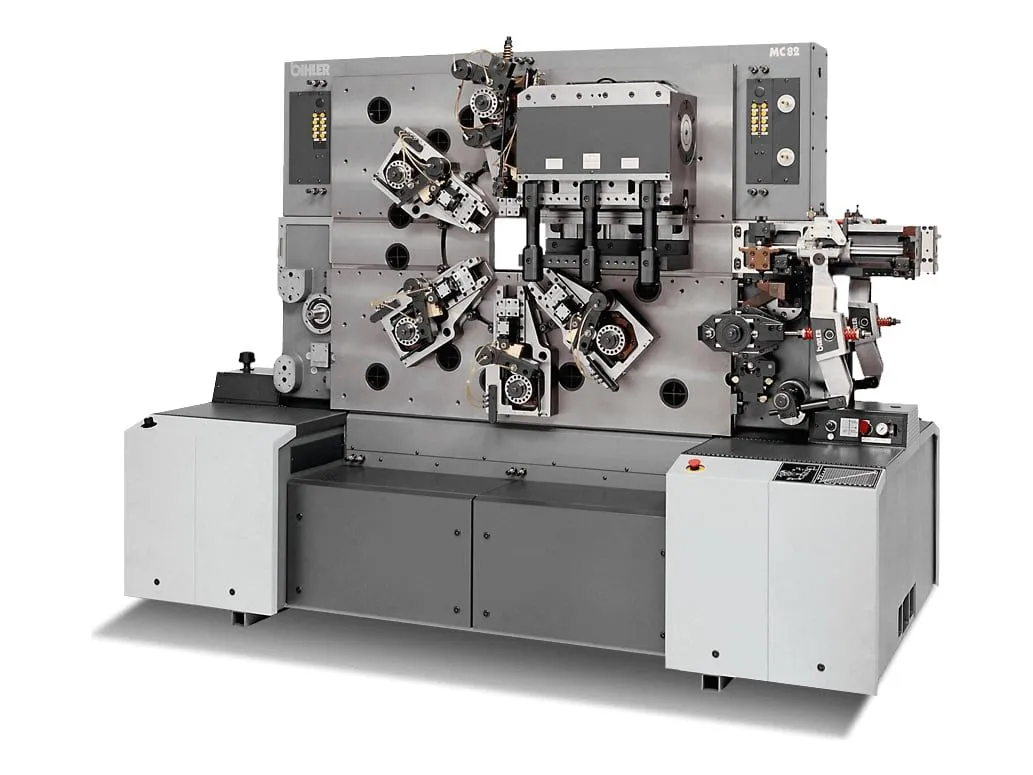 Bihler MC 82 Multi-slide machine with two processing faces for larger stamped and formed parts and sub-assemblies 250 1/min300 kN90 kN Technical data
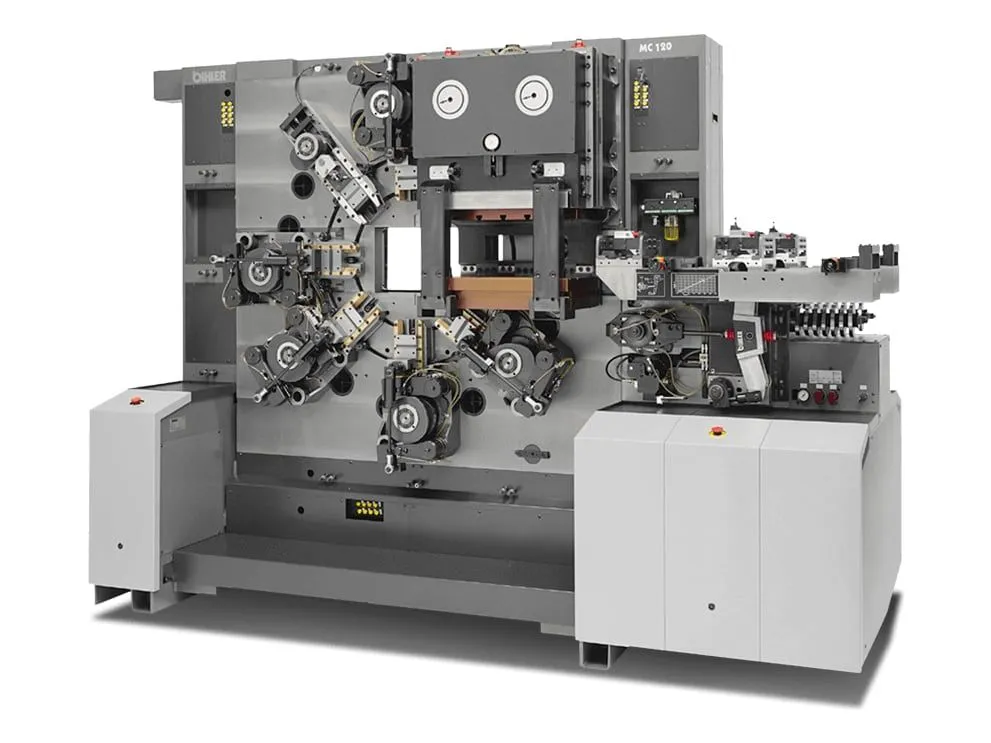 Bihler MC 120 Multi-slide machine with a 700 kN press and two processing faces for large stamped and formed parts and sub-assemblies 150 1/min700 kN160 kN Technical data
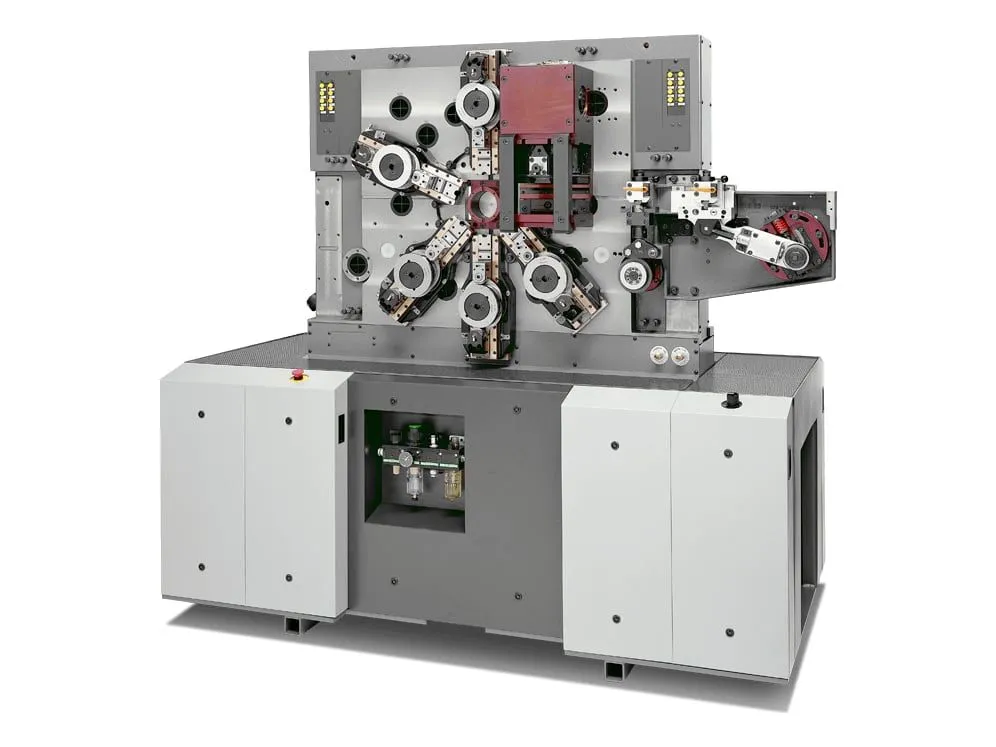 Bihler MCS 1 High-speed multi-slide machine with two processing faces, running at up to 800 strokes per minute 800 1/min70 kN30 kN Technical data
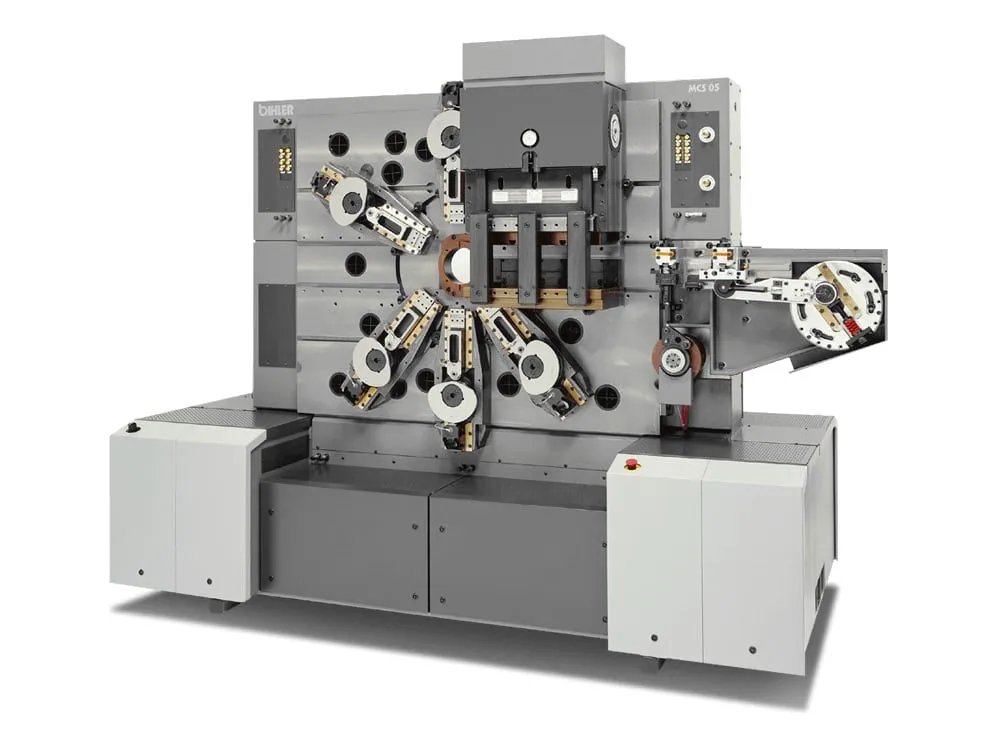 Bihler MCS 05 High-speed multi-slide machine with two processing faces for large stamped and formed parts and sub-assemblies 500 1/min300 kN50 kN Technical data
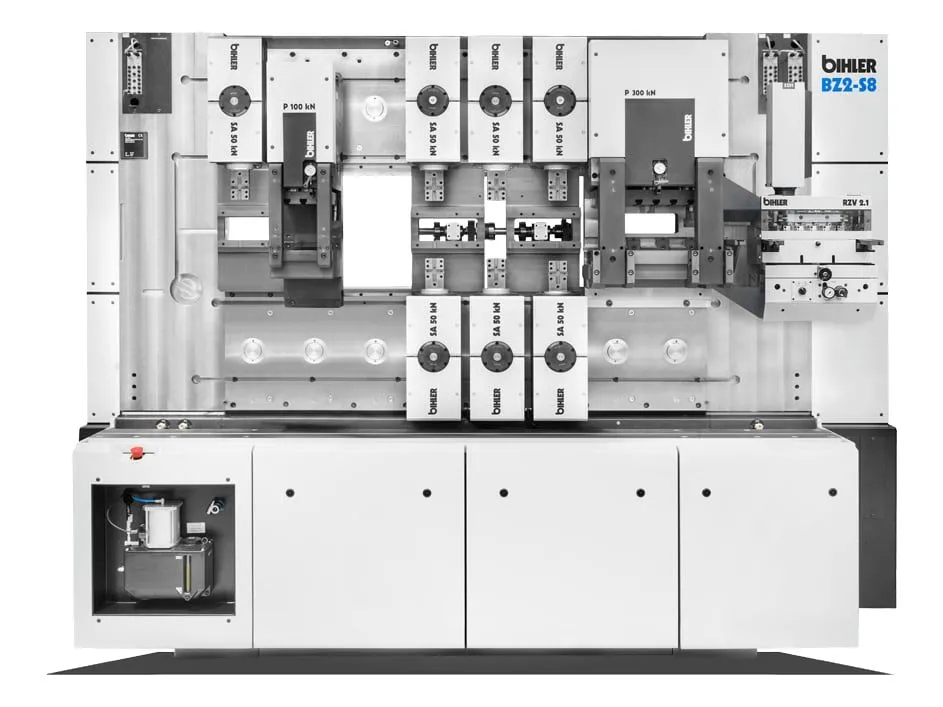 Bihler BZ2-S8 High-performance processing centre driven by servo motors for mass production of stamped and formed parts and sub-assemblies 700 1/min300 kN50 kN Technical data
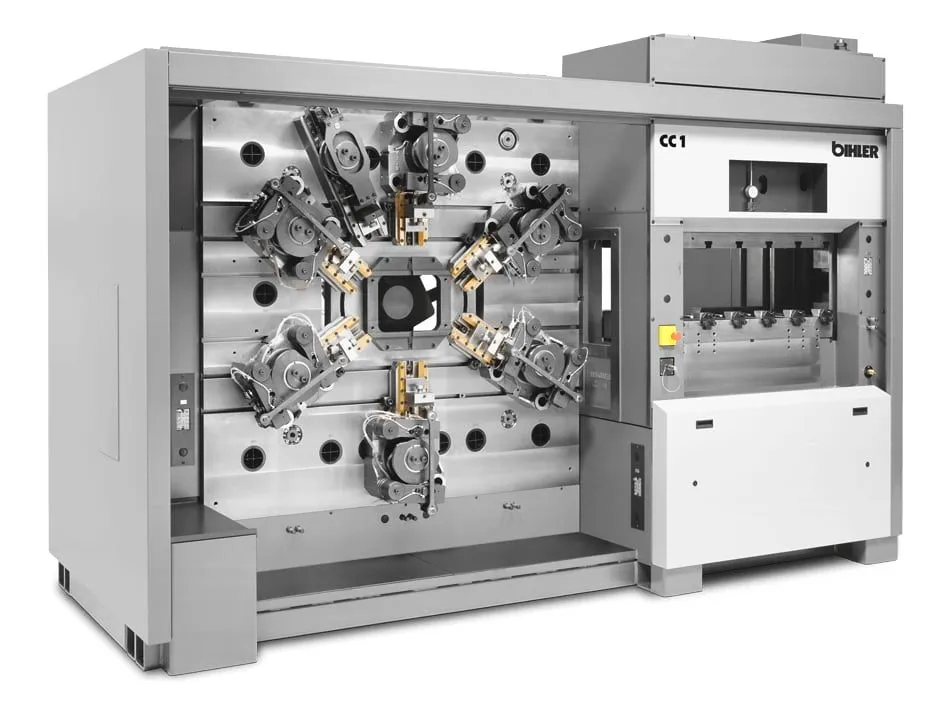 Bihler CC 1 COMBITEC processing centre with a separate 800 kN press module for long, bulky stamped and formed parts and sub-assemblies 200 1/min800 kN160 kN Technical data