Since 198343 years serving Turkish industry

Servo production and assembly systems

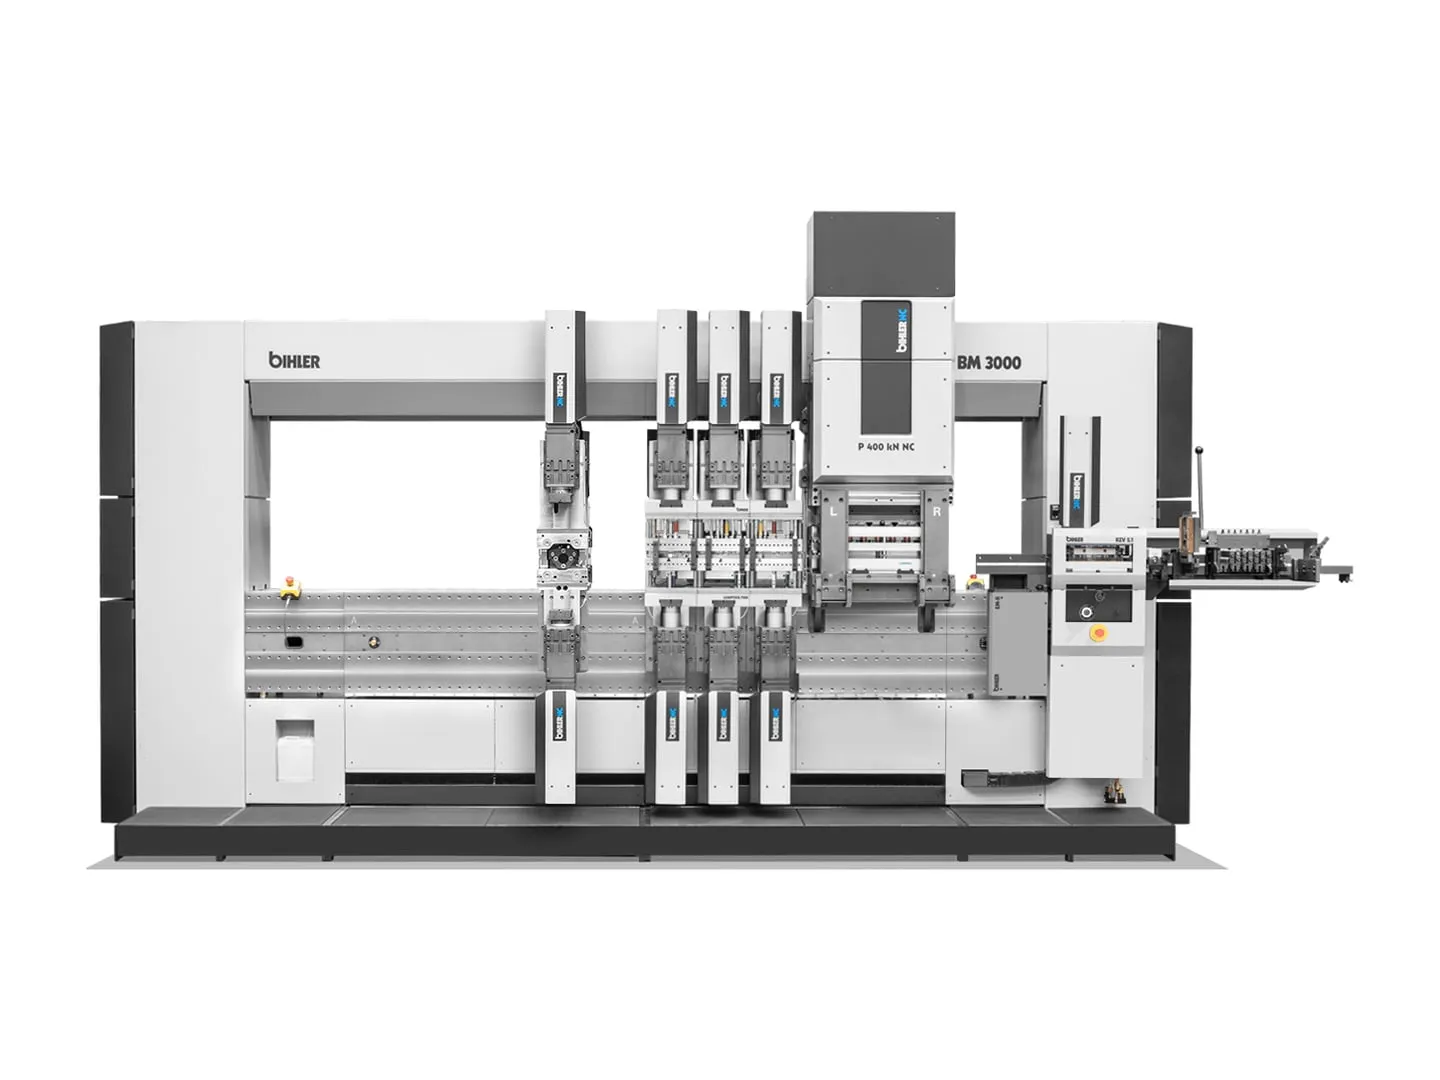
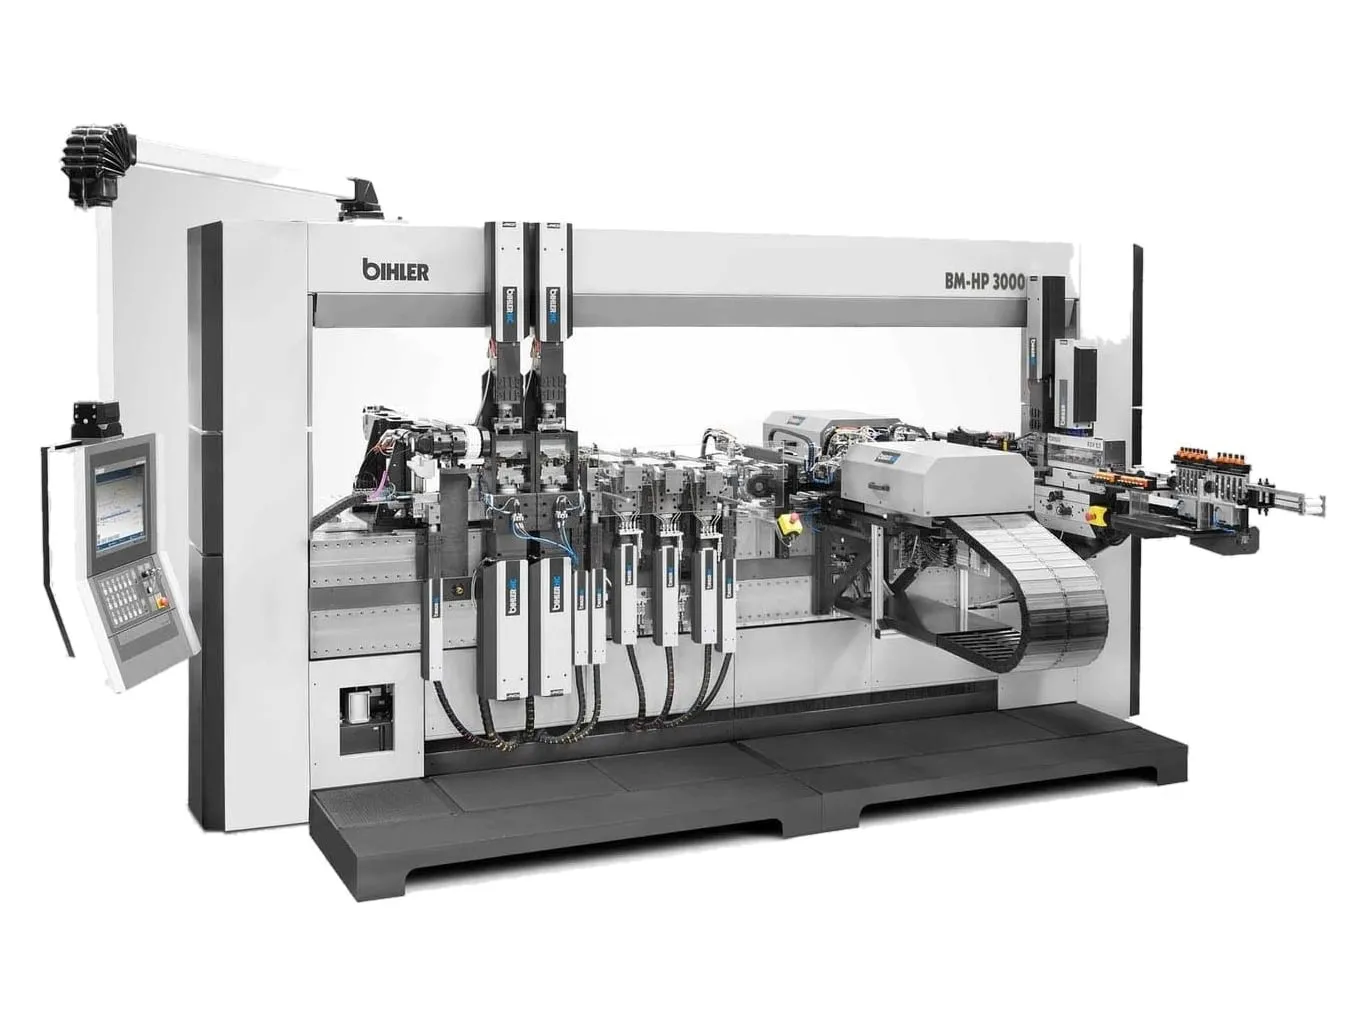
Bihler BM-HP 3000

Servo system producing complete electric-motor hairpins from flat wire on the coil

Bihler BM-HP 3000 hairpin production system
60–120/min Hairpin output
3.2 m/s Wire feed speed
±0.02 mm Feed repeat accuracy
< 0.05 mm Total cross-section loss
3× Cycle rate vs sequential systems

ⓘ Manufacturer data (Bihler BM-HP 3000 page, BM-HP brochure 01/24, b on top 2023); depends on material cross-section and leg length. Values may change and vary; not binding on Boztaş.

Why BM-HP 3000?

One system from coil to storage

Multi-stage straightening, slip-free feeding with the RZV 2.1, cutting, mechanical enamel stripping and pin-end chamfering, 2D pre-bending, 3D die bending and mono-component storage on the same machine; fully automated coil change.
Variant change on the fly

Variants are changed solely by calling up stored data, at a constant machine cycle rate, without downtime or operator intervention; all common hairpin, connection pin and I-pin types can be produced.

Controlled enamel stripping

A sensor unit continuously measures enamel thickness and the combined thickness of enamel and copper inline; total copper cross-section loss stays below 0.05 mm and the pin ends get a pure metal surface.

Variants

BM-HP 3000

Standard hairpin line based on the BIMERIC servo production system; modular process steps, central VariControl VC 1, automatic coil change

Suited to: Industrial mass production of electric-motor stator hairpins

Option: final geometry measurement

Measurement of the part geometry after 3D die bending and inline adjustment

Suited to: Hairpin geometries with tight tolerances

Extension and line integration

Additional process modules can be added or the module arrangement changed; defined interfaces on the last module for links to stator lines or turnkey electric-motor systems

Suited to: Complete stator production lines

Technical data

Columns to compare
FeatureBM-HP 3000
Performance
Output 60–120 finished hairpins per minute (depending on material cross-section and leg length)
Cycle rate three times that of sequential systems (manufacturer)
Material
Material Enamelled flat copper wire, directly from the coil
Part types Common hairpin, connection pin and I-pin types
Process steps
Straightening and feed Multi-stage straightening; RZV 2.1 servo feed up to 3.2 m/s, slip-free, repeat accuracy ±0.02 mm; three-point surface clamping protects the enamel
Cutting To stretched length with an NC module and cutting punch; no deformation, little burr
Stripping and chamfering Mechanical, NC-controlled enamel stripping; both pin ends chamfered simultaneously; inline measurement of enamel and total thickness; cross-section loss < 0.05 mm
Bending Parallel-cycle 2D swivel pre-bending (geometry programmable) + 3D die bending with NC units
Output handling Removal via conveyor belt for sorting and mono-component storage; interfaces for line links
Control
Control VariControl VC 1, central for all processes
Coil change Fully automated
Dimensions and weight
Dimensions / weight —

Manufacturer data (Bihler BM-HP 3000 page, BM-HP brochure 01/24, b on top 2023); depends on material cross-section and leg length.

Processes that can be combined on this machine

  • Straightening
  • Cutting
  • Insulation stripping
  • Chamfering
  • Bending (2D / 3D)
  • Measuring

Typical workpieces

  • Hairpins (Hairpins)
  • Connection pins (Anschlusspins)
  • I-pins (I-Pins)

Related industries: Automotive

Frequently asked questions

Which hairpin types does the BM-HP 3000 produce?

According to the manufacturer, all common hairpin, connection pin and I-pin types, made from enamelled flat copper wire on the coil; output is 60–120 hairpins per minute depending on material cross-section and leg length.

Is the enamel stripped by laser?

No; stripping is mechanical and NC-controlled. A sensor unit continuously measures enamel and total thickness and the station processes each hairpin individually; total cross-section loss is generally below 0.05 mm, and four-sided chamfering of the ends is part of the same process.

Does a variant change require downtime?

No; variants are changed solely by calling up stored data, at a constant machine cycle rate, without stopping the machine and without operator intervention.

Other Bihler models

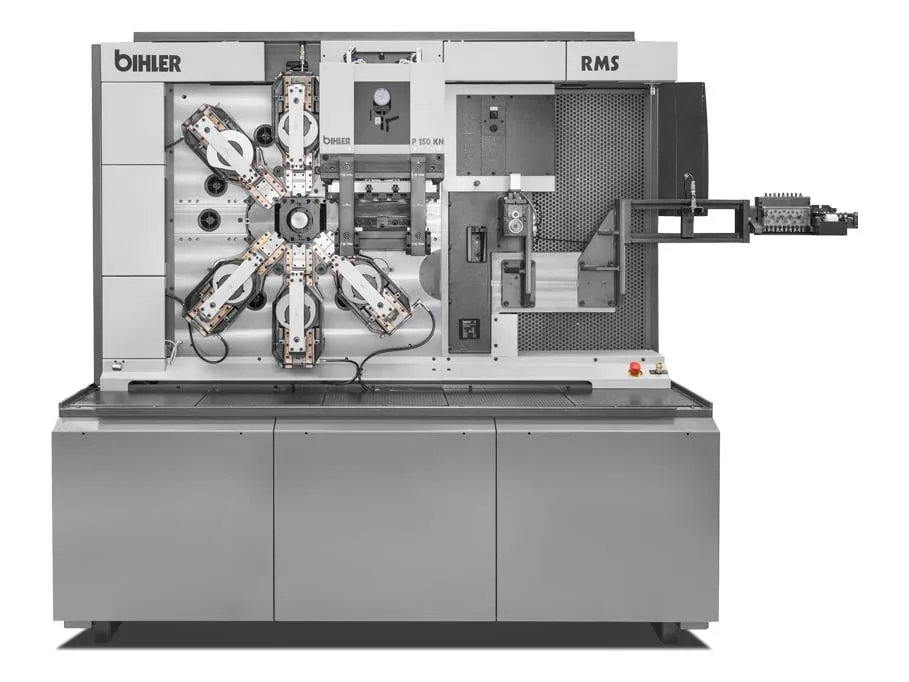
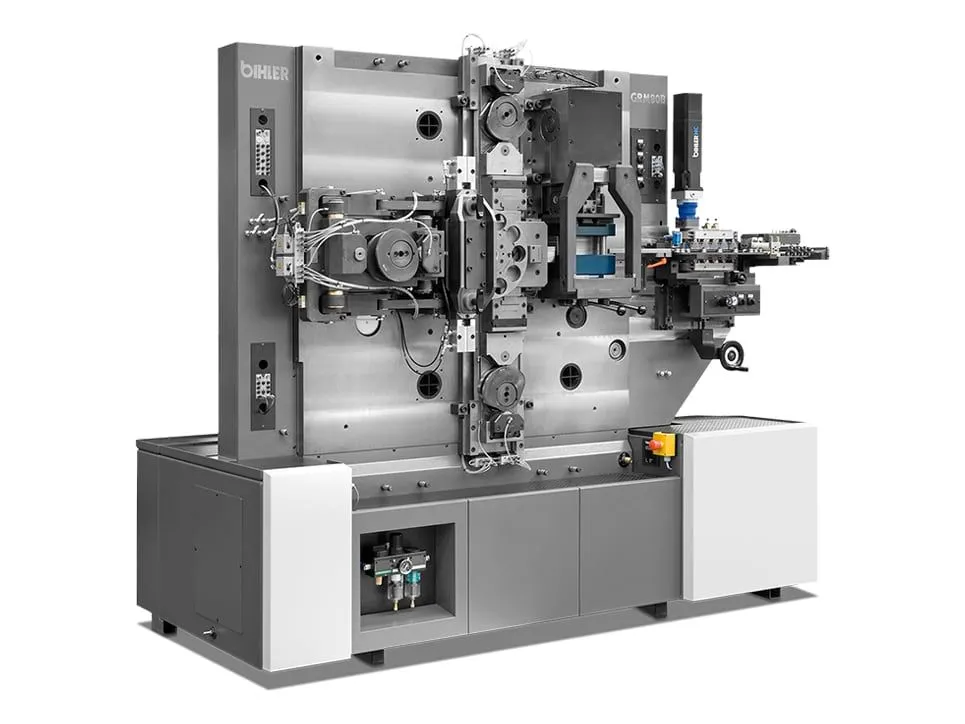
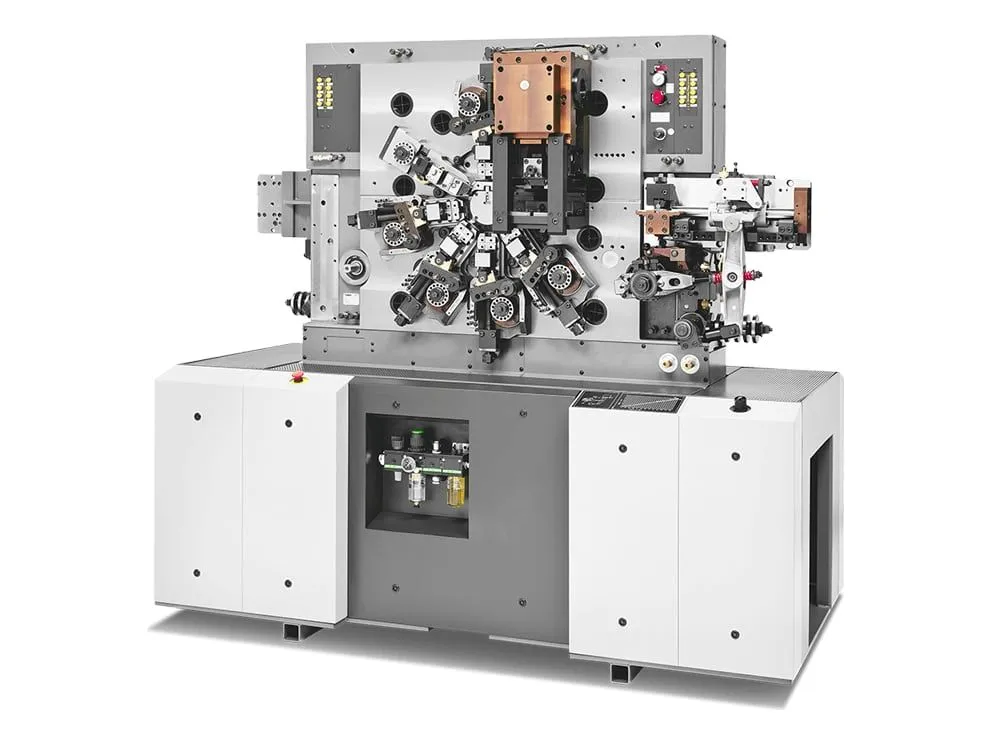
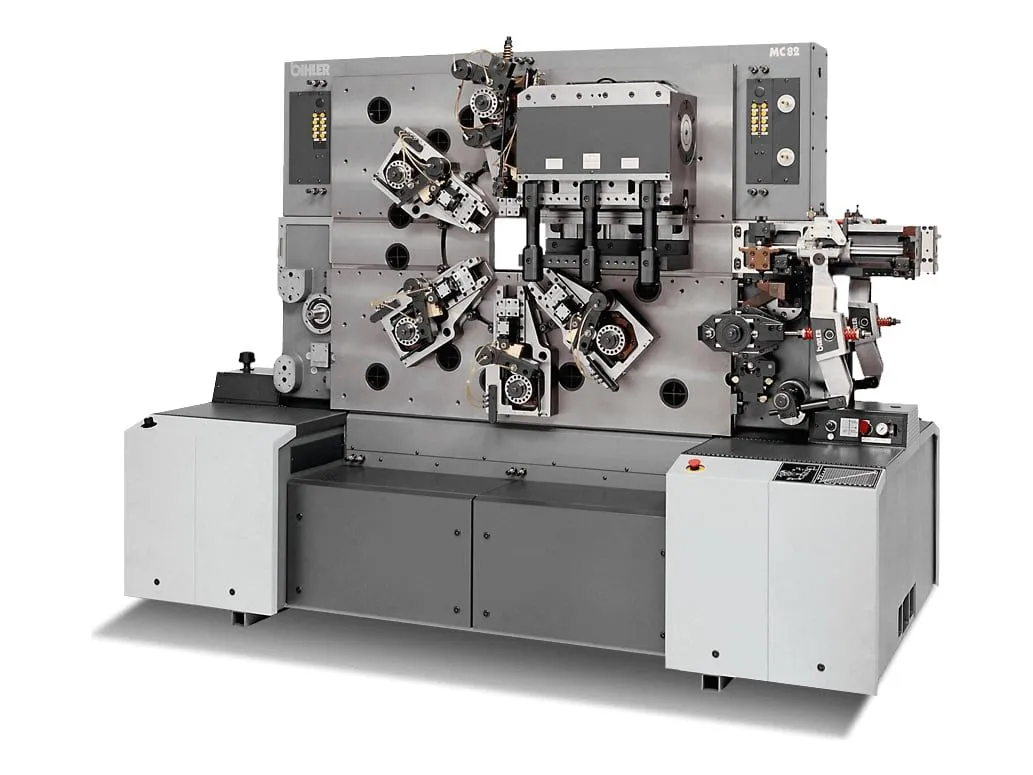
Bihler GRM 80 Bihler GRM 80 Universal multi-slide machine for large stamped and bent parts 250 1/min300–400 kN80 mm Technical data Bihler RM 40 Bihler RM 40 Compact multi-slide machines for mass production of small precision stamped and formed parts 350 1/min90–200 kN60 mm Technical data Bihler RM 30K Bihler RM 30K Compact multi-slide machine for mass production of small stamped and formed metal parts 350 1/min90 kN900 mm Technical data Bihler GRM-NC Bihler GRM-NC Universal servo multi-slide machine for small and medium batches 250 1/min400 kN90 mm Technical data Bihler RM-NC Bihler RM-NC Servo multi-slide machine for small and medium batches with radial tooling 300 1/min200 kN80 mm Technical data Bihler BNC 4 Bihler BNC 4 Servo multi-slide production system compatible with MRP tooling 300 1/min200 kN31 kN Technical data Bihler BIMERIC BM Bihler BIMERIC BM Modular servo production and assembly system from raw material to ready-to-install assemblies 250 1/min400 kN80 mm Technical data Bihler BIMERIC SP Bihler BIMERIC SP Sub-assembly production system combining a servo press with the BIMERIC platform for progressive dies 250 1/min500 kN15–63 mm Technical data Bihler LM 2000-KT / LM 2000-NC Bihler LM 2000-KT / LM 2000-NC Modular linear machine platform with cam-controlled (KT) or servo-controlled (NC) units 500 1/min250 1/min2,000 mm Technical data Bihler SP 800 Bihler SP 800 800 kN servo press for progressive tools; stand-alone or combined with the BIMERIC 800 kN200 1/min30 mm Technical data Bihler RM S Bihler RM S High-speed multi-slide machine for stamped and formed parts made from high-tensile steels 600 1/min150 kN900 mm Technical data Bihler GRM 80B Bihler GRM 80B Bushing machine with a standardised tooling concept for mass production of straight and flanged bushings 220 1/min160 1/min15–40 mm Technical data Bihler MC 42 Bihler MC 42 Multi-slide machine with two processing faces for small stamped and formed parts and sub-assemblies 350 1/min90 kN60 kN Technical data Bihler MC 82 Bihler MC 82 Multi-slide machine with two processing faces for larger stamped and formed parts and sub-assemblies 250 1/min300 kN90 kN Technical data Bihler MC 120 Bihler MC 120 Multi-slide machine with a 700 kN press and two processing faces for large stamped and formed parts and sub-assemblies 150 1/min700 kN160 kN Technical data Bihler MCS 1 Bihler MCS 1 High-speed multi-slide machine with two processing faces, running at up to 800 strokes per minute 800 1/min70 kN30 kN Technical data Bihler MCS 05 Bihler MCS 05 High-speed multi-slide machine with two processing faces for large stamped and formed parts and sub-assemblies 500 1/min300 kN50 kN Technical data Bihler BZ2-S8 Bihler BZ2-S8 High-performance processing centre driven by servo motors for mass production of stamped and formed parts and sub-assemblies 700 1/min300 kN50 kN Technical data Bihler CC 1 Bihler CC 1 COMBITEC processing centre with a separate 800 kN press module for long, bulky stamped and formed parts and sub-assemblies 200 1/min800 kN160 kN Technical data

Catalogue

We will e-mail you the catalogue

Enter your details and we will send the download link to your e-mail address straight away.

Your details are used only to send this catalogue and to contact you about your request. KVKK Notice