Since 198343 years serving Turkish industry

Linear machines

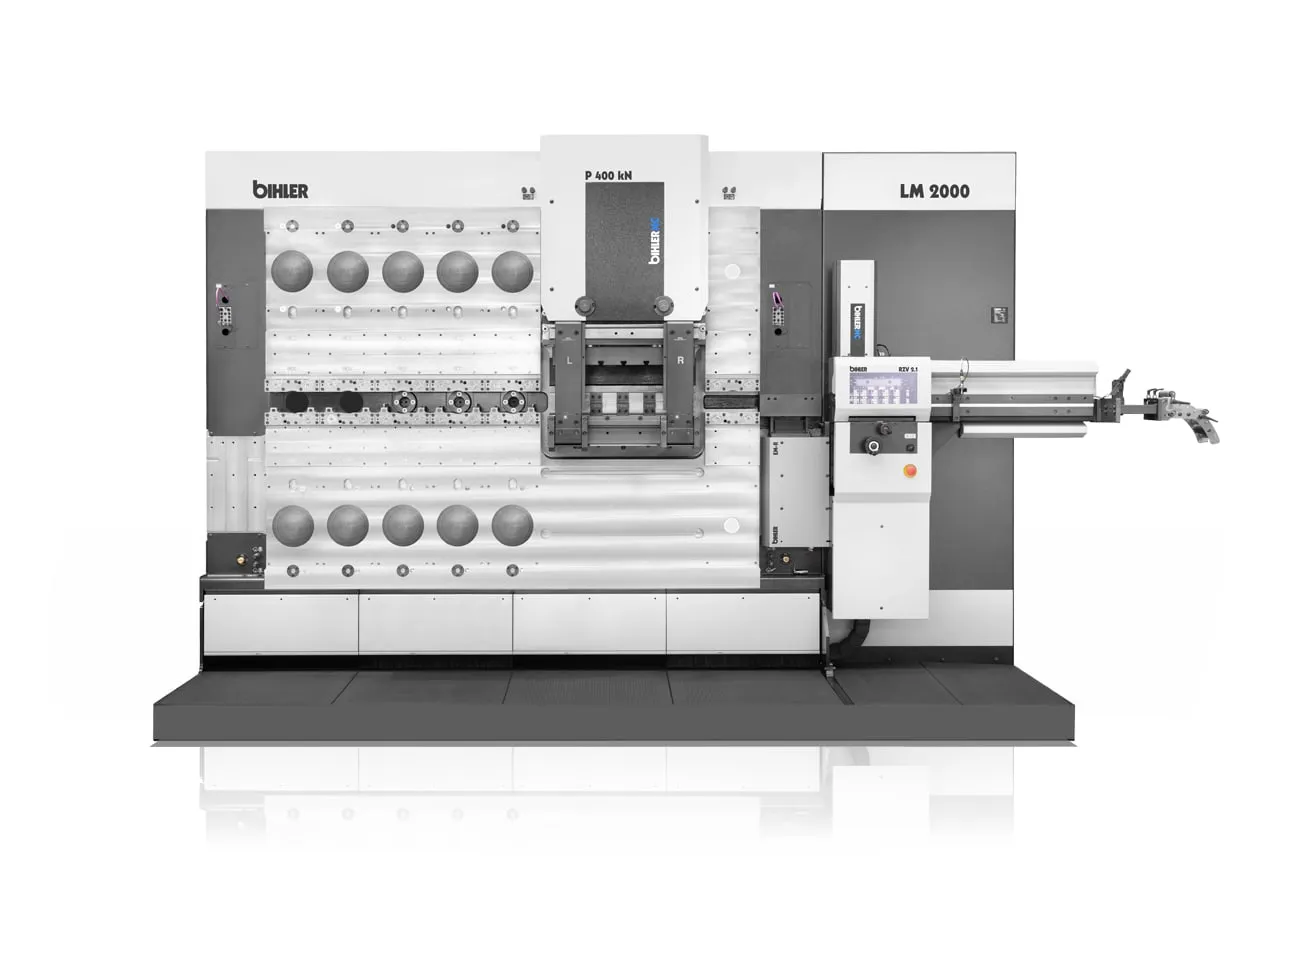
Bihler LM 2000-KT / LM 2000-NC

Modular linear machine platform with cam-controlled (KT) or servo-controlled (NC) units

Bihler LM 2000 linear machine platform
500 1/min Stroke rate (LM 2000-KT)
250 1/min Stroke rate (LM 2000-NC)
2,000 mm Processing length
400 kN Press force
80 mm Strip width

ⓘ Manufacturer data (Bihler LM 2000-KT / LM 2000-NC product page); depends on material and process. Values may change and vary; not binding on Boztaş.

Why LM 2000-KT / LM 2000-NC?

One platform, two variants

The units in the forming area are cam-controlled on the LM 2000-KT and servo-controlled on the LM 2000-NC. The manufacturer positions the KT for medium to large batches (few variants) and the NC for small to medium batches (many variants).
Standard tool interfaces

The press area is compatible with Meusburger SBP 400 and SBH 400 standard cutting frames; the module stations in the linear area have standard interfaces and a zero-point clamping system with hydraulic clamping. Tools can be shared across the Bihler Modular Series machines (LM 2000-KT/-NC, BIMERIC, GRM-NC).

Up to 15 movements, plus added processes

Each of the five module stations in the linear area offers up to three movements from three directions (top, bottom, 3rd level). The platform can be extended with modules for screw joining (MSE 250), thread forming (GSE 250), laser welding (LSM 250) and insulator assembly (MMI 250).

Variants

LM 2000-KT

Cam-controlled slide units in the forming area (max. 31 kN, stroke max. 28 mm); up to 500 1/min. Manual quicklift to reach the set-up and maintenance position without changing the cam; cams are replaced with a quick-change system.

Suited to: Medium to large batches, few variants

LM 2000-NC

Servo units in the forming area (max. 31 kN, stroke max. 100 mm); up to 250 1/min. Operating stroke, position and motion profile are freely programmable; manual interventions such as cam changes and stroke position adjustment are no longer needed.

Suited to: Small to medium batches, many variants

Technical data

Columns to compare
FeatureLM 2000-KTLM 2000-NC
Performance
Stroke rate stepless, max. 500 1/minstepless, max. 250 1/min
Press 400 kN eccentric press; fixed stroke 16 mm; stroke position adjustment 3.5 mm, stepless400 kN eccentric press; fixed stroke 16 mm; stroke position adjustment 3.5 mm, stepless
Forming units Cam-controlled slide units: max. 31 kN; stroke max. 28 mm; stroke position adjustment 28 mm, steplessServo (NC) units: max. 31 kN; stroke max. 100 mm; stroke, position and motion profile freely programmable
Movements (linear area) Up to three at each of 5 module stations, up to 15 in total; optional servo slide unit under the pressUp to three at each of 5 module stations, up to 15 in total; optional servo slide unit under the press
Tool area and feed
Processing length 2,000 mm2,000 mm
Press tool area Compatible with Meusburger SBP 400 / SBH 400 standard cutting frames; nominal cutting-frame height at BDC 208 ±0.05 mm; table length 670 mmCompatible with Meusburger SBP 400 / SBH 400 standard cutting frames; nominal cutting-frame height at BDC 208 ±0.05 mm; table length 670 mm
Tool clamping (linear area) Standard interfaces; zero-point clamping system with hydraulic clampingStandard interfaces; zero-point clamping system with hydraulic clamping
NC central mandrel max. 5; max. 8.9 kN; stroke max. 95 mmmax. 5; max. 8.9 kN; stroke max. 95 mm
Feed RZV 2.1 servo radial gripper feed; any feed lengthRZV 2.1 servo radial gripper feed; any feed length
HLT 250 linear tool modules max. 500 1/min; strip thickness 0.1–1.0 mm; module change < 10 min—
Material
Strip width max. 80 mmmax. 80 mm
Strip thickness depends on material and processdepends on material and process
Control
Control VariControl VC 1 (version 3.0); 24-inch multi-touch displayVariControl VC 1 (version 3.0); 24-inch multi-touch display
Monitoring Press force monitoring (with overload protection) and bearing temperature monitoring; overload sensors in the slide unitsPress force monitoring (with overload protection) and bearing temperature monitoring; software overload protection and absolute measuring system in the NC units
Lubrication Oil circulation lubrication (oil temperature, fill level and contamination monitored); central lubrication system with two circuitsOil circulation lubrication (oil temperature, fill level and contamination monitored); central lubrication system with two circuits
Data interface OPC UA as standard; machine conditions can be transferred to an MES or ERP systemOPC UA as standard; machine conditions can be transferred to an MES or ERP system
Dimensions and weight
Weight (without tools) approx. 8,000 kgapprox. 8,000 kg

Manufacturer data (Bihler LM 2000-KT / LM 2000-NC product page); depends on material and process. The OPC UA row is taken from the Bihler Modular Series page.

Processes that can be combined on this machine

  • Stamping
  • Bending
  • Coining
  • Thread forming (GSE 250)
  • Screw joining (MSE 250)
  • Laser welding (LSM 250)
  • Contact welding
  • Assembly (MMI 250)

Typical workpieces

  • Stamped and formed parts from strip material (Stanzbiegeteile aus Bandmaterial)
  • Box terminals for boards (Kastenkontakte für Platinen)
  • Stainless steel cable holders for control cabinets (Edelstahl-Leitungshalter für Schaltschränke)
  • Flat springs (Bandfedern)

Related industries: Electronics and Connectors

Frequently asked questions

What is the difference between the LM 2000-KT and the LM 2000-NC?

Both are the same machine platform: 2,000 mm processing length, 400 kN press, strip up to 80 mm wide. They differ in the processing units in the linear area. The LM 2000-KT has cam-controlled slide units and reaches 500 1/min; the LM 2000-NC has servo units, reaches 250 1/min, and its stroke, position and motion profile are freely programmable.

Which cutting frames and tools does the LM 2000 use?

The press area is compatible with Meusburger SBP 400 and SBH 400 standard cutting frames. The module stations in the linear area have standard interfaces and a zero-point clamping system with hydraulic clamping; tools can be shared across the Bihler Modular Series machines (LM 2000-KT/-NC, BIMERIC, GRM-NC).

Which processes can be added besides forming?

The MSE 250 screw joining, GSE 250 thread forming, LSM 250 laser welding and MMI 250 insulator assembly modules can be added. Their software is included in the VC 1 control as standard, and each module can be set up in different positions to suit the process.

Other Bihler models

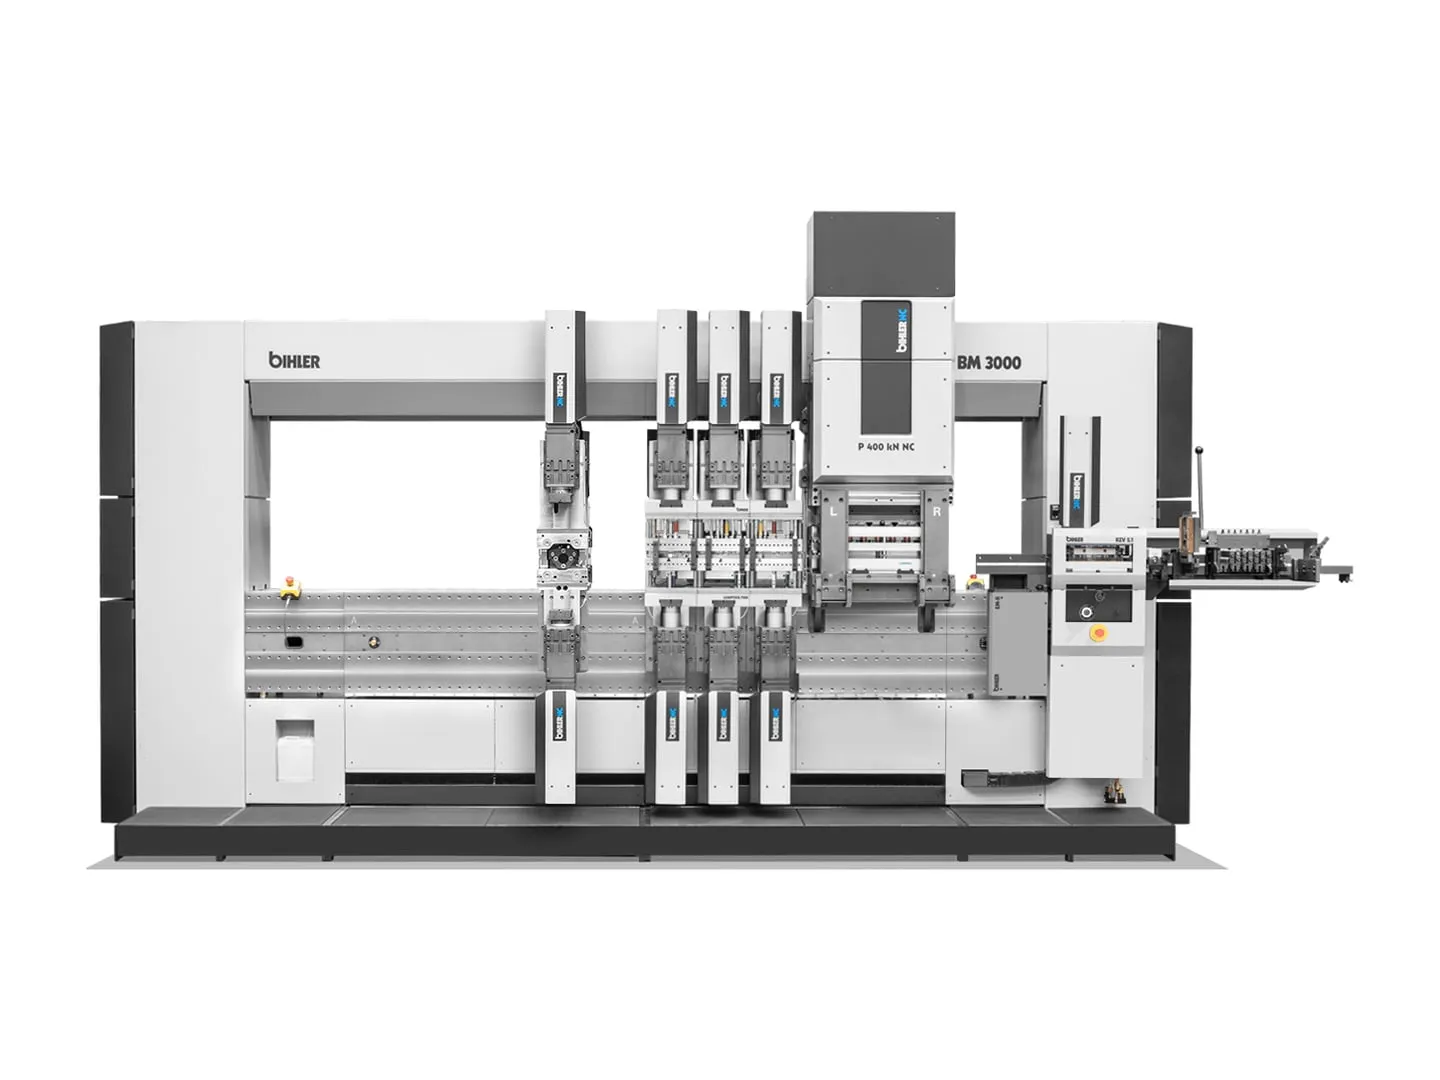
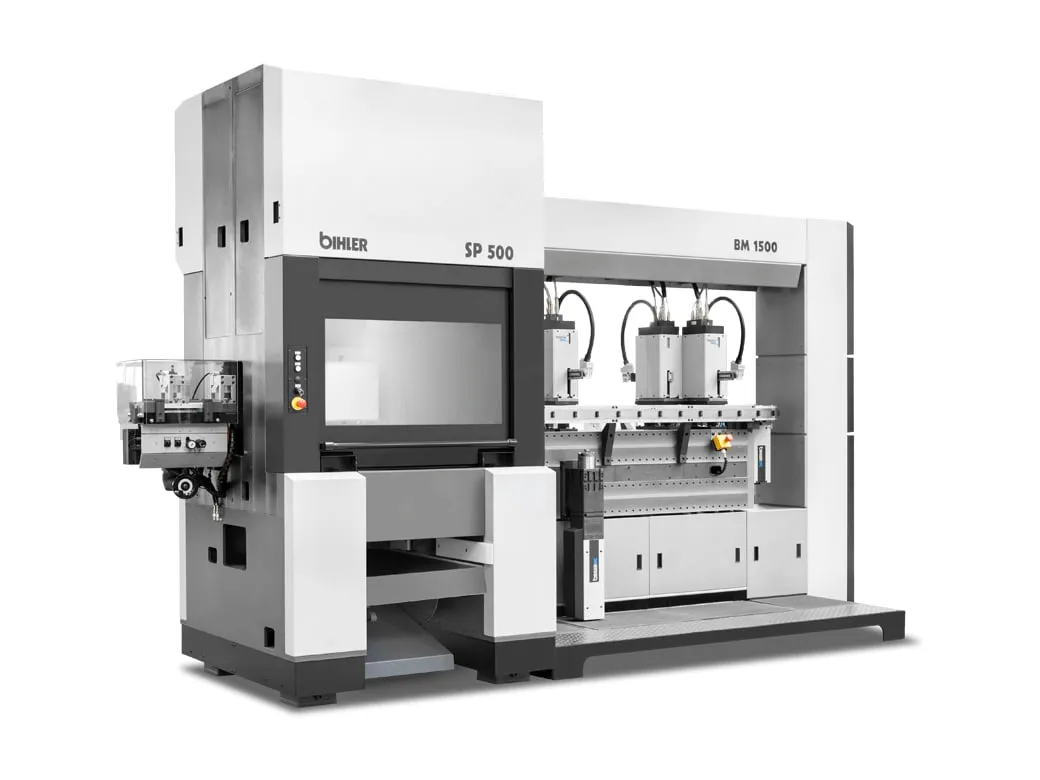
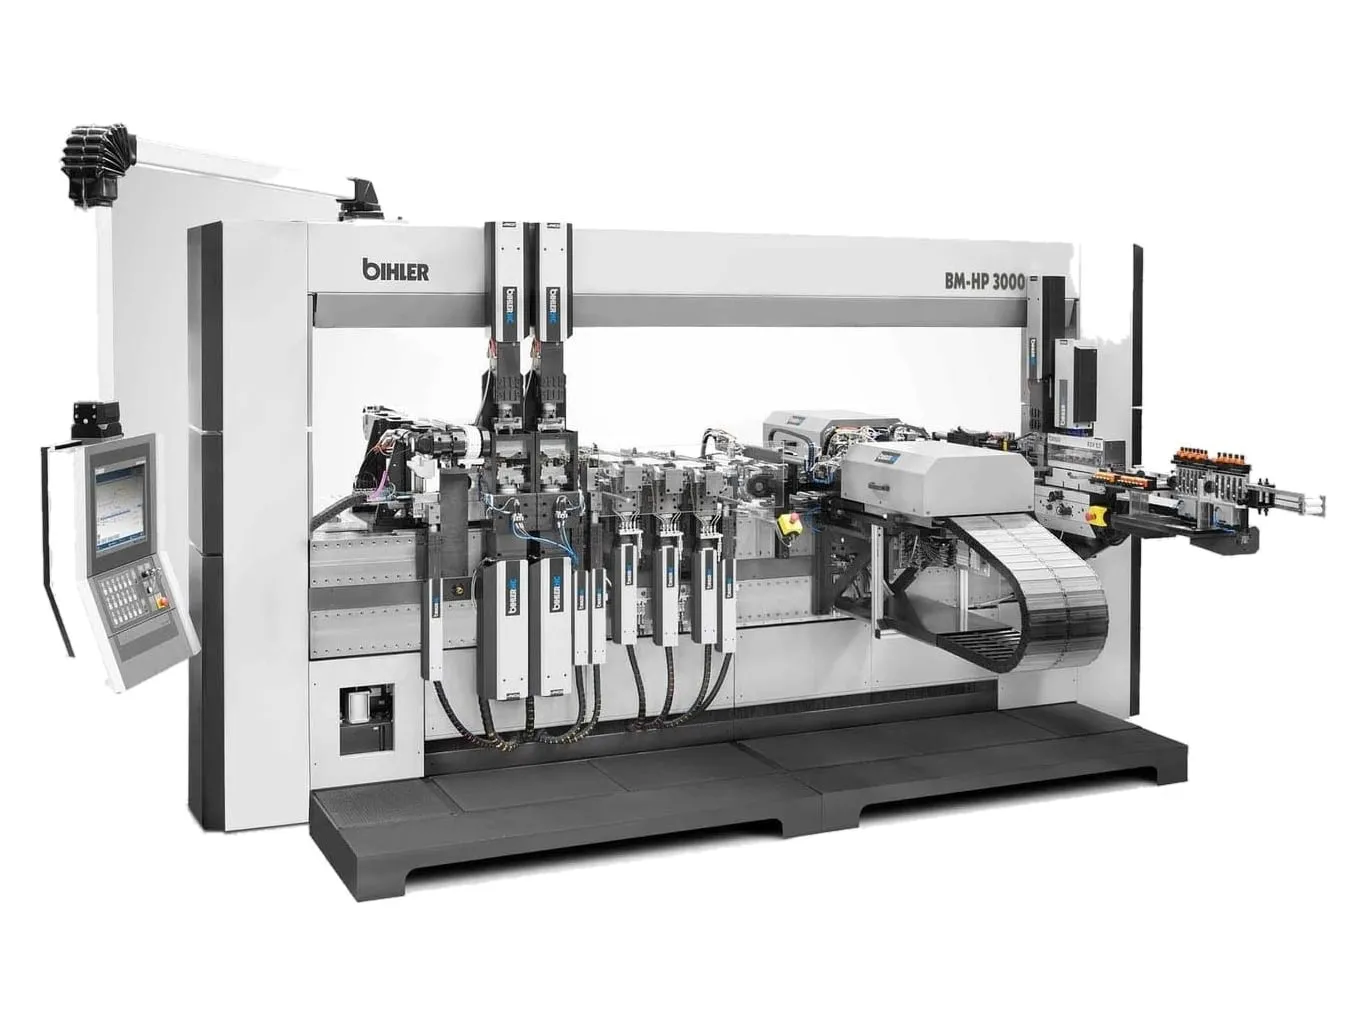
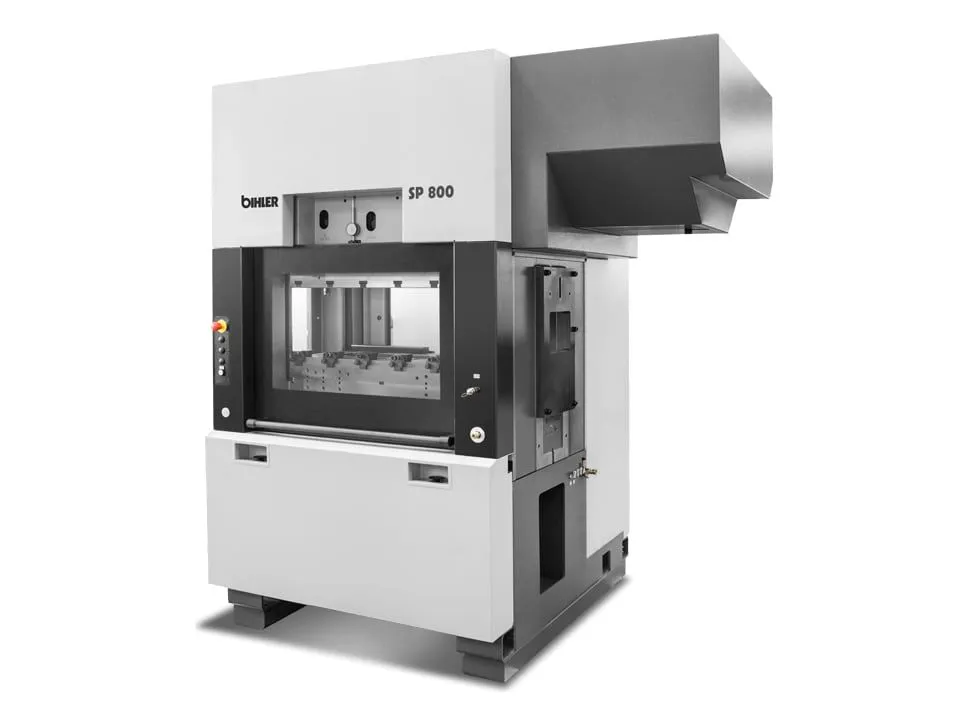
Bihler GRM 80 Bihler GRM 80 Universal multi-slide machine for large stamped and bent parts 250 1/min300–400 kN80 mm Technical data Bihler RM 40 Bihler RM 40 Compact multi-slide machines for mass production of small precision stamped and formed parts 350 1/min90–200 kN60 mm Technical data Bihler RM 30K Bihler RM 30K Compact multi-slide machine for mass production of small stamped and formed metal parts 350 1/min90 kN900 mm Technical data Bihler GRM-NC Bihler GRM-NC Universal servo multi-slide machine for small and medium batches 250 1/min400 kN90 mm Technical data Bihler RM-NC Bihler RM-NC Servo multi-slide machine for small and medium batches with radial tooling 300 1/min200 kN80 mm Technical data Bihler BNC 4 Bihler BNC 4 Servo multi-slide production system compatible with MRP tooling 300 1/min200 kN31 kN Technical data Bihler BIMERIC BM Bihler BIMERIC BM Modular servo production and assembly system from raw material to ready-to-install assemblies 250 1/min400 kN80 mm Technical data Bihler BIMERIC SP Bihler BIMERIC SP Sub-assembly production system combining a servo press with the BIMERIC platform for progressive dies 250 1/min500 kN15–63 mm Technical data Bihler BM-HP 3000 Bihler BM-HP 3000 Servo system producing complete electric-motor hairpins from flat wire on the coil 60–120/min3.2 m/s±0.02 mm Technical data Bihler SP 800 Bihler SP 800 800 kN servo press for progressive tools; stand-alone or combined with the BIMERIC 800 kN200 1/min30 mm Technical data Bihler RM S Bihler RM S High-speed multi-slide machine for stamped and formed parts made from high-tensile steels 600 1/min150 kN900 mm Technical data Bihler GRM 80B Bihler GRM 80B Bushing machine with a standardised tooling concept for mass production of straight and flanged bushings 220 1/min160 1/min15–40 mm Technical data Bihler MC 42 Bihler MC 42 Multi-slide machine with two processing faces for small stamped and formed parts and sub-assemblies 350 1/min90 kN60 kN Technical data Bihler MC 82 Bihler MC 82 Multi-slide machine with two processing faces for larger stamped and formed parts and sub-assemblies 250 1/min300 kN90 kN Technical data Bihler MC 120 Bihler MC 120 Multi-slide machine with a 700 kN press and two processing faces for large stamped and formed parts and sub-assemblies 150 1/min700 kN160 kN Technical data Bihler MCS 1 Bihler MCS 1 High-speed multi-slide machine with two processing faces, running at up to 800 strokes per minute 800 1/min70 kN30 kN Technical data Bihler MCS 05 Bihler MCS 05 High-speed multi-slide machine with two processing faces for large stamped and formed parts and sub-assemblies 500 1/min300 kN50 kN Technical data Bihler BZ2-S8 Bihler BZ2-S8 High-performance processing centre driven by servo motors for mass production of stamped and formed parts and sub-assemblies 700 1/min300 kN50 kN Technical data Bihler CC 1 Bihler CC 1 COMBITEC processing centre with a separate 800 kN press module for long, bulky stamped and formed parts and sub-assemblies 200 1/min800 kN160 kN Technical data

Catalogue

We will e-mail you the catalogue

Enter your details and we will send the download link to your e-mail address straight away.

Your details are used only to send this catalogue and to contact you about your request. KVKK Notice