Standardised process modules
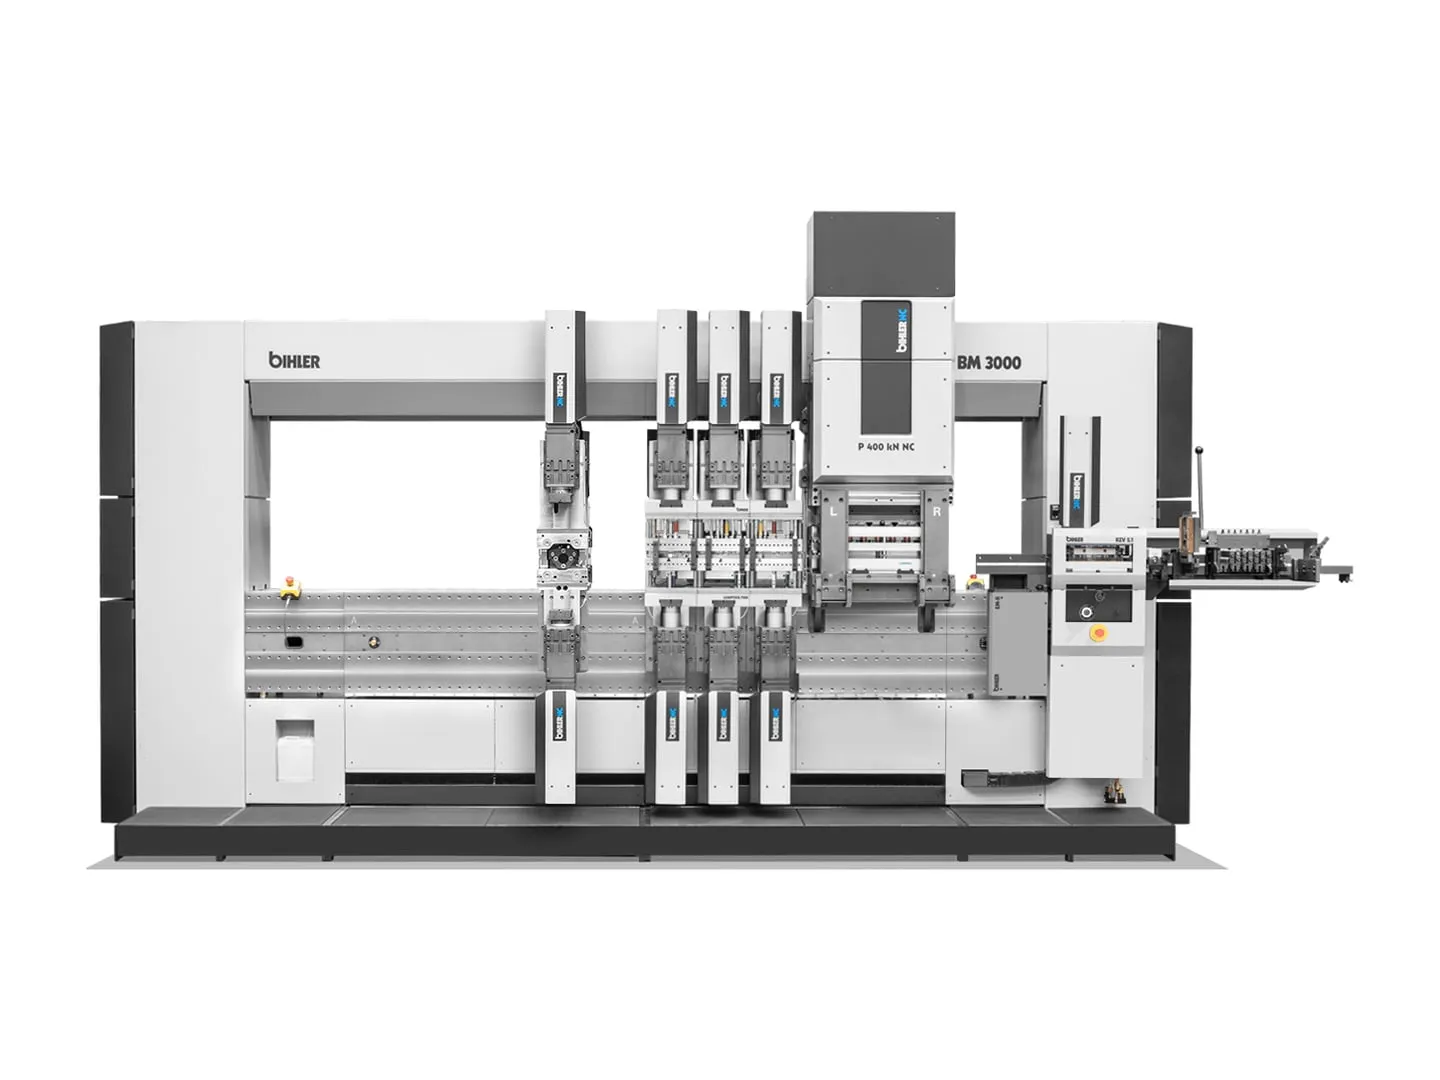
Feeding module EM-R (RZV 2.1, 2,000 mm), stamping module PM400 (400 kN spindle press, Meusburger SBP / SBH 400, 750 mm) and forming module BM-L250 (31 kN NC slide pairs, LEANTOOL L250); all designed for 80 mm strip.
Since 198343 years serving Turkish industry
Servo production and assembly systems
Modular servo production and assembly system from raw material to ready-to-install assemblies
ⓘ Manufacturer data: BIMERIC Modular product page and brochure (11/24), BIMERIC BM brochure (05/17), Bihler application examples (b on top / b. Values may change and vary; not binding on Boztaş.
Feeding module EM-R (RZV 2.1, 2,000 mm), stamping module PM400 (400 kN spindle press, Meusburger SBP / SBH 400, 750 mm) and forming module BM-L250 (31 kN NC slide pairs, LEANTOOL L250); all designed for 80 mm strip.
For servo process modules such as contact welding, thread forming (GSE K/KS), screw insertion (MSE 2), pick & place, lift-rotate (HDE), conveyor belt and insulation stripping; the system can be extended later.
1,500 mm machine base blocks combine up to 6,000 mm; linear tools are shared with the GRM-NC, LM 2000-KT and LM 2000-NC (Modular Series).
Pre-assembled EM-R / PM400 / BM-L250 modules, 400 kN spindle press (stroke 4–60 mm), NCA-5 31 kN; zero-point hydraulic tool clamping; 24" multi-touch VC 1; base up to 6,000 mm
Suited to: Multi-variant component and assembly production
Manufacturer application: worm-gear hose clamps of 8–120 mm diameter, 100 fully assembled clamps per minute, set-up under 30 minutes
Suited to: Compact assembly cell
Manufacturer applications: contact component 80/min, spool carrier 40/min, short-stroke pushbutton 240/min, sintered plain bearing bush 80/min, ring-shaped contact lamella 100/min; tool change between different assemblies within half an hour
Suited to: Production with frequently changing assemblies
Manufacturer applications: hydraulic valve connector in 16 variants at 80/min (variant change under 30 min), head restraint tubes at 40/min (44 NC axes), circuit breaker thermal assembly at 120/min, 48 V power connector in approx. 100 steps
Suited to: Complex hybrid assemblies with many process steps
Manufacturer applications: watertight electric motor housings (approx. 30 % less material than deep drawing), production of power sockets, battery cell connectors in carrier frames
Suited to: Complete products with long process chains
| Feature | BIMERIC Modular | BIMERIC BM (brochure 05/17) |
|---|---|---|
| Performance | ||
| Cycle rate | max. 250 1/min (depending on the application) | max. 250 1/min (depending on the application) |
| Drive | Completely servo-controlled | Fully NC |
| Press | NC spindle press max. 400 kN, stroke 4–60 mm (PM400) | NC two-point eccentric presses: 150 kN / 8 mm, 150 kN / 12 mm, 200 kN / 12 mm, 300 kN / 16 mm |
| Servo press option | — | SP 500: 500 kN, 400 1/min, stroke 15–63 mm, stroke position 0–60 mm, plate 1,000 × 560 mm |
| NC units | NCA-5: max. 31 kN, stroke max. 100 mm | NCA-2 0.4 / 0.8 kN; NCA-3 2.5 / 5 kN; NCA-4 10 / 15 kN; NCA-5 40 kN |
| Tool area and feed | ||
| Feed | RZV 2.1 NC radial gripper feed; positioning ±0.02 mm | RZV 2.1 NC radial gripper feed; feed length from zero to infinity |
| Tooling system | LEANTOOL L250 linear tools; Meusburger SBP / SBH 400 cutting frames; zero-point hydraulic clamping | Modular linear tools; quick-change systems |
| Assembly line | Workpiece carrier spacing 100 / 150 / 200 mm | Workpiece carrier spacing 100 / 150 / 200 mm (special up to 450 mm); positioning ±0.10 mm |
| Upper edge of material | — | 1,230 mm above the floor |
| Material | ||
| Strip / wire | strip max. 4 mm / 80 mm; wire max. Ø 4 mm | — |
| Control | ||
| Control | VariControl VC 1 (3.0), 24" multi-touch; control cabinet in the housing; OPC UA | VariControl VC 1, separate control cabinet, 15" TFT touch screen |
| Monitoring | Sensors in all machine and processing components (predictive maintenance); press and slide force monitoring optional | Press and slide force monitoring optional |
| Dimensions and weight | ||
| Machine base | Block 1,500 × 500 × 500 mm; combinable up to 6,000 mm | Block 1,500 × 500 × 500 mm; combinable up to 4,500 mm |
| Dimensions / weight | Depending on design | — |
| Equipment | ||
| Protection and supplies | Safety fence, personal protection or sound enclosure; pneumatics, hydraulics, central lubrication (depending on the application) | Safety fence, personal protection or sound enclosure; pneumatics, hydraulics, central lubrication (depending on the application) |
Manufacturer data: BIMERIC Modular product page and brochure (11/24), BIMERIC BM brochure (05/17), Bihler application examples (b on top / b.inside). Application rates are manufacturer examples; depends on material and process.
Technical data is taken from information published by the manufacturer. The manufacturer may change it without notice, and values may vary with the model and the machine configuration. The data is for information only and is not binding on Boztaş; binding values are stated only in a written quotation.
Related industries: AutomotiveHydraulicsElectricalElectronics and ConnectorsDomestic Appliances
The BIMERIC Modular is the current, standardised design of the platform: pre-assembled feeding (EM-R), stamping (PM400, 400 kN) and forming (BM-L250) modules are designed for 80 mm strip, the base extends up to 6,000 mm and linear tools are shared with the Modular Series. The BIMERIC BM brochure dated 05/17 describes 150–300 kN NC eccentric presses, an optional SP 500 servo press and a base of up to 4,500 mm.
The manufacturer positions the GRM-NC for individual stamped and formed parts and the BIMERIC Modular for jobs that add processes such as welding, thread cutting or screw insertion, and assembly, to forming. Linear tools built to the same design guideline can be moved between the two machines.
For a product change usually only the active tool parts are exchanged and the programmed data are recalled from the control. In the manufacturer's applications, a tool change on the BM 3000 takes within half an hour, and set-up on the BM 1500 hose-clamp line and the BM 4500 hydraulic-connector line takes under 30 minutes.
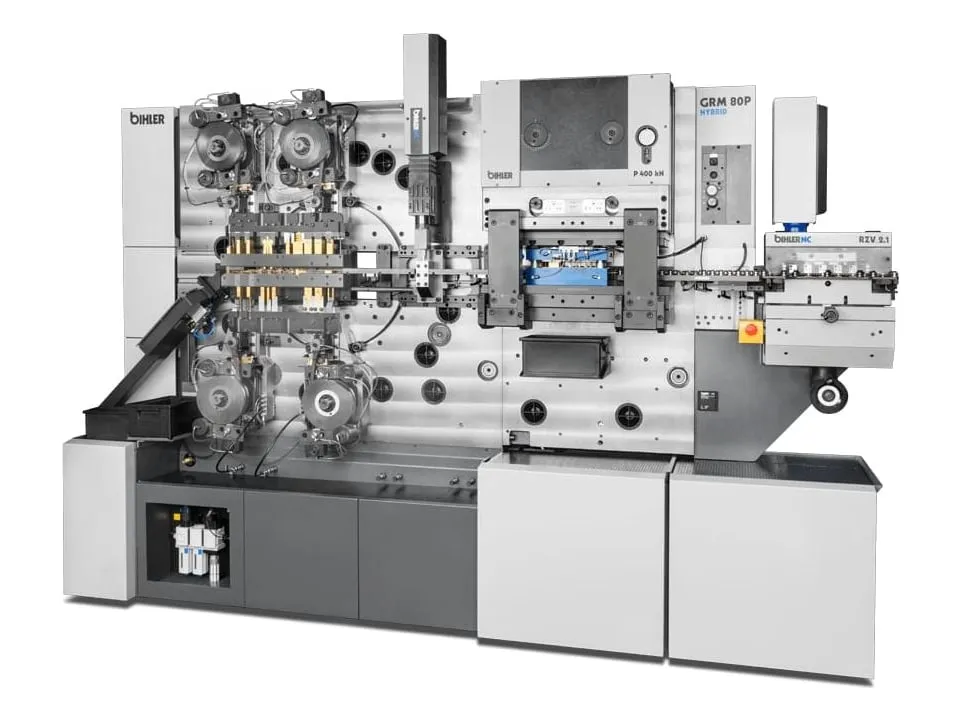 Bihler GRM 80 Universal multi-slide machine for large stamped and bent parts 250 1/min300–400 kN80 mm Technical data
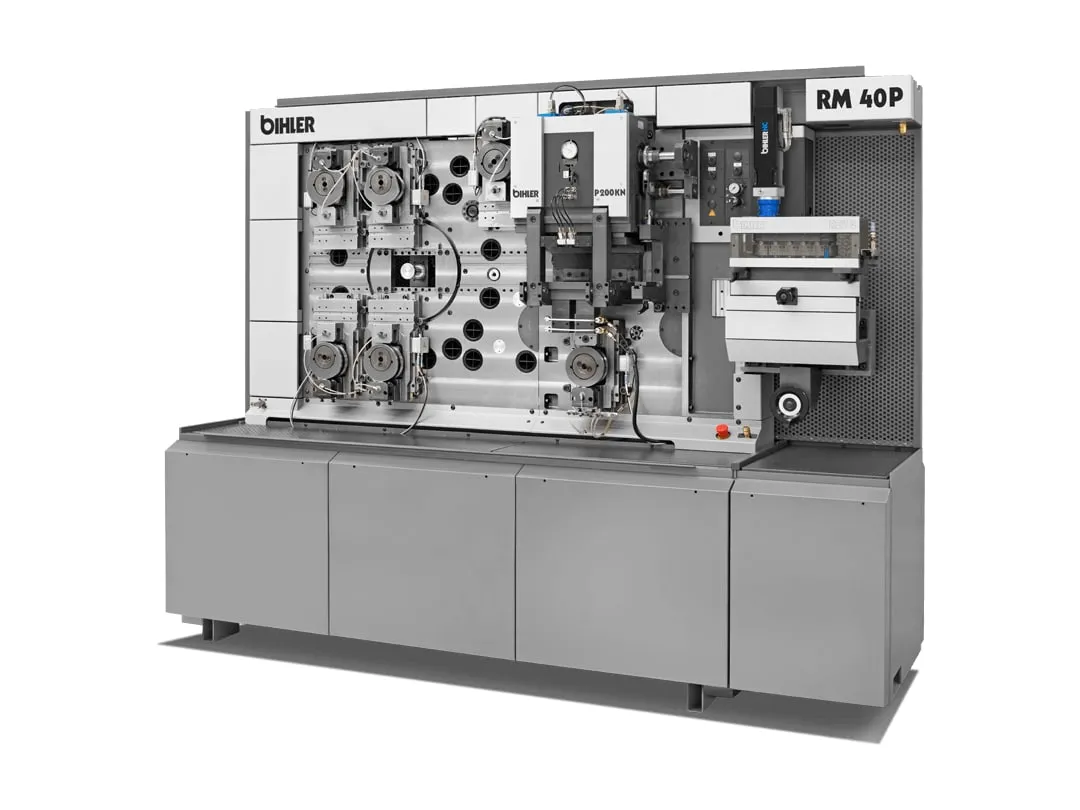 Bihler RM 40 Compact multi-slide machines for mass production of small precision stamped and formed parts 350 1/min90–200 kN60 mm Technical data
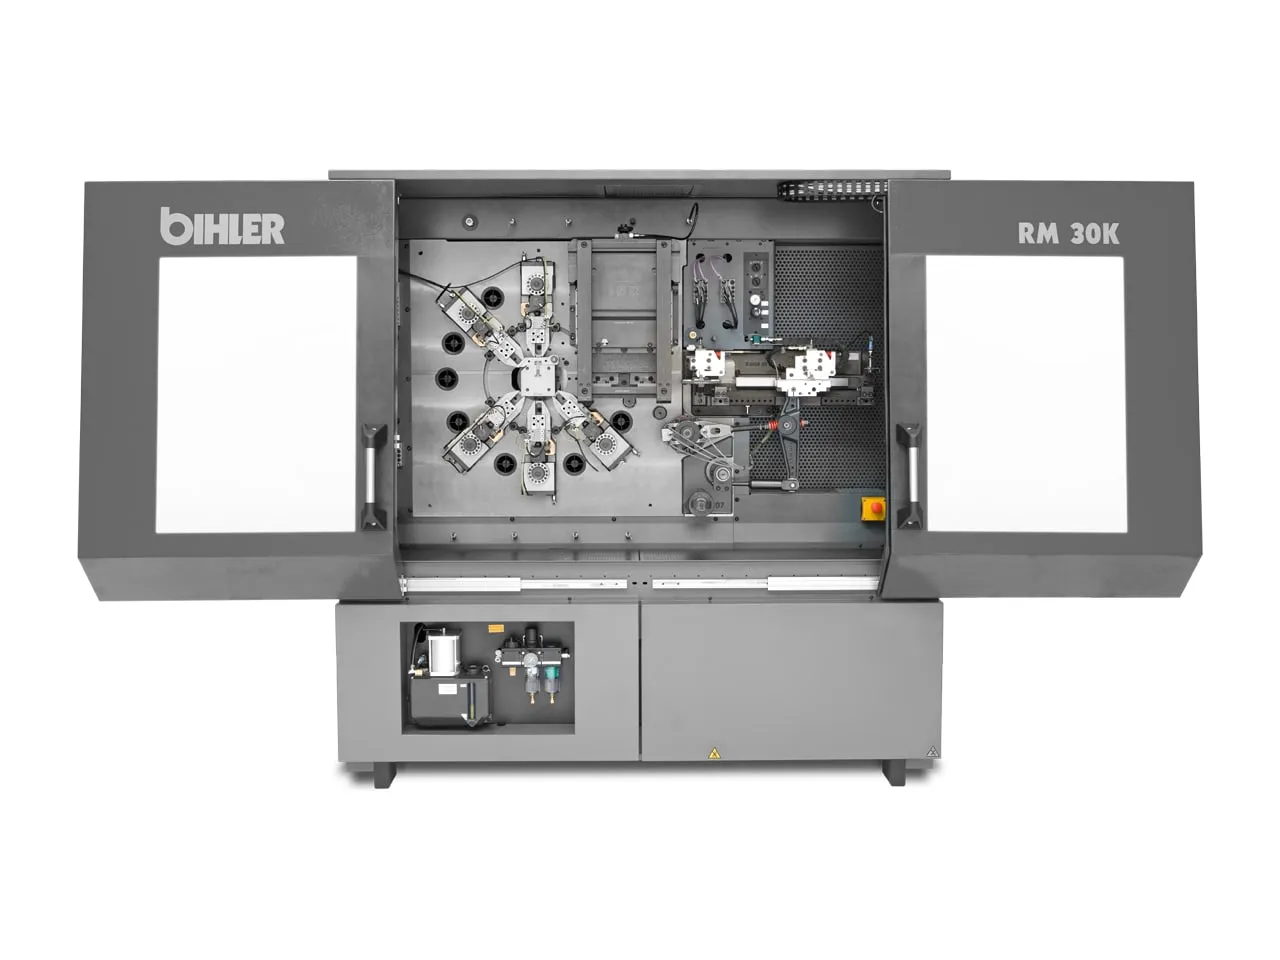 Bihler RM 30K Compact multi-slide machine for mass production of small stamped and formed metal parts 350 1/min90 kN900 mm Technical data
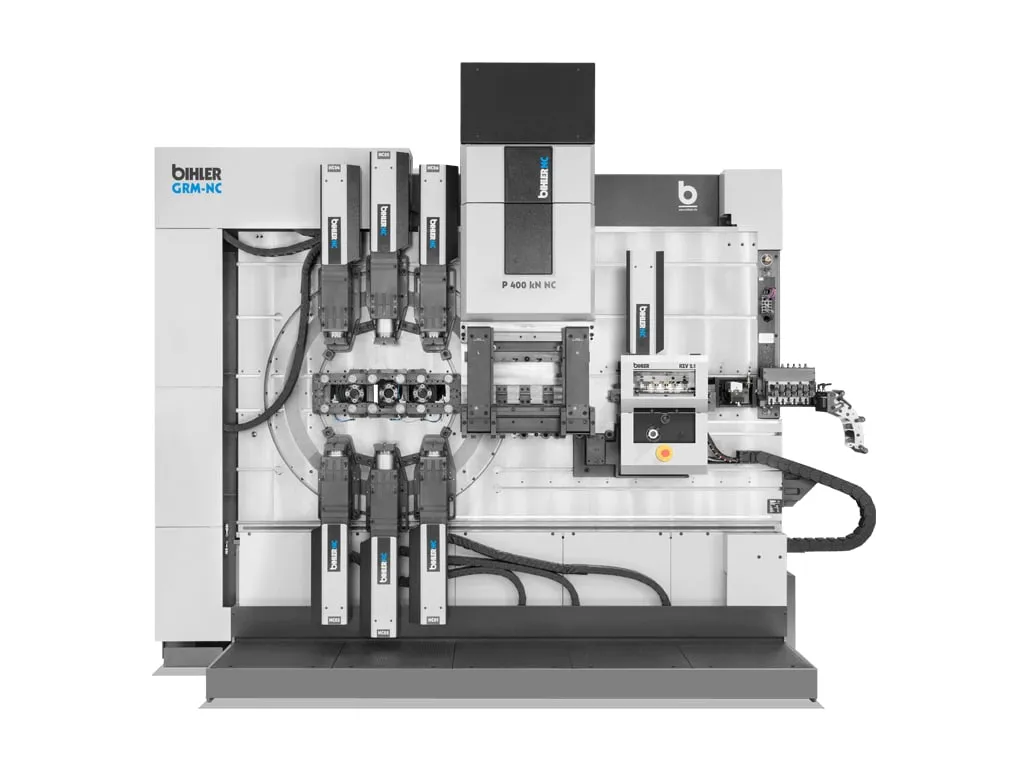 Bihler GRM-NC Universal servo multi-slide machine for small and medium batches 250 1/min400 kN90 mm Technical data
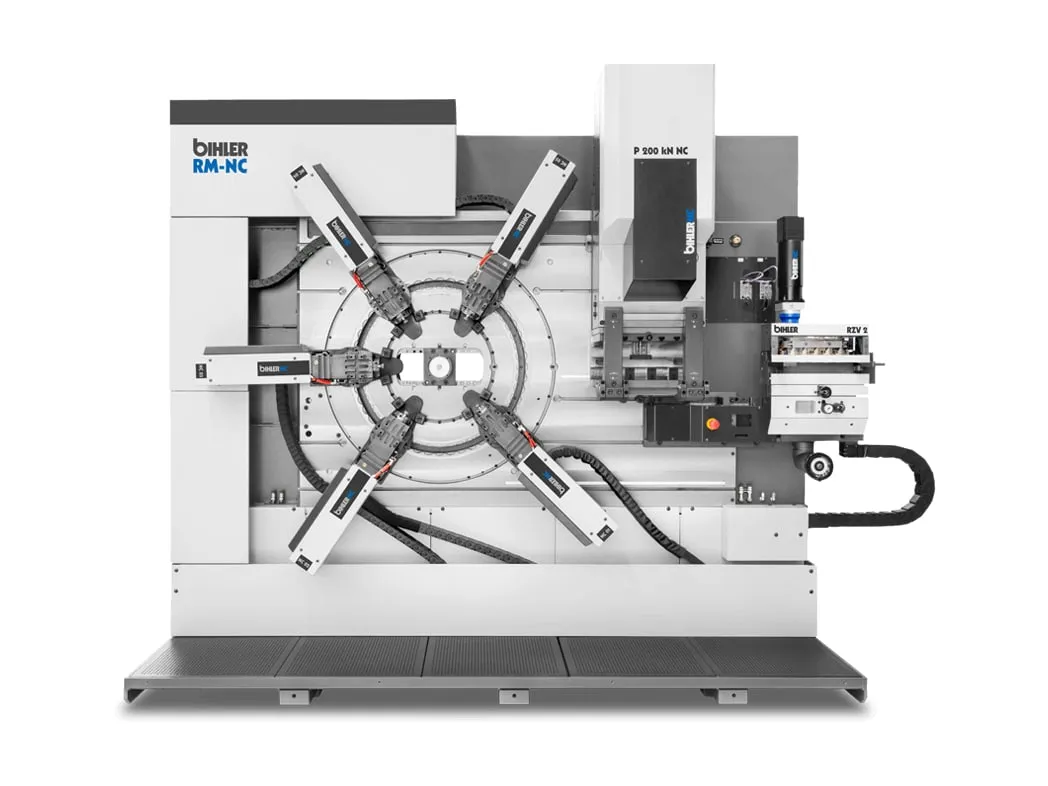 Bihler RM-NC Servo multi-slide machine for small and medium batches with radial tooling 300 1/min200 kN80 mm Technical data
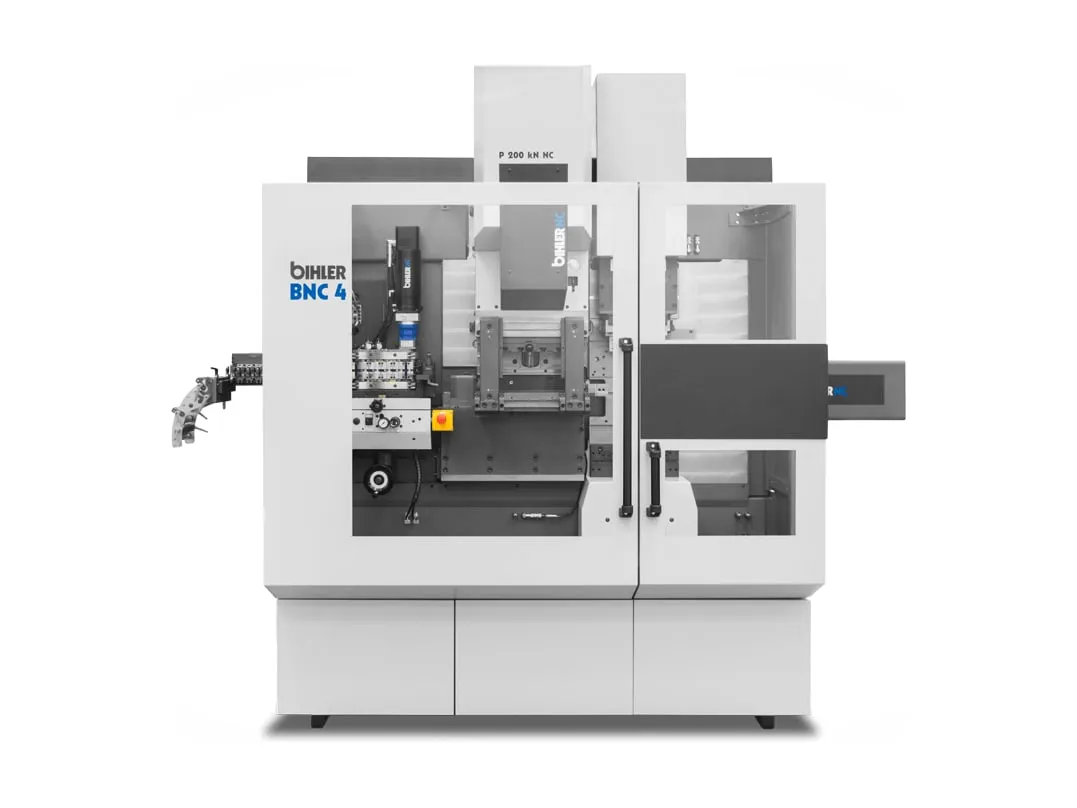 Bihler BNC 4 Servo multi-slide production system compatible with MRP tooling 300 1/min200 kN31 kN Technical data
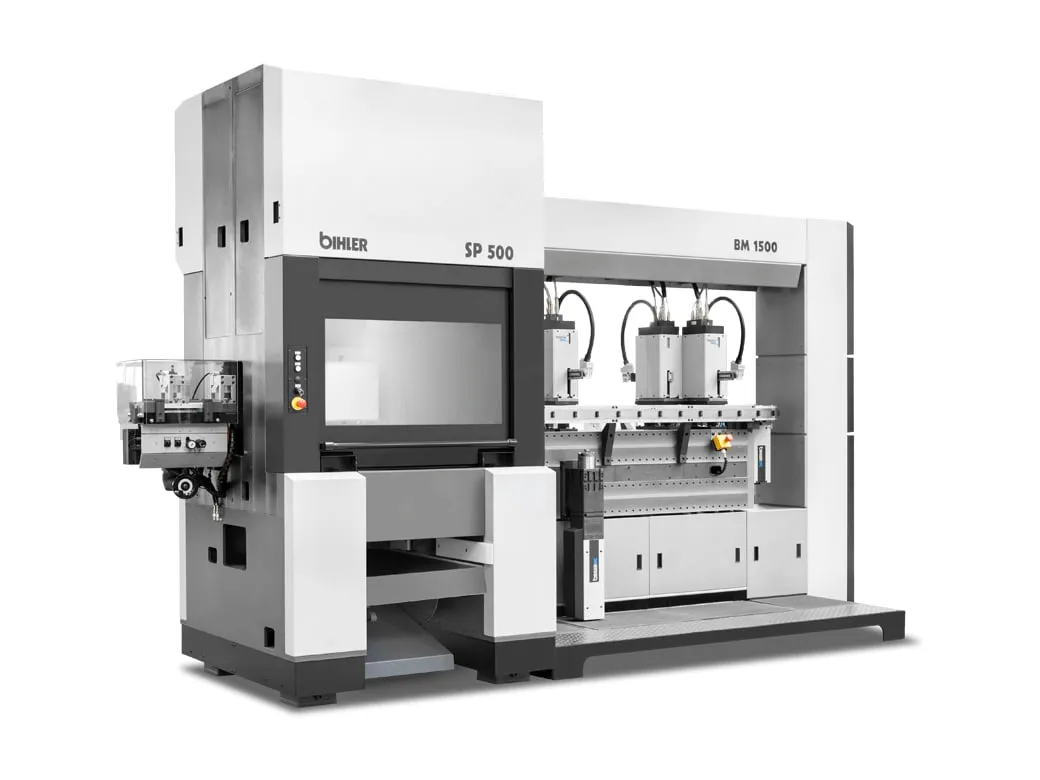 Bihler BIMERIC SP Sub-assembly production system combining a servo press with the BIMERIC platform for progressive dies 250 1/min500 kN15–63 mm Technical data
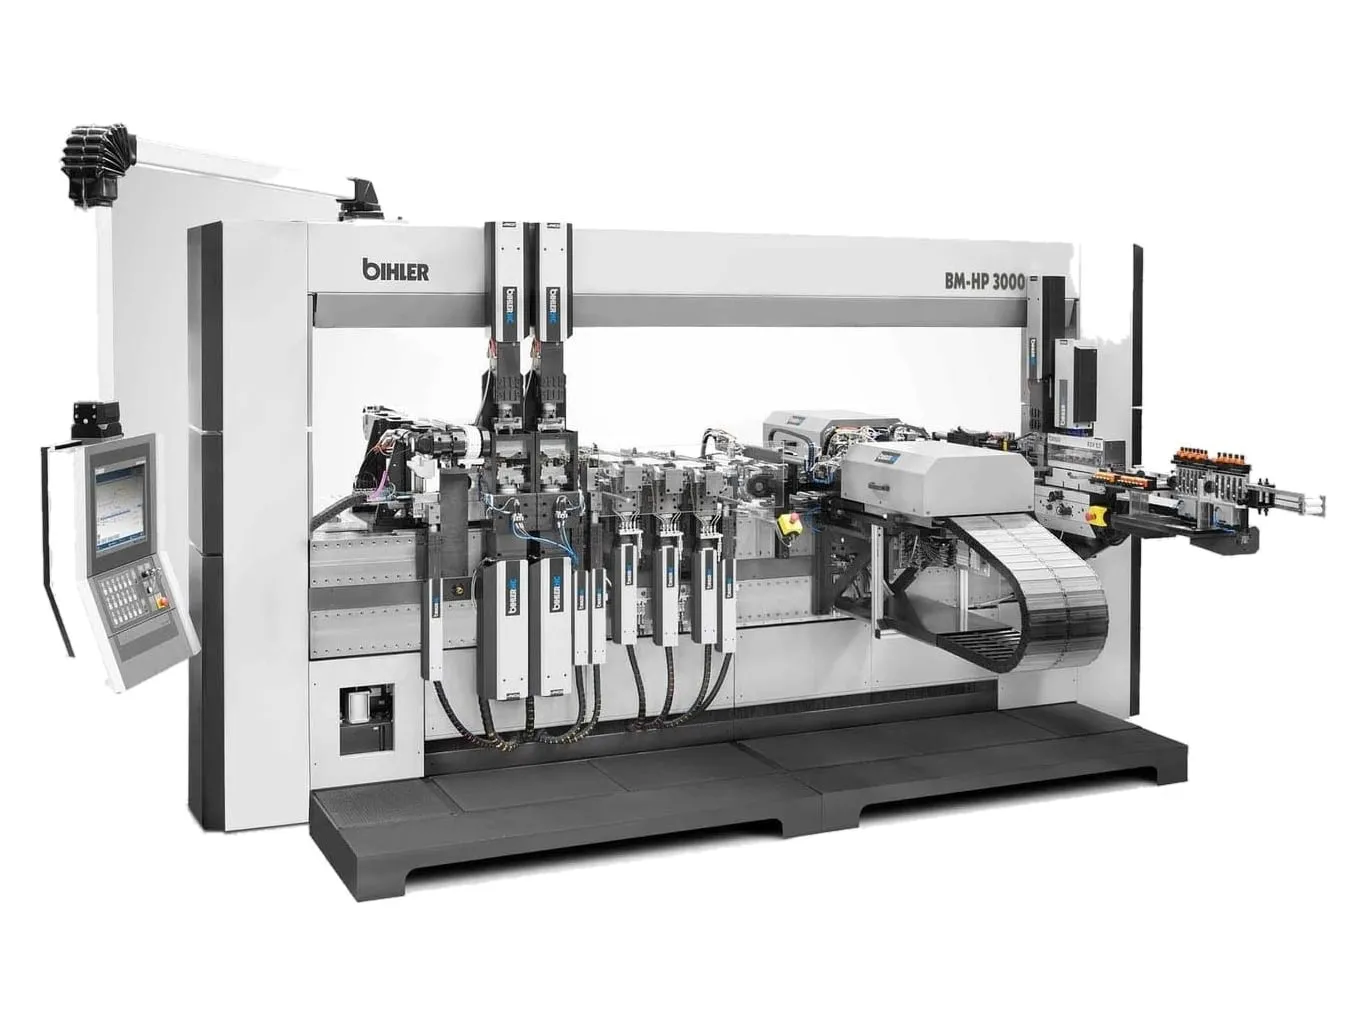 Bihler BM-HP 3000 Servo system producing complete electric-motor hairpins from flat wire on the coil 60–120/min3.2 m/s±0.02 mm Technical data
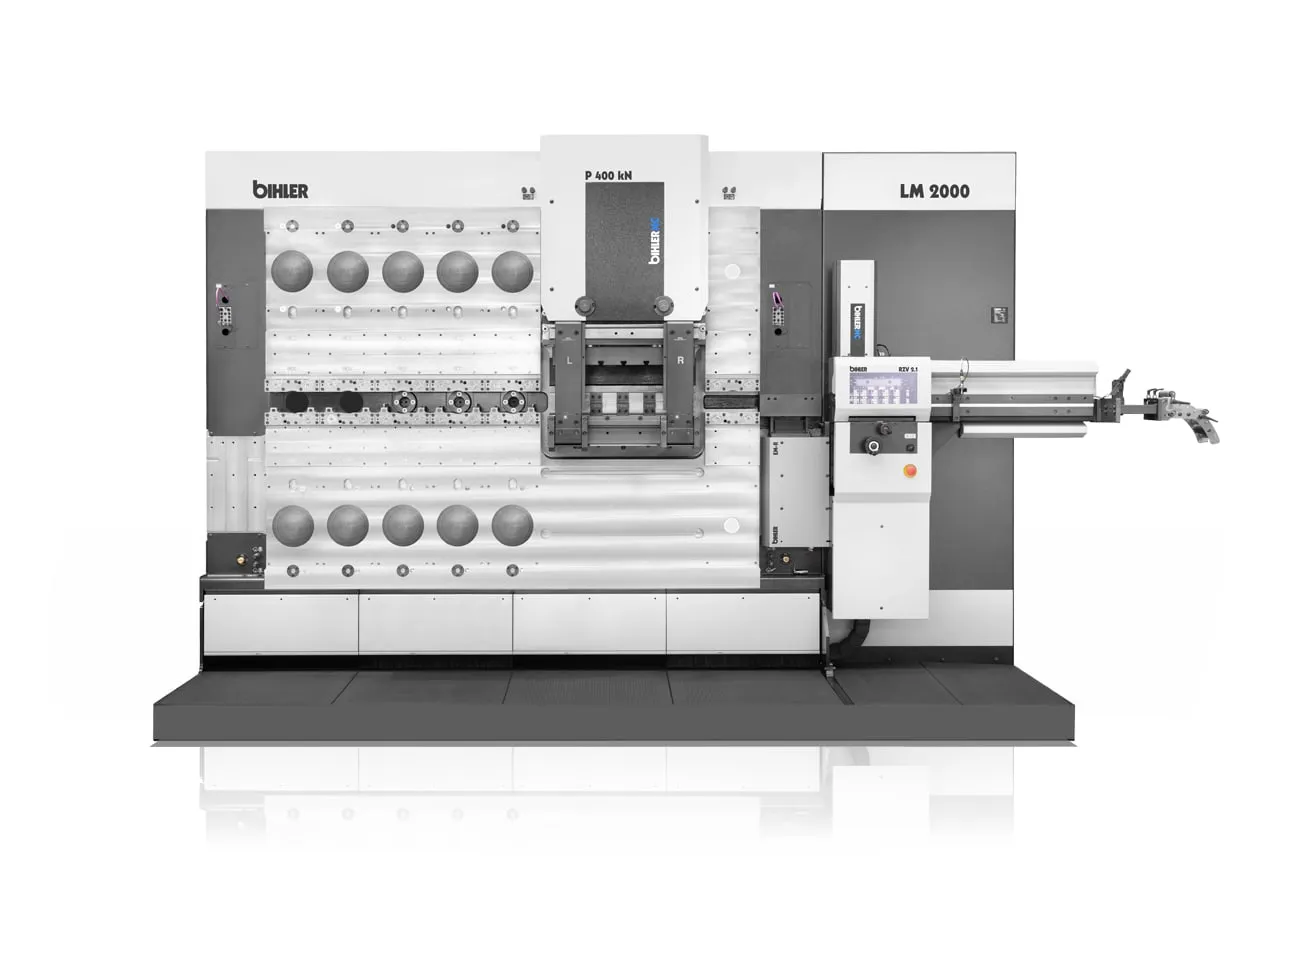 Bihler LM 2000-KT / LM 2000-NC Modular linear machine platform with cam-controlled (KT) or servo-controlled (NC) units 500 1/min250 1/min2,000 mm Technical data
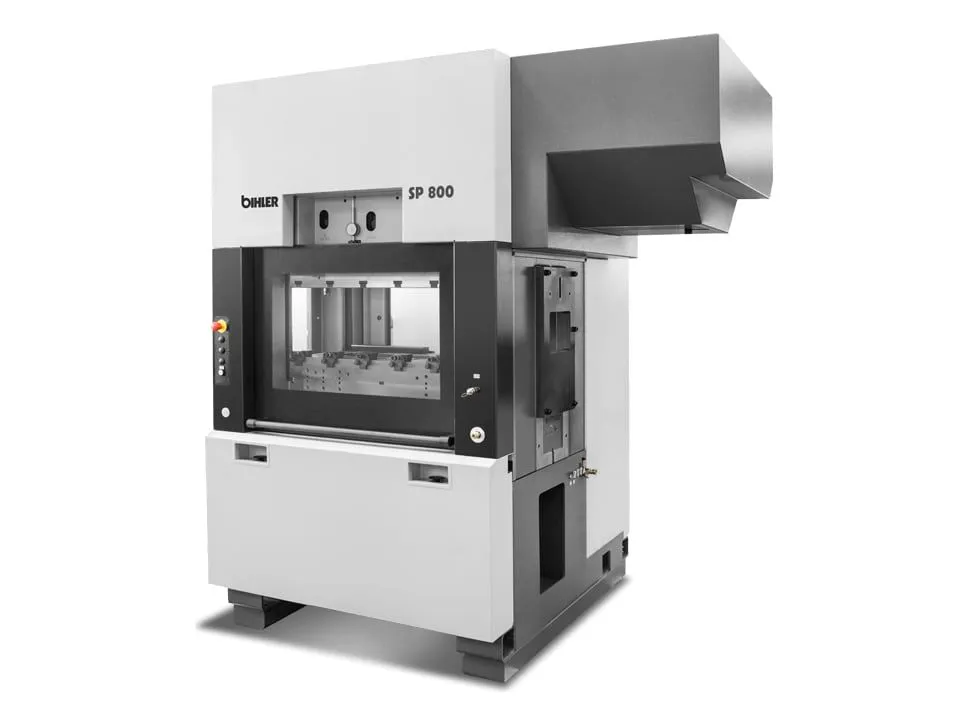 Bihler SP 800 800 kN servo press for progressive tools; stand-alone or combined with the BIMERIC 800 kN200 1/min30 mm Technical data
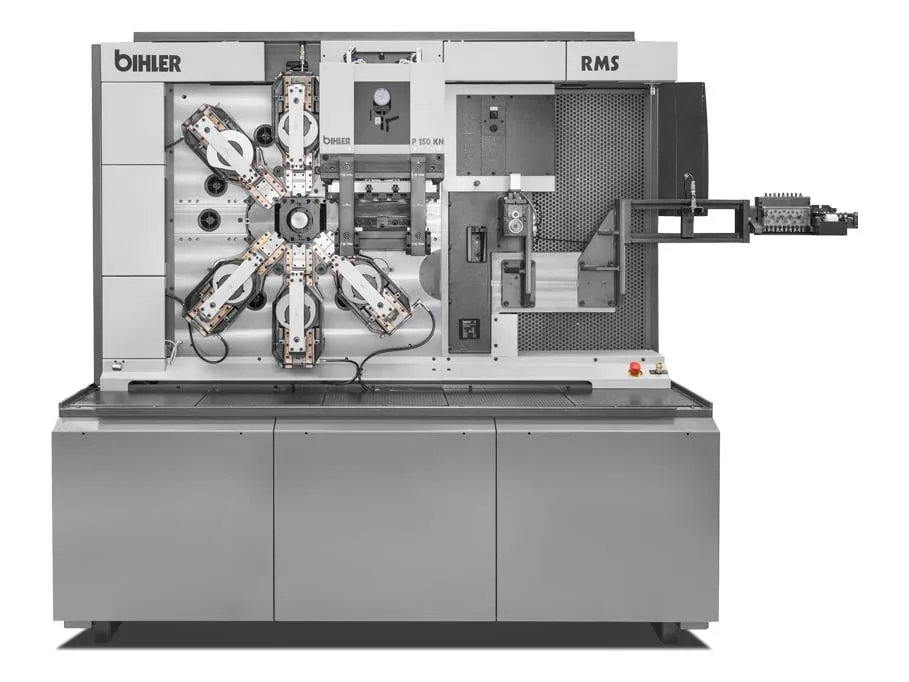 Bihler RM S High-speed multi-slide machine for stamped and formed parts made from high-tensile steels 600 1/min150 kN900 mm Technical data
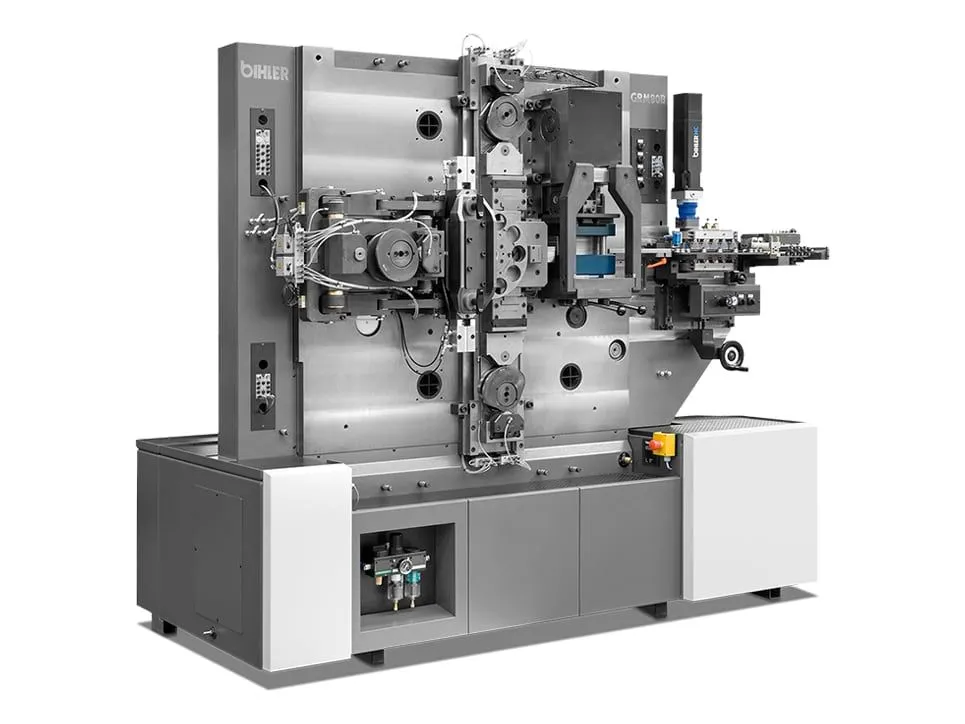 Bihler GRM 80B Bushing machine with a standardised tooling concept for mass production of straight and flanged bushings 220 1/min160 1/min15–40 mm Technical data
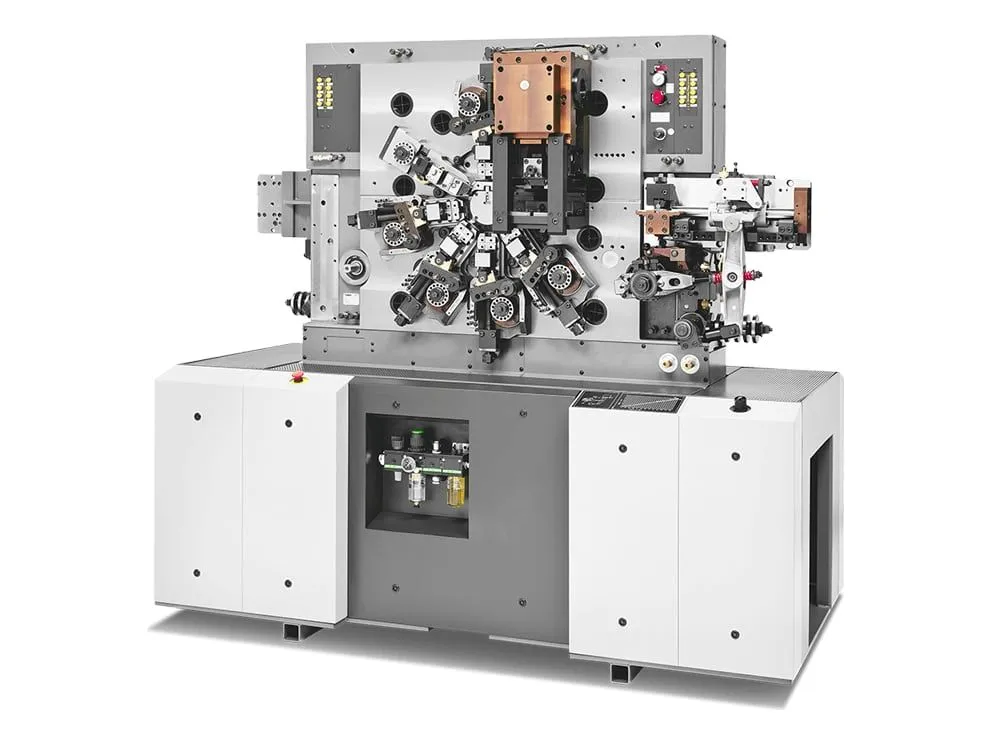 Bihler MC 42 Multi-slide machine with two processing faces for small stamped and formed parts and sub-assemblies 350 1/min90 kN60 kN Technical data
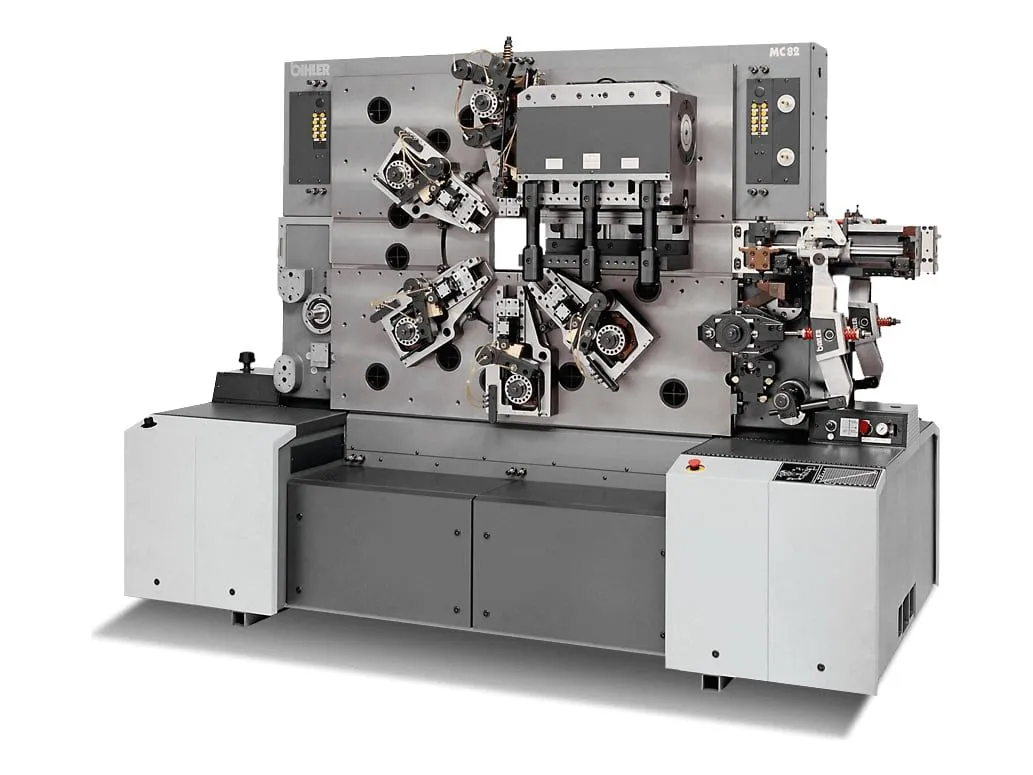 Bihler MC 82 Multi-slide machine with two processing faces for larger stamped and formed parts and sub-assemblies 250 1/min300 kN90 kN Technical data
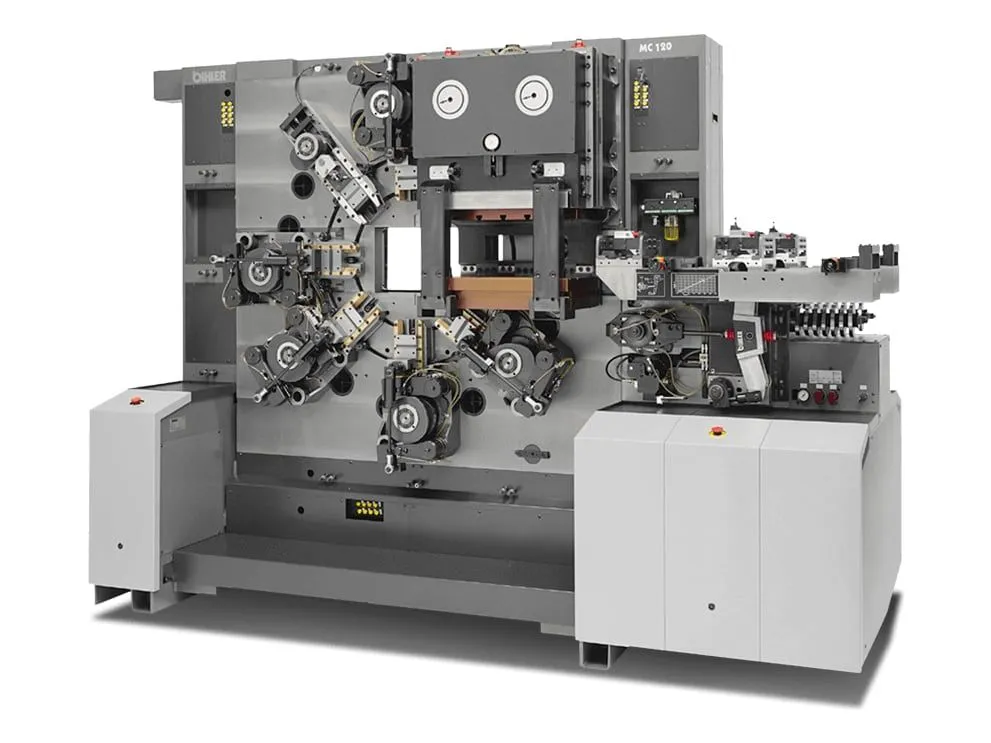 Bihler MC 120 Multi-slide machine with a 700 kN press and two processing faces for large stamped and formed parts and sub-assemblies 150 1/min700 kN160 kN Technical data
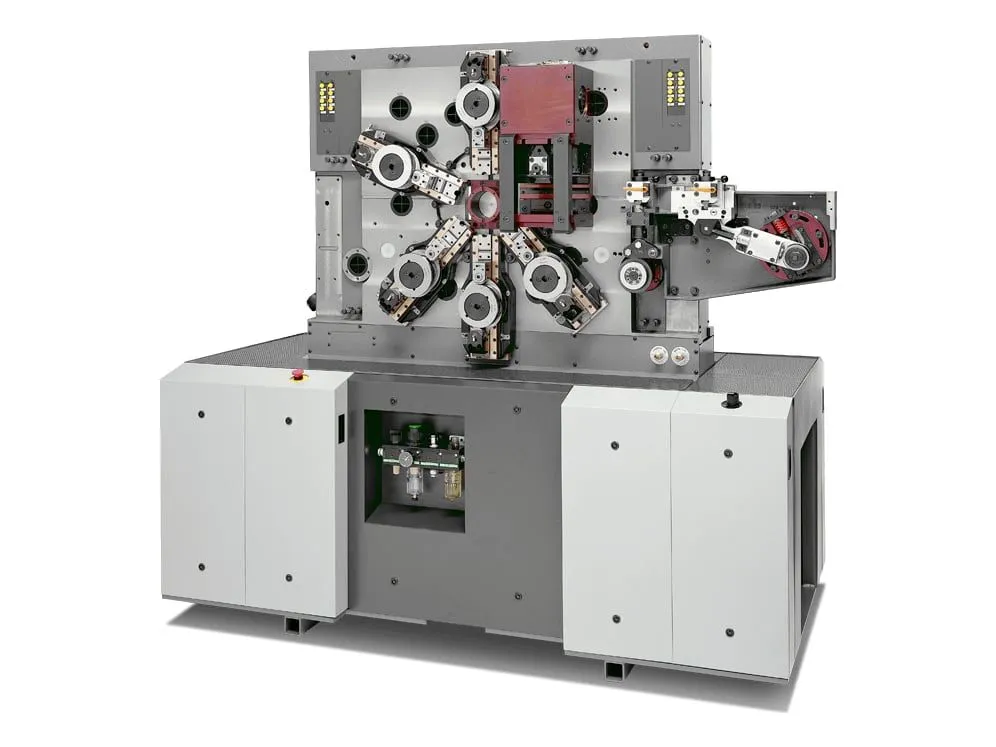 Bihler MCS 1 High-speed multi-slide machine with two processing faces, running at up to 800 strokes per minute 800 1/min70 kN30 kN Technical data
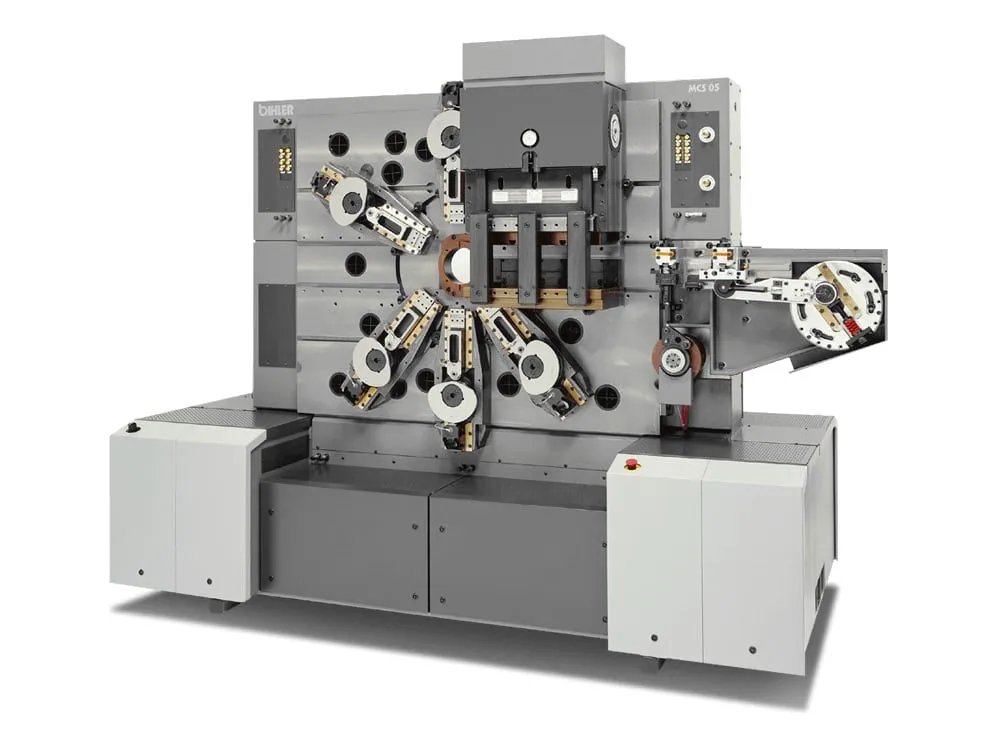 Bihler MCS 05 High-speed multi-slide machine with two processing faces for large stamped and formed parts and sub-assemblies 500 1/min300 kN50 kN Technical data
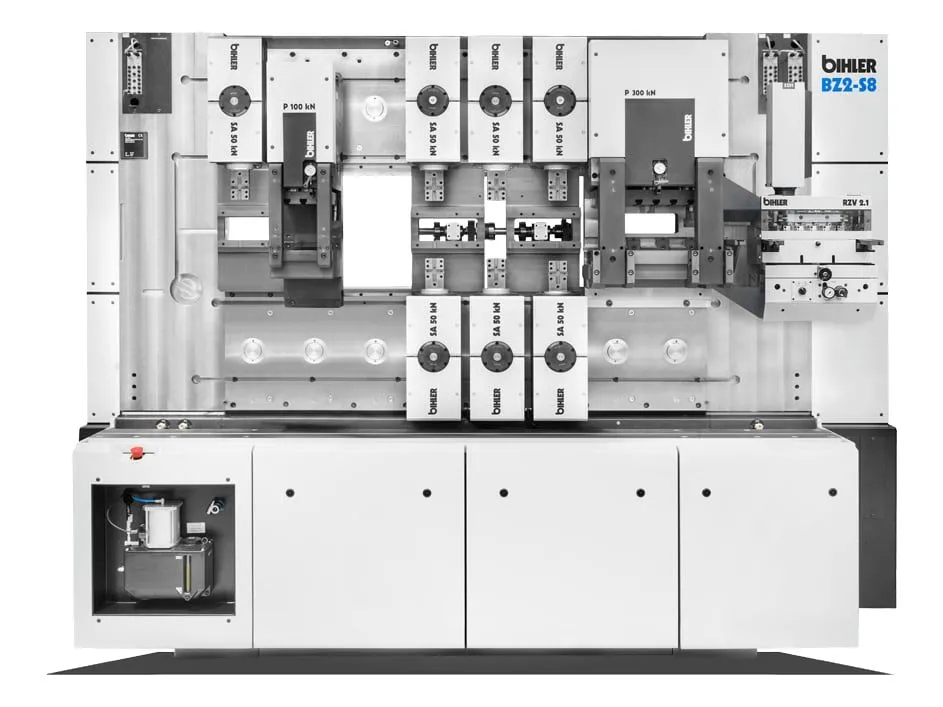 Bihler BZ2-S8 High-performance processing centre driven by servo motors for mass production of stamped and formed parts and sub-assemblies 700 1/min300 kN50 kN Technical data
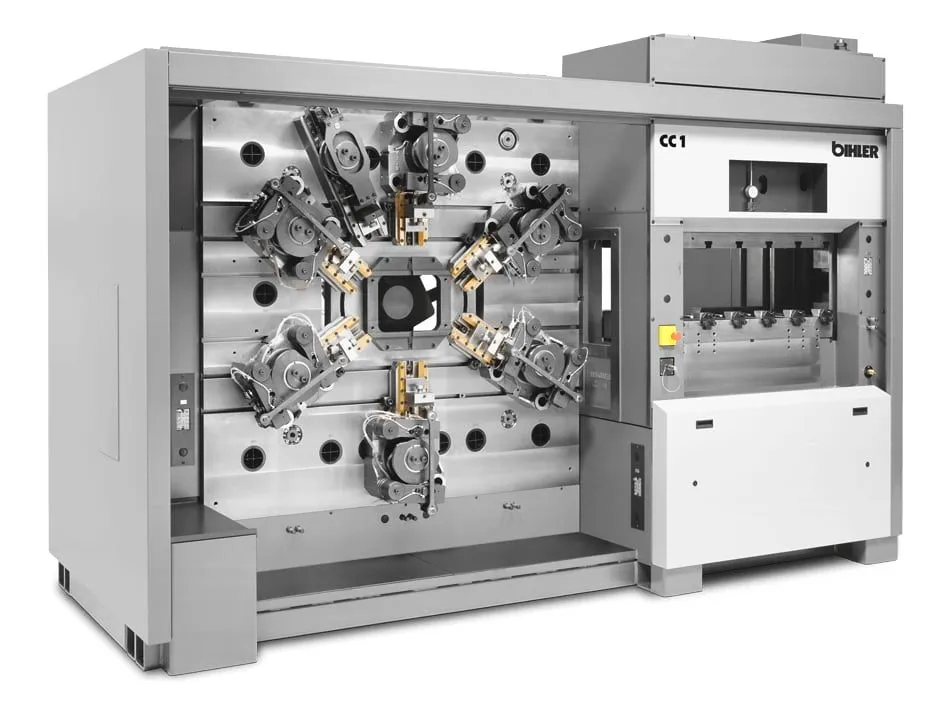 Bihler CC 1 COMBITEC processing centre with a separate 800 kN press module for long, bulky stamped and formed parts and sub-assemblies 200 1/min800 kN160 kN Technical data