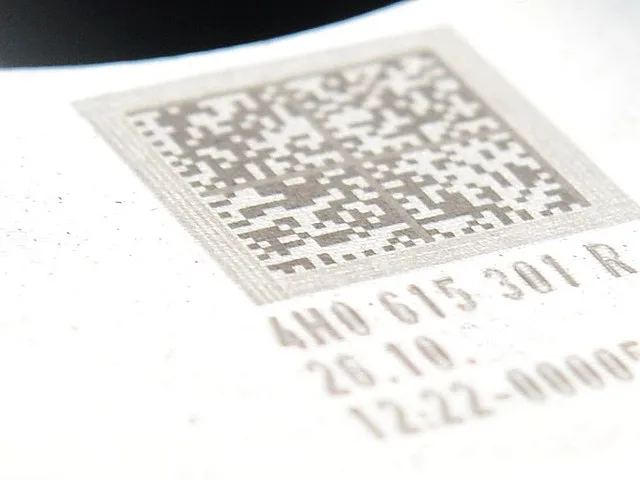
Press lines, deep hole drilling, lathes, multi-slide and marking systems for the automotive and supplier industry; references at TOFAŞ, Ford Otosan, Renault, Mercedes-Benz, ZF and Bosch plants.
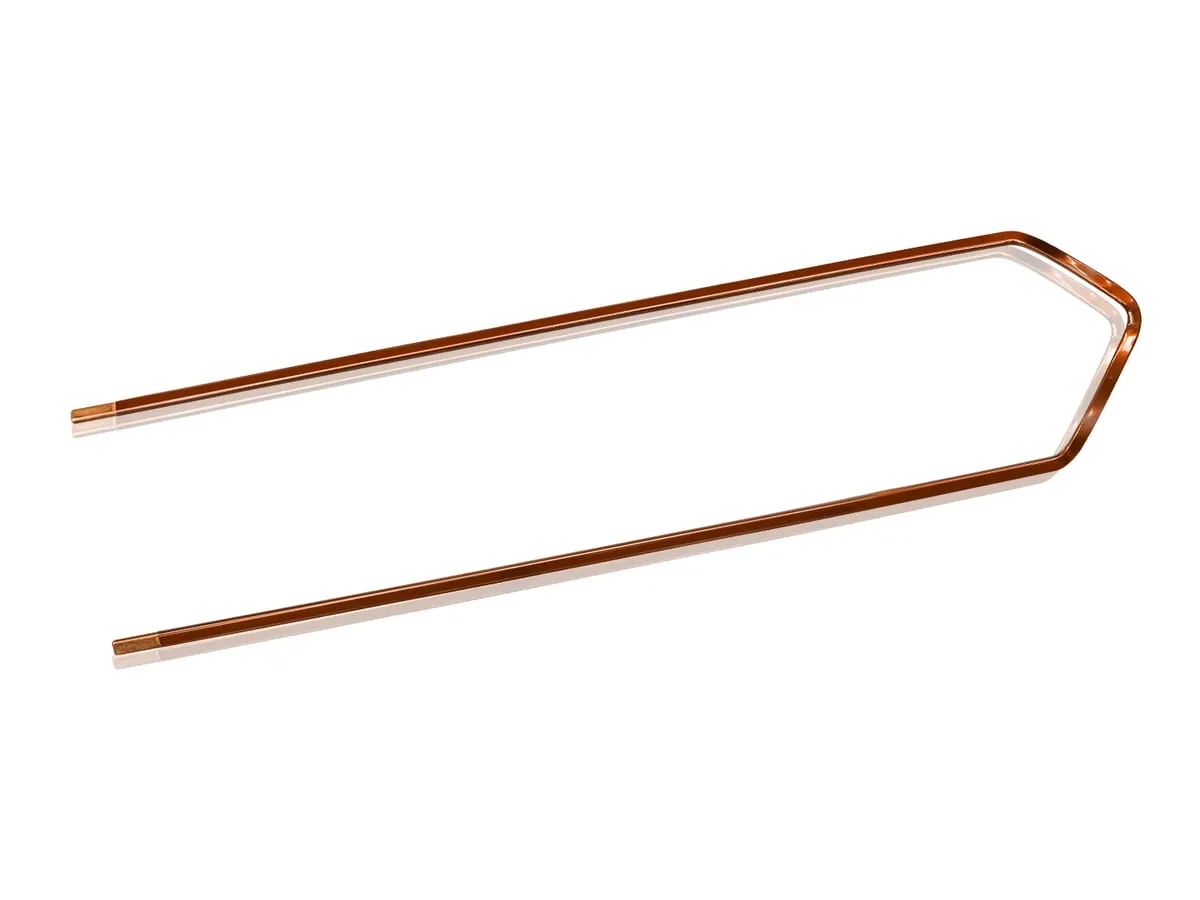
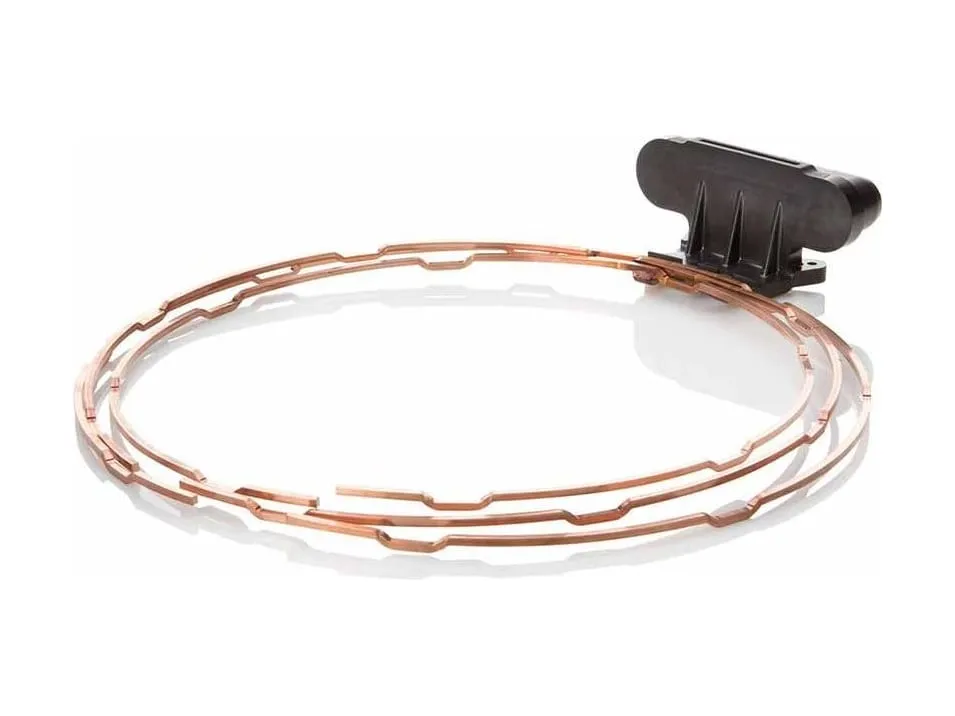
Winding elements for electric motor stators. Straightening, feeding, cutting, enamel stripping, 2D pre-bending and 3D bending of flat wire in one line; 60–120 hairpins per minute, type change on the fly.
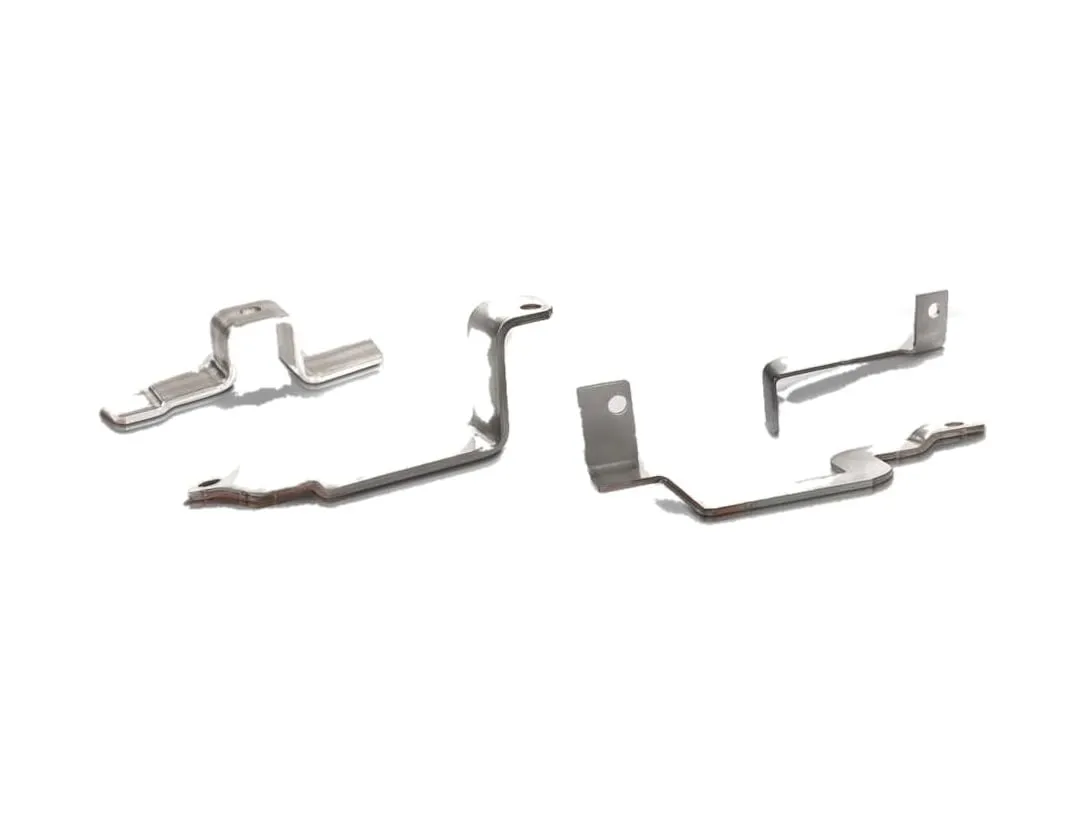
Current-carrying copper and aluminium busbars for e-mobility, up to 4 mm thick. In radial production the strip is as wide as the part, saving up to 50% material.
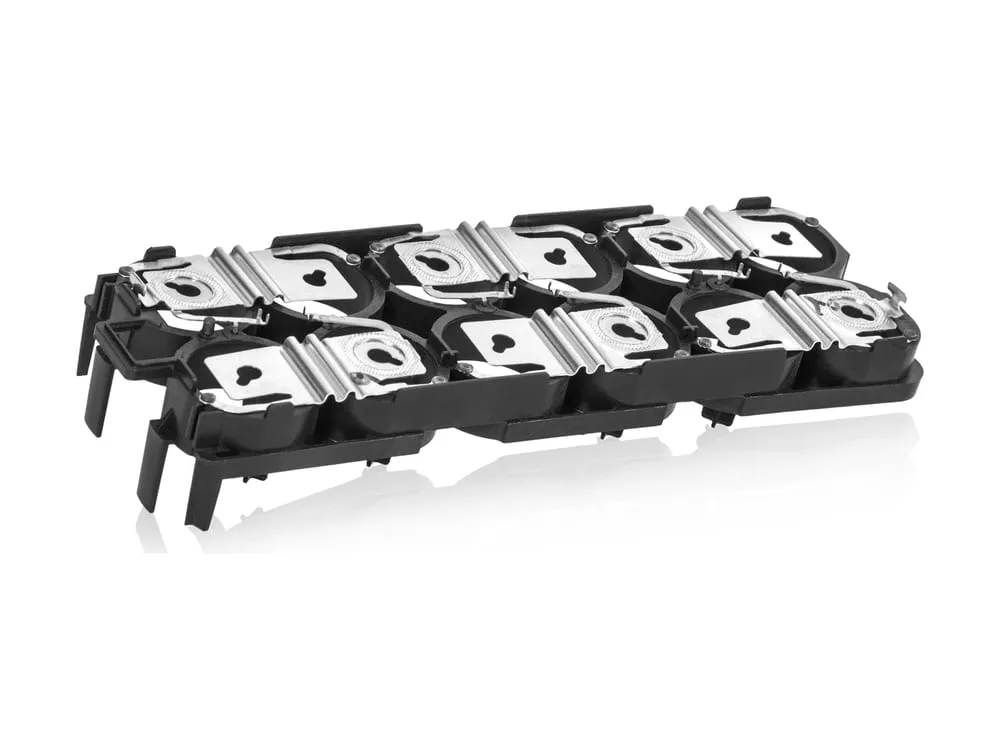
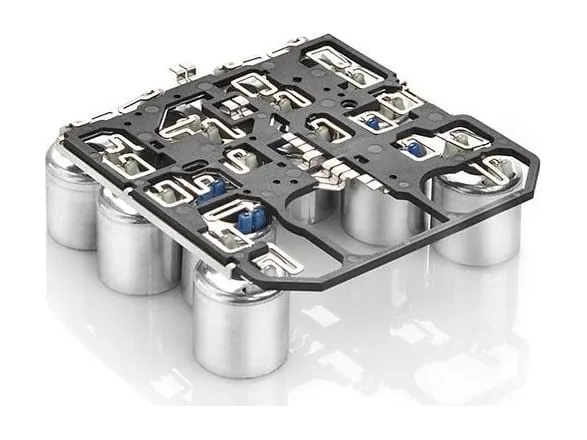
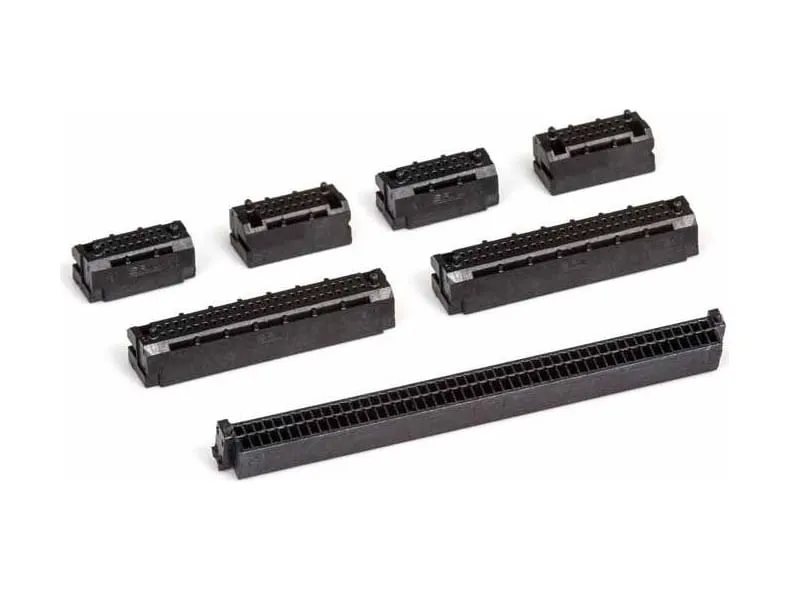
The cell-contacting system that links the cells of a traction battery: low losses, tolerance compensation between cells, fast assembly. Connectors come out produced and mounted in the carrier frame.
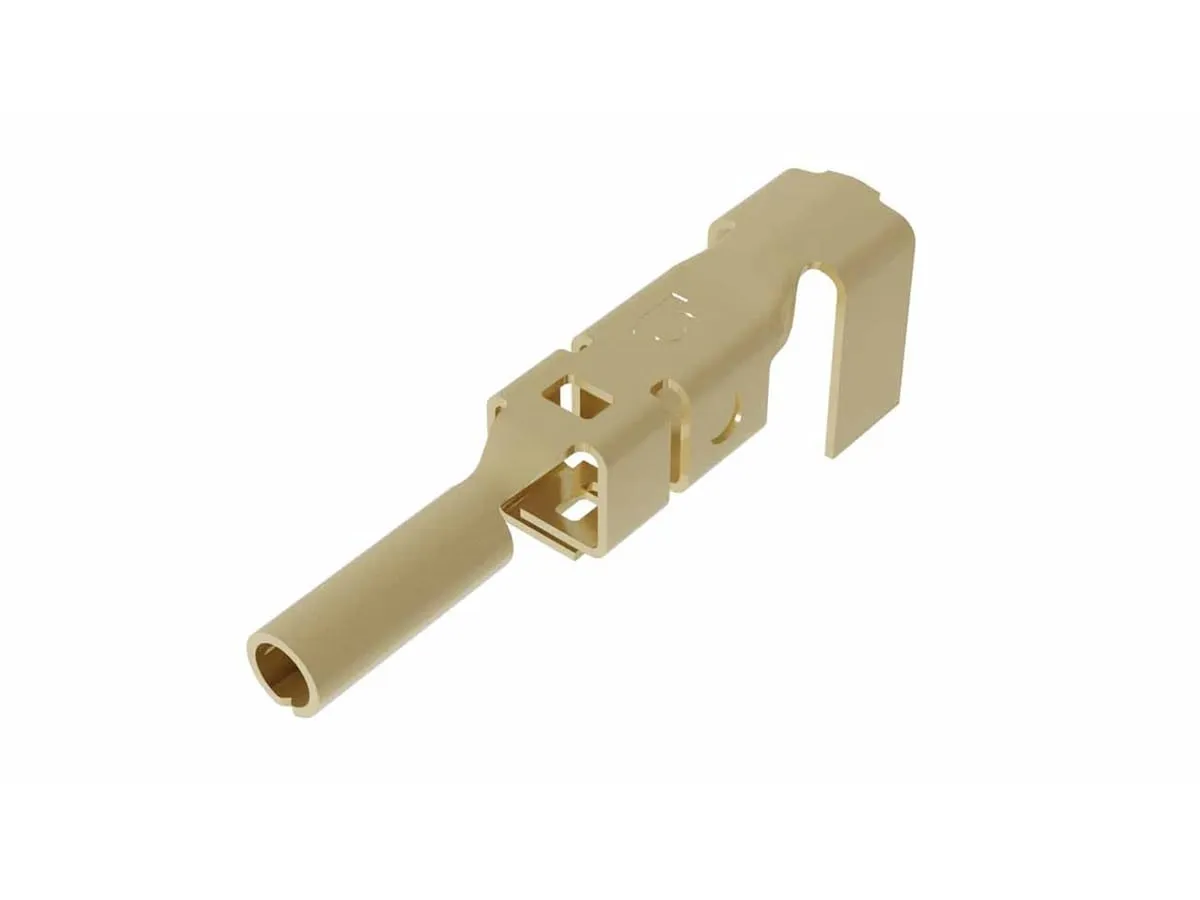
Stamped connector pins and contacts: precision cutting, embossing, piercing, calibrating and collar drawing; forming, laser-welding and assembly modules combine in one line.
ESP valves need precise control. The coil assembly is built in one system from component feeding to finished parts on pallets, at 1.5 s per part; retooling takes minutes.
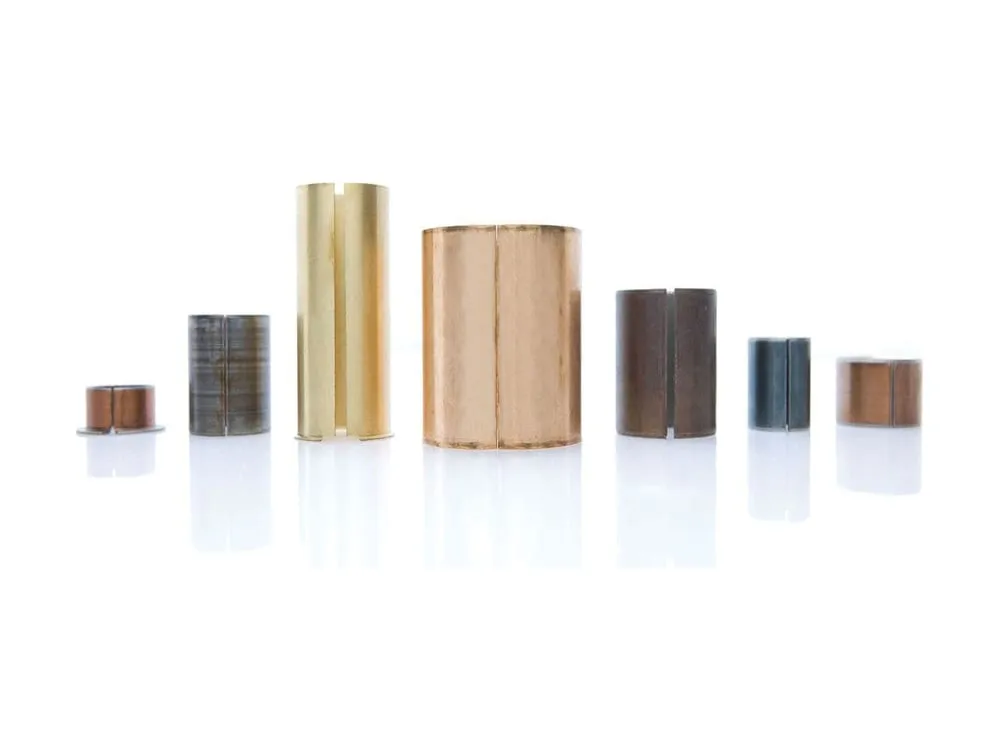
Cylindrical plain bearing bushes, with or without flange, cut, bent and calibrated from composite sintered strip. A bushing machine makes 220 straight or 160 flanged bushes per minute.
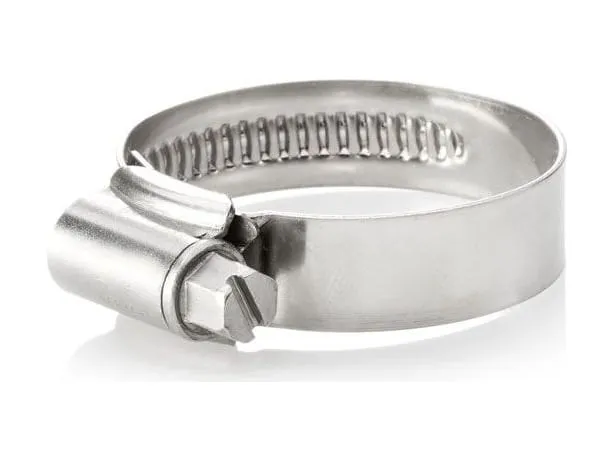
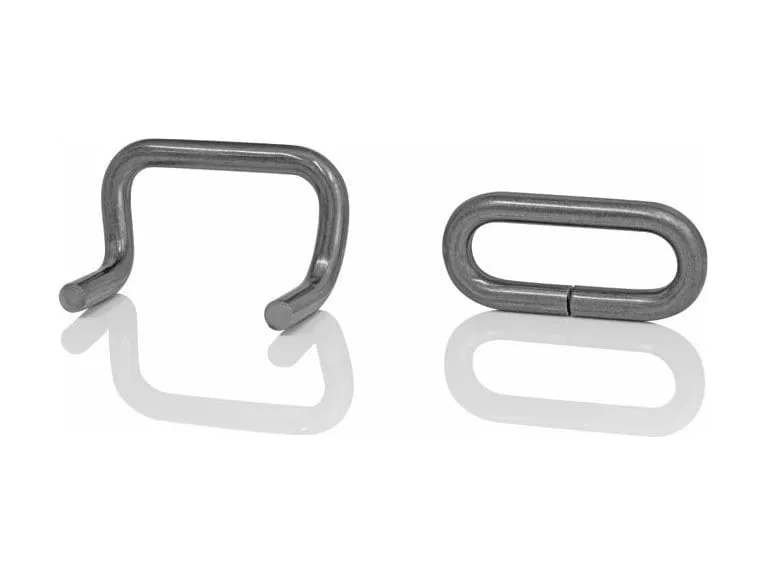
Worm-gear hose clamps whose screw engages perforations or embossed grooves in the band. One system delivers 100 fully assembled clamps per minute, Ø 8–120 mm; setup under 30 minutes.
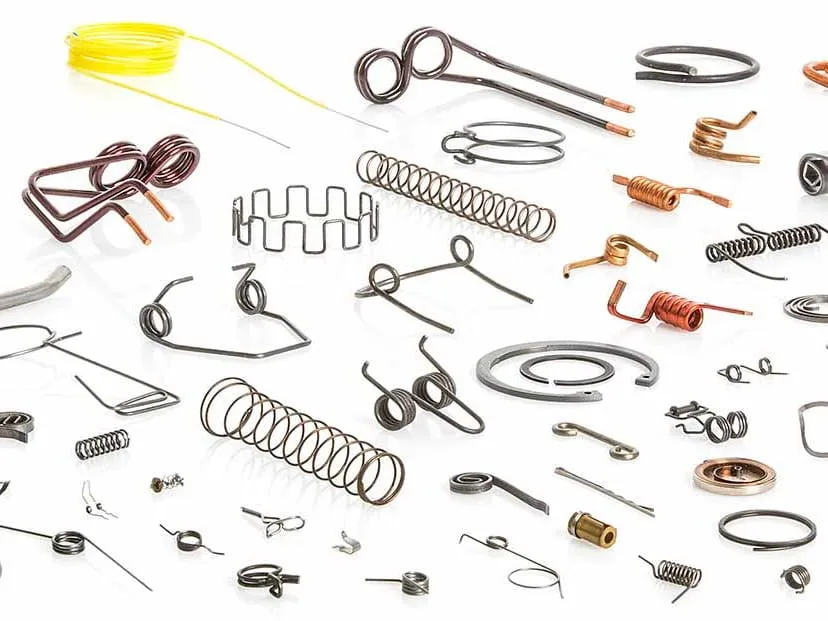
Bihler's speciality since its first spring-winding machine in 1953. Simultaneous forming gives very high speeds and forming from the inside out avoids twist; wire parts can also be coined, cut and welded.
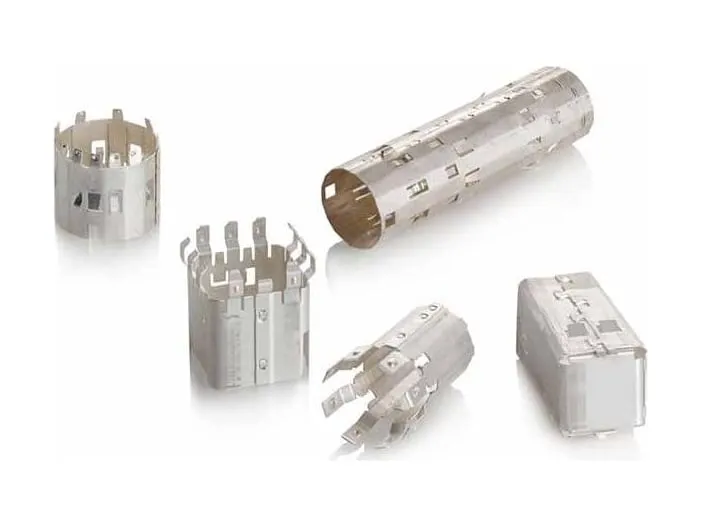
Sleeves that shield charging-socket components of electric vehicles against electric and magnetic fields. Up to 170 per minute, variant change under 30 minutes.
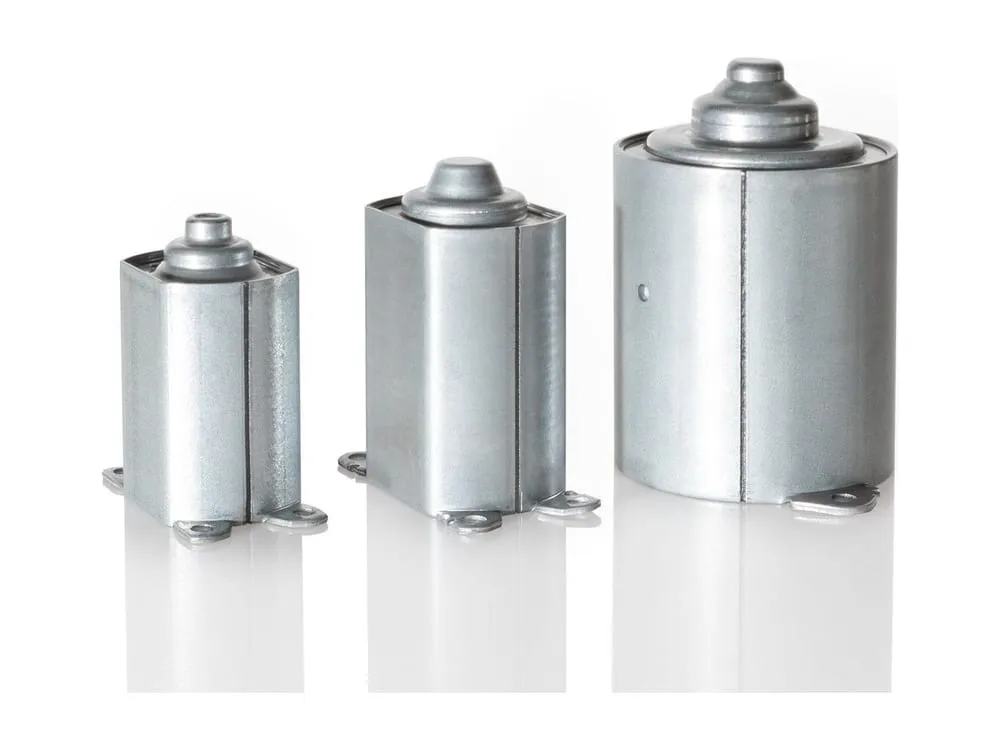
Made from strip instead of deep drawing: stamping, forming, laser welding and assembly in one system; less material and weight, no drawing oil. Double-walled housings raise motor performance.
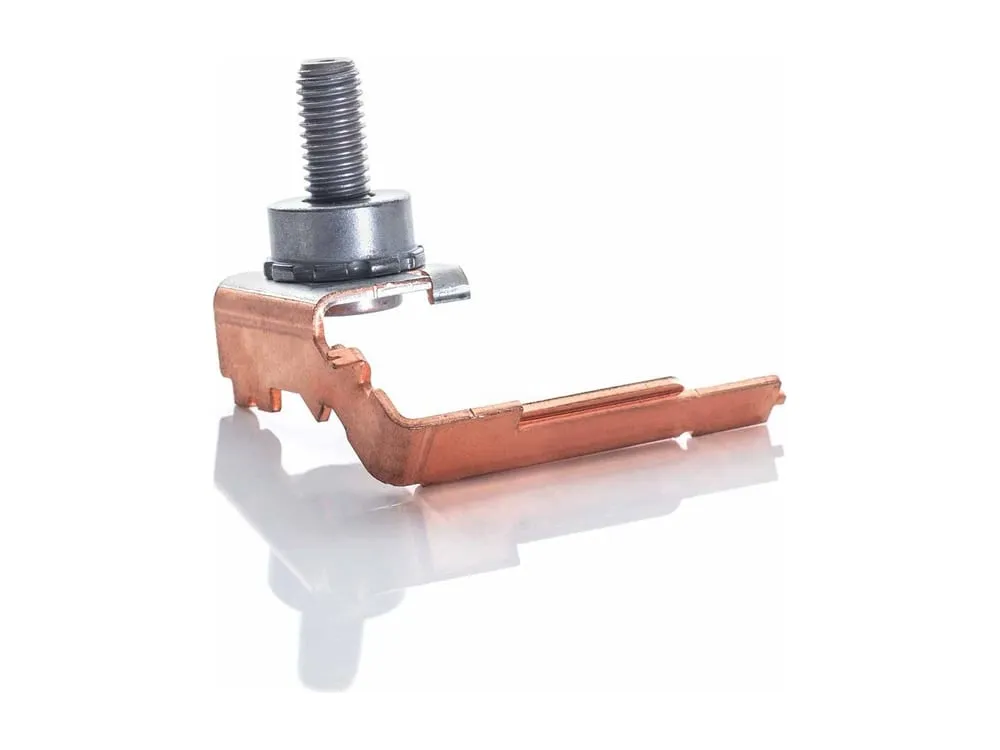
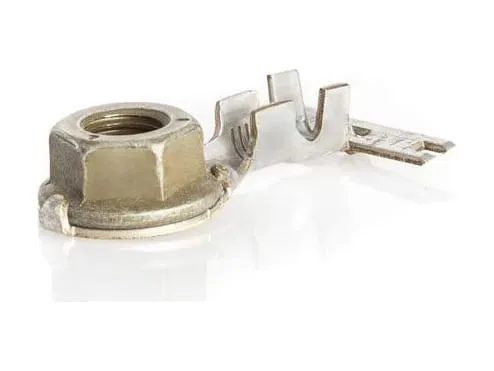
Connects the EV battery to the chassis for potential equalisation, spark and EMI protection. Stamping, bending, bolt and washer feeding and force-monitoredpress-fitting in one system; three variants, 60 per minute.
Safety-critical: must be produced in high volumes with short cycle times and process reliability. With Euro 7, hard-coatedlow-emission discs join grey-cast-iron discs in series production.
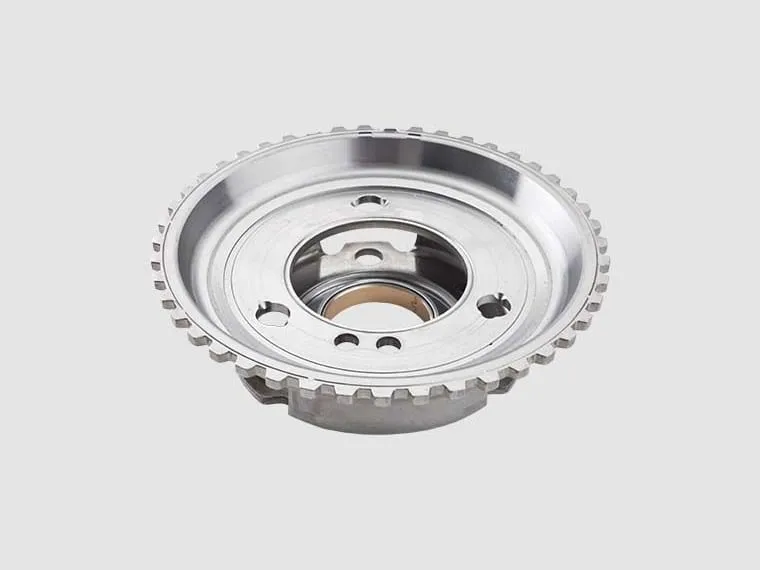
As transmission output grows, gears, disc carriers, shafts and planet gears must be made in larger volumes, with high precision and flexible processes.
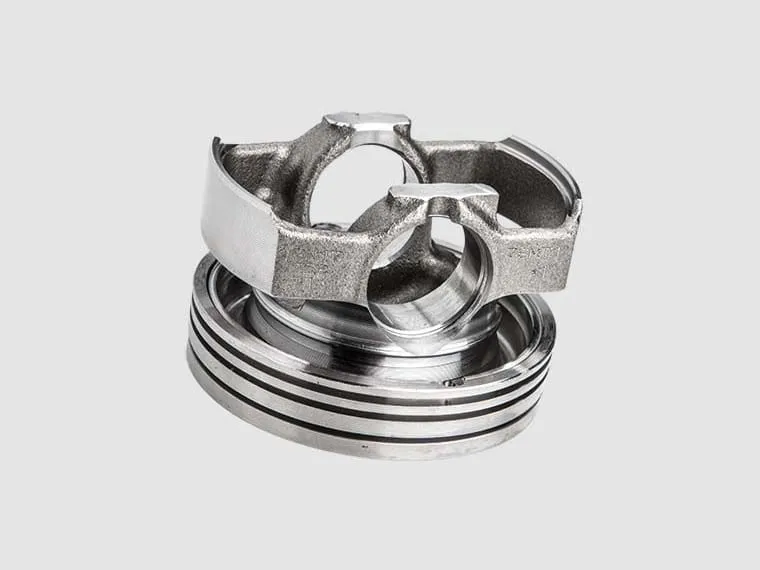
Critical for clean combustion and long engine life, with ever more complex shapes. Very tight outer-contour tolerances; aluminium and hardened-steel pistons of different types and sizes on one machine.
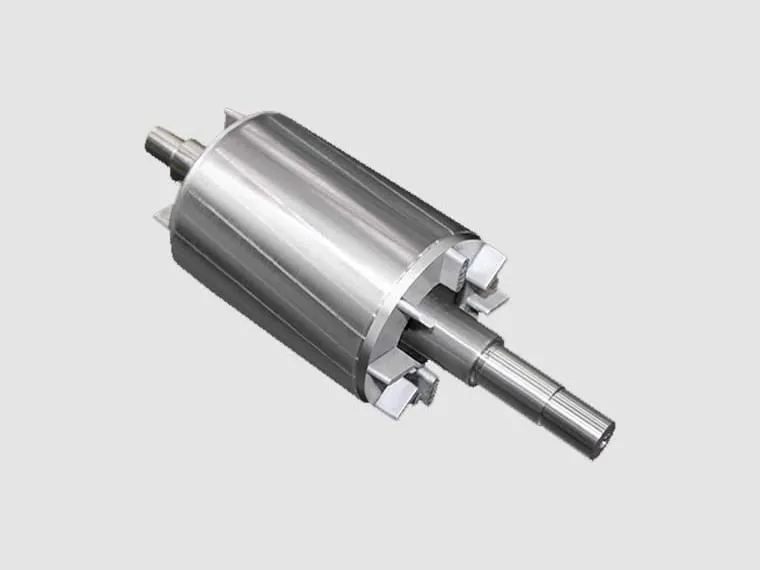
Solid small-diameter shafts in electric motors; the lamination stack makes the rotor heavy, and every extra gram reduces an EV's range. Machined in complete cells with robot or gantry loading.
An indispensable, complex-shaped connecting element of the drive train. Needs high volumes, error-free processes and short cycle times; turning is split into several sub-processes.
Modern automatic transmissions contain up to three planetary gear sets; the planet carrier holds their gears. Increasingly common thanks to high efficiency, compact design and high power density.
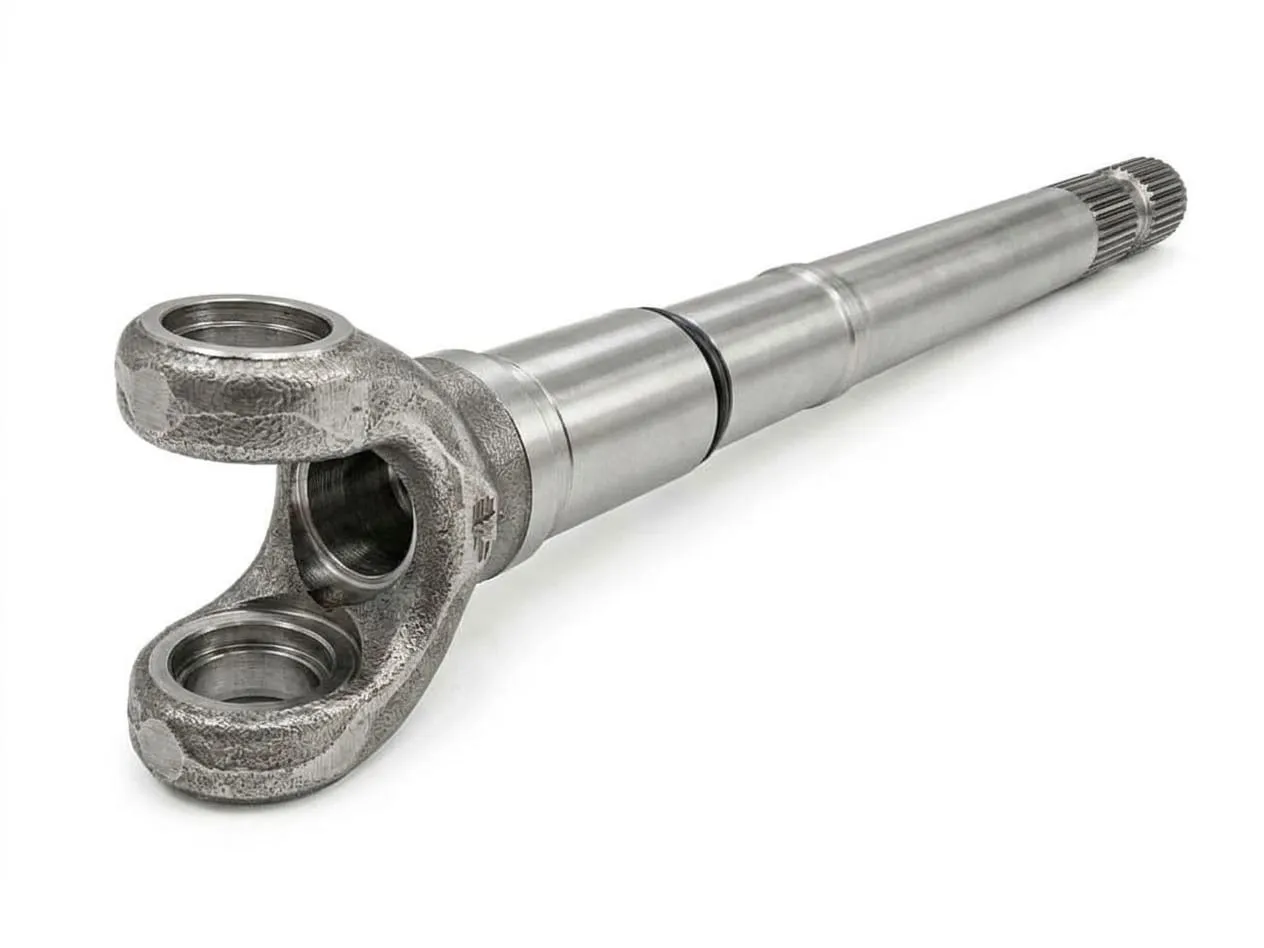
A drive component in commercial vehicles, agricultural and construction machinery. Yoke eye and cross holes are machined in few setups; bearing seats are pre-turned before hardening and ground afterwards.
References: TOFAŞ, Ford Otosan, Renault, Mercedes-Benz, MAN, BMC, ZF, Bosch, Delphi, Federal Mogul, Valfsan and Doğu Pres are among our references in this industry. All references
Your workpiece is not listed?
Describe the workpiece, material and annual quantity; we will define the right machine type together.