Complete installation
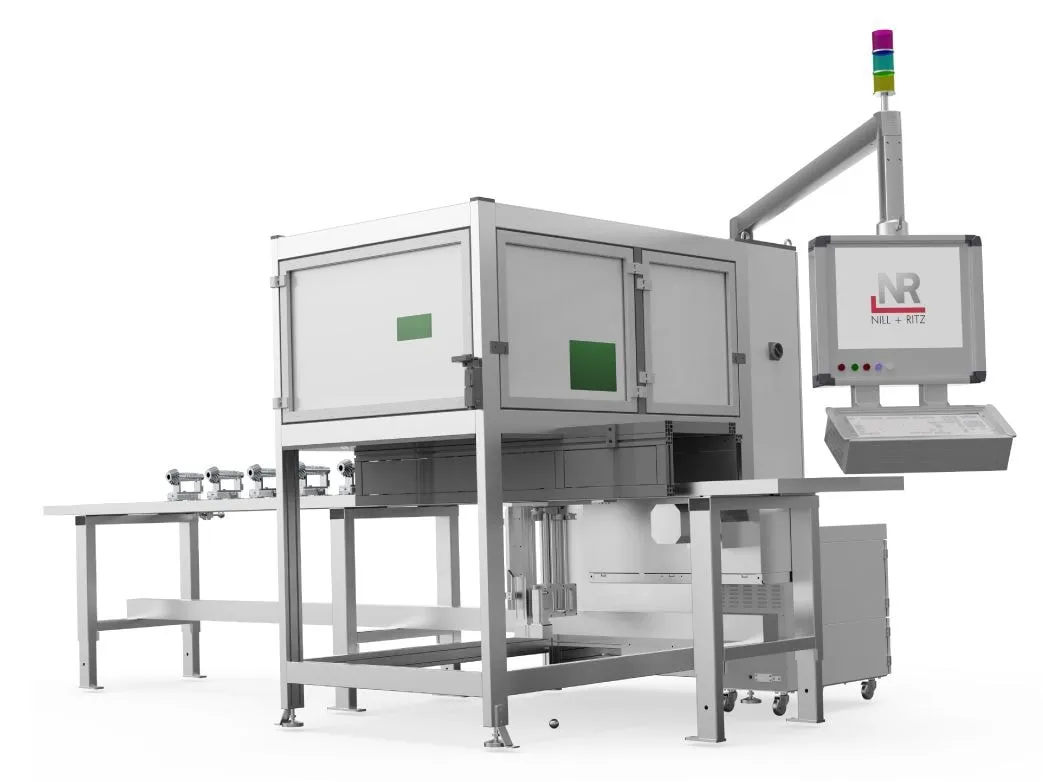
Nill + Ritz combines part infeed and outfeed, conveyors, handling and clamping systems and, on request, robot cells with the marking unit in one station; from semi-automatic to inline production.
Since 198343 years serving Turkish industry
Inline marking stations
Fully automatic laser and dot peen marking with part feeding, position detection and Data Matrix reading
ⓘ Manufacturer reference applications; every station is engineered for the part. Values may change and vary; not binding on Boztaş.
Nill + Ritz combines part infeed and outfeed, conveyors, handling and clamping systems and, on request, robot cells with the marking unit in one station; from semi-automatic to inline production.
Plain text and Data Matrix code; a camera detects part position and hole pattern, after marking a second camera reads the code and grades its quality against a standard.
Laser, dot peen, scribe, machined engraving and inkjet are combined to suit the part; in the brake disc station, for example, laser marking takes 12 s and dot peening 38 s.
Laser class 1 housing, laser safety window and working-area lighting; additional controlled axes, rotary table and handling
Suited to: Crankshaft, crankcase, gearbox and pinion shaft, dual-clutch transmission, drive set, film
Modular TSM unit; complete installation with feeding system, conveyor, handling and clamping system
Suited to: Crown wheel, piston, aluminium cast housing, motorcycle frame
Laser + dot peen marking or dot peen marking + inkjet; robot or portal loader
Suited to: Brake discs
Plate handling with different plate magazines, fully automatic infeed and outfeed, special software and order management, extraction
Suited to: Type plates in different sizes
| Feature | Brake disc (dot peen + engraving) | Brake disc (laser + dot peen) | Crankshaft (laser) | Pinion shaft (laser) | Drive set (laser) | Piston (TSM dot peen) |
|---|---|---|---|---|---|---|
| Part | ||||||
| Part size | 230–450 mm | 200–450 mm | — | 150–320 mm | — | 90–150 mm |
| Material | Aluminium / cast steel | Aluminium | Steel | Aluminium / cast steel | Steel | Aluminium / cast steel |
| Marking | ||||||
| Method | Dot peen marking and machined engraving | Laser and dot peen marking | Laser | Laser | Laser | Dot peen marking |
| Content | Plain text and Data Matrix | Plain text and Data Matrix | Plain text and Data Matrix | Plain text | Plain text and Data Matrix | Plain text |
| Times | ||||||
| Marking time | 30 s | Laser 12 s, dot peen 38 s | 8 s | 12 s | Plain text 3.5 s; with Data Matrix 6.5 s | 11 s |
| Cycle time | 60 s | 60 s | 20 s | 32 s | 13.5 s | 15 s |
| Axes and feeding | ||||||
| Axis configuration | 3 linear, 1 rotary, 1 swivel axis | 5 linear, 1 rotary axis | 2 linear axes, 1 rotary table | 1 rotary, 1 linear axis | 2 linear axes, 1 lifting axis with gripper jaws | 3 linear axes |
| Part feeding | Roller conveyor and portal gripper | Robot | Loading portal | Pallet conveyor system | Lifting unit | Robot loading |
| Equipment | ||||||
| Accessories | Part position detection, tool changer, hole-pattern recognition, extraction | Part position detection, hole-pattern recognition, Data Matrix reading, pneumatic drawer and clamping, extraction | Data Matrix camera, extraction, laser deflection, live-image camera, database connection (ORACLE) | Extraction | Data Matrix camera, extraction, pneumatic swivel unit | Pneumatic clamping fixture, electrical probing |
| Interfaces | — | — | — | — | ProfiNet, switch, TCP/IP, BDE (production data acquisition) | — |
Manufacturer reference applications; every station is engineered for the part. Further references (marking / cycle time): dual-clutch transmission, laser, 50 / 72 s; crankcase, laser, 15 / 30 s; gearbox shaft, laser, 18 / 32 s; brake disc, TSM dot peen + inkjet, 26 / 34 s; aluminium cast housing, TSM dot peen, 22 / 42 s; motorcycle frame, TSM scribe, 22 / 40 s.
Technical data is taken from information published by the manufacturer. The manufacturer may change it without notice, and values may vary with the model and the machine configuration. The data is for information only and is not binding on Boztaş; binding values are stated only in a written quotation.
Related industries: AutomotiveAerospace
In the manufacturer's reference stations cycle times vary with the part: 13.5 s for a drive set (laser), 60 s for a brake disc, 72 s for a dual-clutch transmission. The time depends on part, content and method.
Nill + Ritz offers both methods and compares them for the application. In one gear application laser was chosen for its shorter marking time, text adaptation without tool change and no worn marking tools to replace. On crown wheels and bevel gears, assembly data is applied inline by dot peen marking.
Yes; reference stations have been built with ProfiNet, TCP/IP and BDE interfaces, an OPC interface, barcode scanner and database connection. The marked Data Matrix code is read by camera in the station.
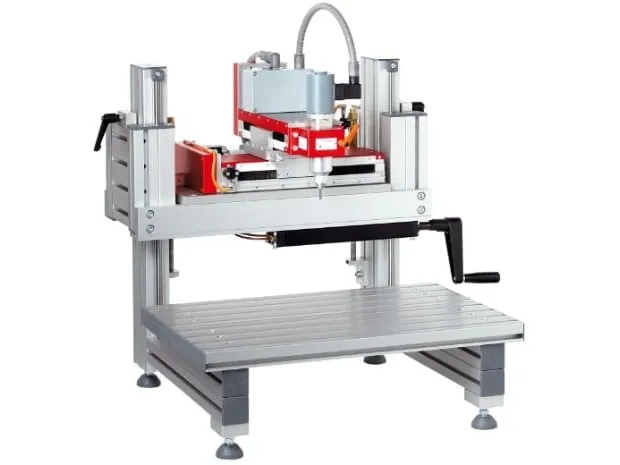 Nill + Ritz TSM Dot peen and scribe marking: integration module, bench machine with underframe and type-plate machine 50–800 mm50–400 mm120 mm/s Technical data
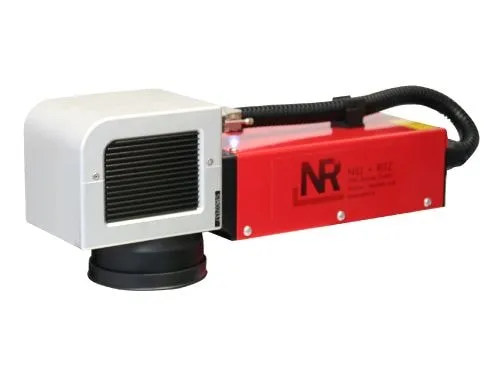 Nill + Ritz ISN marking laser 20, 50 and 100 W fibre laser marking modules for integration into production lines 20–100 W1,064 nm2–200 kHz Technical data
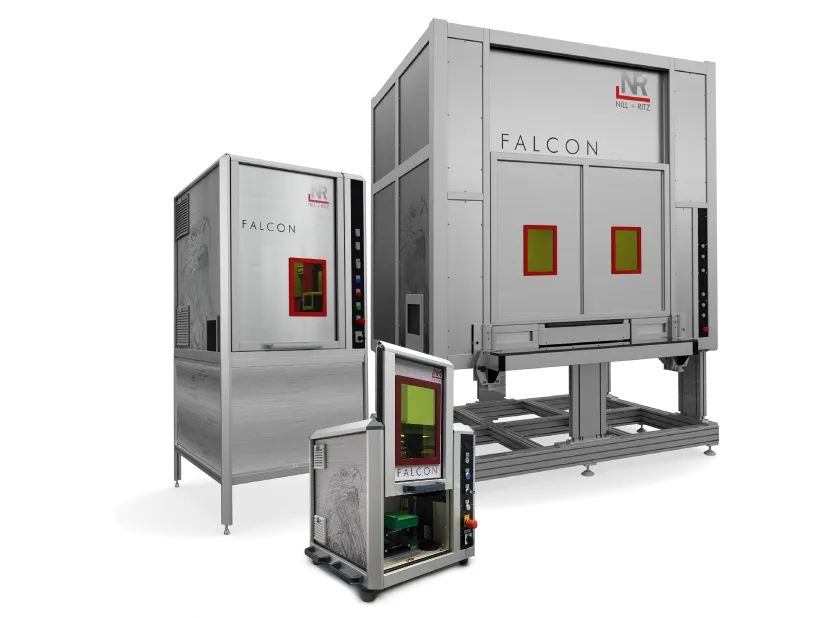 Nill + Ritz FALCON Laser marking stations in five sizes and a laser cabin for large parts 5 sizes1,300 × 1,100 × 800 mm~1,000 × 1,000 mm Technical data